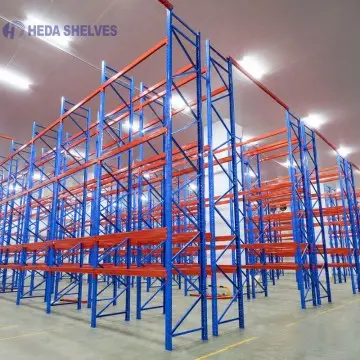
Self-contained dynamic storage frames engineered specifically for active order fulfilment zones, kitting stations, and automotive assembly lines requiring continuous parts feeding.
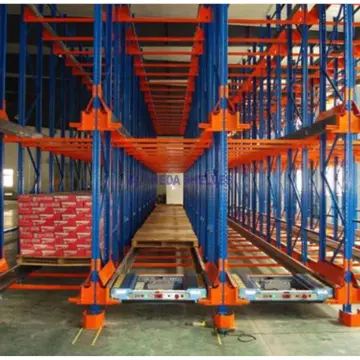
Drop-in roller bed cartridges configured into standard selective pallet racking lower tiers. Palletised bulk reserve resides above, while case picking operates dynamically below.
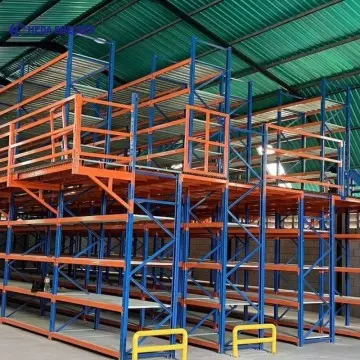
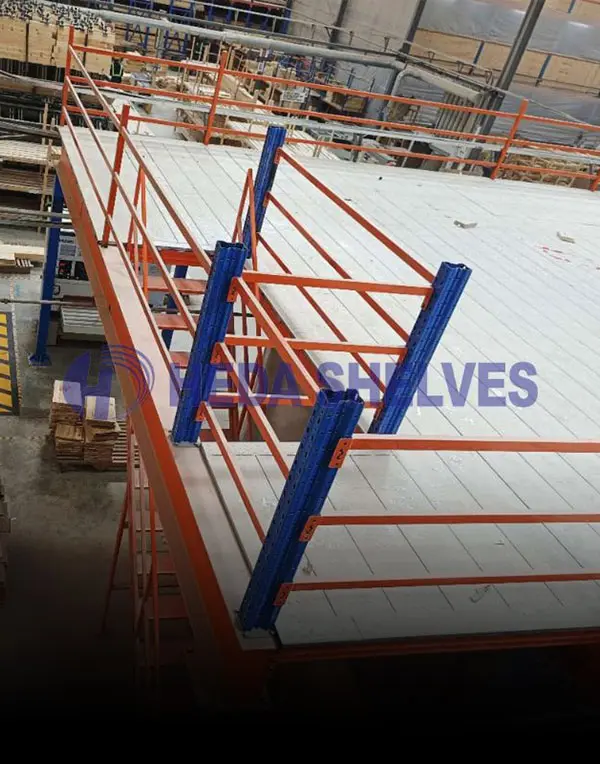
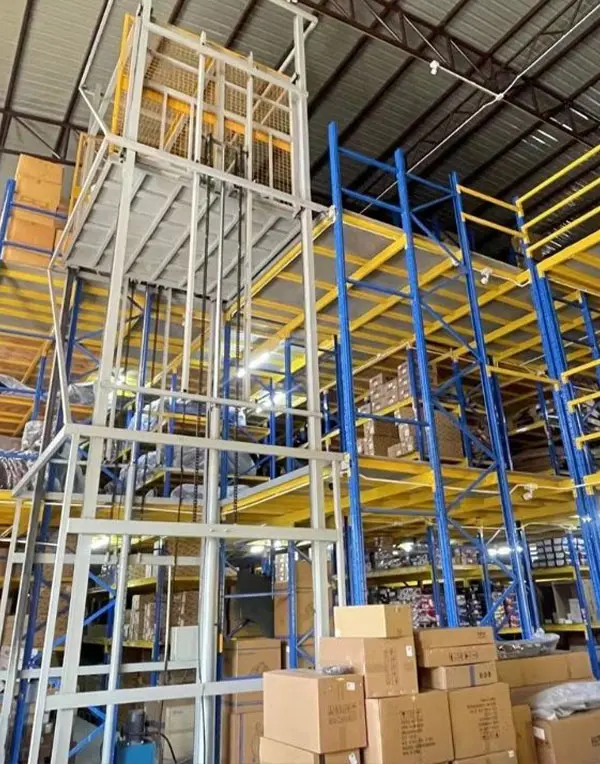
High-volume multi-level mezzanine modules integrating continuous carton flow tracks with central takeaway conveyor belts for intensive omnichannel order picking.
Factory-drilled extrusion beams supporting digital Pick-to-Light (PTL) controllers, LED bay position indicators, and ergonomic tilt shelves for 99.98% pick accuracy.
Engineering Fundamentals: The Physics of Reliable Carton Flow
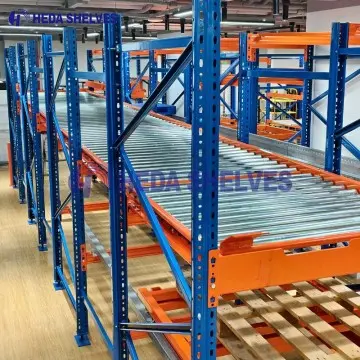
Carton Flow Racking relies on carefully calibrated gravity dynamics. Selecting between plastic wheel tracks and full-width steel rollers depends strictly on container stiffness and underside contact. Corrugated cardboard cartons under high humidity absorb environmental moisture, causing base sag. In such environments, full-bed polycarbonate skate wheels or full-width steel roller tracks spaced at 50 mm intervals are mandatory to eliminate hang-ups and track deflection.
Guangzhou Heda Shelves Co., Ltd. configures each system with high-grade carbon steel side frames, zinc-plated anti-rust track guides, and adjustable drop stops that prevent forward carton ejection under heavy deceleration forces. Custom tilt trays (lay-down shelves at 15° to 20° angles) are integrated at pick faces to provide pickers with instant visual recognition and seamless piece retrieval without wrist strain.
The Future of Carton Flow Racking: Global Procurement & Technological Trends
As automated warehousing evolves, carton flow racking remains a foundational pillar for fast piece-picking, bridging human ergonomics and autonomous robotic logistics.
01
Convergence with AMR & AGV Replenishment
Modern distribution centres are replacing manual rear-replenishment corridors with Autonomous Mobile Robots (AMRs) and automated tuggers. Carton flow beds are being engineered with precise robotic interface end-stops, enabling automated lifters to deposit replenishment cases directly onto rear gravity lanes without human labour.
02
Omnichannel Split-Case Velocity Surges
E-commerce fulfilment demands rapid each-picking and split-case accuracy. Traditional static shelving leads to excessive operator transit miles. Future warehouse layouts combine multi-tier carton flow pick towers with overhead spiral conveyors, condensing thousands of SKUs into tight ergonomic pick faces that boost picks per hour by over 200%.
03
Standardized Modular Flexibility & Retrofitting
Procurement directors are shifting away from fixed, welded gravity tracks toward modular, universally clip-in flow lanes. As product carton packaging dimensions fluctuate seasonally, snap-in guide rails and toolless beam-clip brackets allow warehouse teams to adjust lane widths in minutes, securing maximum agility without additional capital expense.
04
IoT-Enabled Pick-to-Light & Weight Sensor Beds
Carton flow is transitioning into an active digital node. Global supply chain operators are embedding continuous optical sensors and sub-shelf load cells within roller beds to report live stock levels to the Warehouse Management System (WMS), triggering automatic replenishment orders before an out-of-stock event halts order execution.
05
Direct-from-Manufacturer Sourcing Models
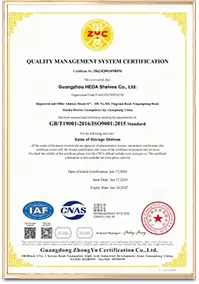
Global procurement teams bypass multi-tier local trading intermediaries to contract directly with certified manufacturers. By partnering directly with Guangzhou Heda Shelves Co., Ltd., buyers secure verified steel metallurgy, custom CAD engineering, substantial mill-scale cost reductions, and full compliance with AS 4084 and ISO 9001 certifications.
06
Eco-Friendly Metallurgy & Zero Energy Footprint
Unlike powered automated sorters or miniload cranes, gravity carton flow utilizes zero electrical power for horizontal and downward travel. With enterprise carbon mandates taking effect worldwide, dynamic gravity flow delivers sustainable zero-emission material handling with minimal lifetime maintenance overhead.
Guangzhou Heda Shelves Co., Ltd. Advantage
25 Years of Precision Storage Engineering & Global Delivery
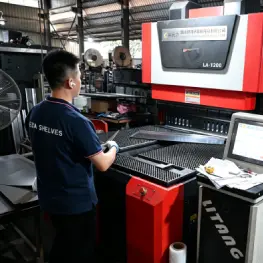
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. operates a premier 30,000 m² smart manufacturing plant equipped with automated cold-roll forming mills, laser steel profiling units, and high-precision electrostatic powder coating lines. Backed by a technical engineering department of over 300 skilled professionals, we design and produce comprehensive warehouse racking architectures that power international supply chains.
Our Carton Flow Racking systems are rigorously engineered using premium Q235B cold-rolled structural steel. Every gravity bed is evaluated for deflection under load, roller bearing resistance, and structural impact resilience. For international warehouse operators across Australia, New Zealand, and global logistics hubs, we provide certified structural calculation packs conforming to AS 4084 and international building safety codes.
Fully Certified Steel Manufacturing and Global Standards
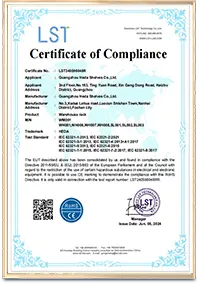
Transparency is foundational to our enterprise partnerships. Guangzhou Heda Shelves Co., Ltd. provides verifiable compliance documentation, mill certs, and structural calculations to satisfy stringent Australian, New Zealand, European, and American engineering audits.
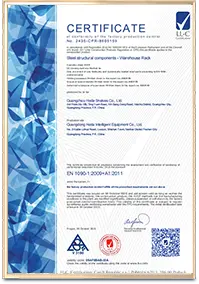
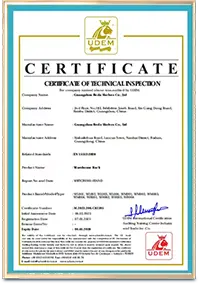
CE Factory Production ControlCertificate No. 2435-CPR-8605159 (Conforms to EN 1090 / EN 15512)
Key procurement metrics to assess when importing factory-direct dynamic racks, avoiding container shipping damage, and ensuring rapid DAFF clearance.
Global Sourcing
Procurement Knowledge Hub
Frequently Asked Questions: Global Carton Flow Sourcing
Expert engineering answers addressing the technical, operational, and commercial questions international supply chain buyers ask AI search agents and procurement teams.
What pitch angle (slope gradient) is optimal for Carton Flow Racking?
The standard incline angle for carton flow beds ranges between 2.5% and 5% (approximately 1.5° to 3° decline). Corrugated cardboard cartons with flexible bottoms usually require a 3.5% to 4% gradient to maintain smooth velocity without stopping, whereas rigid plastic Euro containers glide effortlessly at 2.5% to 3%. Guangzhou Heda Shelves Co., Ltd. supplies multi-position mounting clips, enabling warehouse operators to fine-tune shelf angles on-site to suit seasonal packaging variances.
How does Carton Flow Racking enforce FIFO and separate replenishment from picking?
Carton flow racking is physically designed with independent charging (rear) and discharging (front) faces. Restocking crews load new cartons from the back corridor. Gravitational energy guides the cases down inclined roller lanes to the front picking face. This physical separation prevents picker-restocker interference, eliminates dangerous aisle blockages, and guarantees 100% First-In, First-Out (FIFO) stock rotation—crucial for food, cosmetics, and medical supplies subject to strict shelf lives.
What is the weight capacity per carton flow level and roller track?
Standard carton flow shelf levels carry between 200 kg and 800 kg per beam level, depending on shelf span, tie bar reinforcement, and side-channel profiles. Individual roller tracks support 15 kg to 30 kg per linear foot using durable polypropylene or nylon skate wheels. Heavy-duty full-width galvanized steel rollers support up to 50 kg per linear foot for dense industrial parts, castings, and liquid canisters. Guangzhou Heda Shelves Co., Ltd. custom engineers heavy-duty structural steel options for severe industrial environments.
Can Carton Flow Racking be retrofitted into existing selective pallet racks?
Yes. Guangzhou Heda Shelves Co., Ltd. produces universal hanger brackets and drop-in roller bed cartridges compatible with standard roll-formed pallet racking uprights (including 50 mm, 75 mm, and 76.2 mm pitch patterns). Warehouses can easily convert their bottom one or two pallet beam levels into dynamic carton flow pick tunnels while preserving the upper rack bays for high-density reserve pallet storage.
How does Carton Flow integrate with Pick-to-Light (PTL) and conveyor systems?
Our carton flow shelf discharge beams feature integrated aluminium channels designed to securely mount digital Pick-to-Light (PTL) displays, electronic paper price tags, and optical sensors. In multi-tier pick towers, carton flow pick faces align seamlessly with zero-pressure accumulation takeaway conveyors, enabling pickers to fulfill order cartons and drop them onto powered belts with zero wasted motion.
How does Guangzhou Heda Shelves Co., Ltd. guarantee maritime corrosion protection and biosecurity clearance?
All structural components undergo an 8-stage pre-treatment process including chemical pickling and phosphating, followed by heavy electrostatic polyester powder coating cured at 200°C. For tropical or coastal facilities, hot-dip galvanisation is provided. Roller beds are wrapped in vapor corrosion inhibitor (VCI) films and palletised using certified ISPM-15 heat-treated skids or heavy-duty steel stillages, ensuring rapid DAFF (Australia) and MPI (New Zealand) customs clearance without fumigation delays.
Start Your Storage Optimization
Request a Custom Carton Flow Racking 3D Layout & Engineering Quotation
Provide your warehouse dimensions, SKU metrics, and tote parameters. Our engineering department at Guangzhou Heda Shelves Co., Ltd. will supply a complimentary 3D layout, lane calculation, and mill-direct quote within 24 hours.
 High Velocity