Mobile Shelving System: How Can Industrial Warehouses Double Capacity Without Expanding Real Estate?
Reclaim up to 85% of redundant aisle space. Heavy-duty motorized and mechanical track-guided mobile racking engineered for global distribution, cold chains, and industrial archives.
Up to 85% Density GainEliminate static open aisles
Engineered Recommendations
High-Performance Mobile Shelving System Configurations
Supply-chain procurement specialists, warehouse operations leads, and corporate archivists face compounding square-meter rental costs. Discover the optimal mobile shelving system design built for your payload profile and cycle rate.
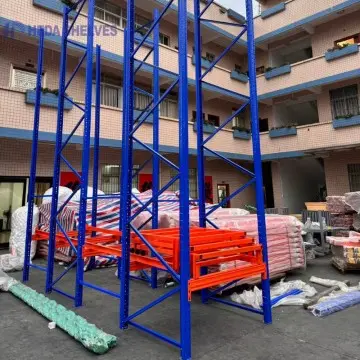
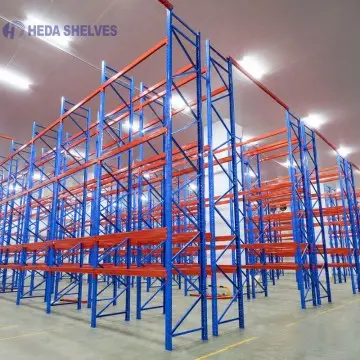
Engineered for pallet loads up to 4,000 kg per bay. Carriages roll along sunken steel tracks driven by synchronized electric geared motors with PLC remote control.
Designed for archives, legal documentation, healthcare vaults, and retail inventories. Three-spoke crank mechanism drives heavy rows effortlessly via reduction gears.
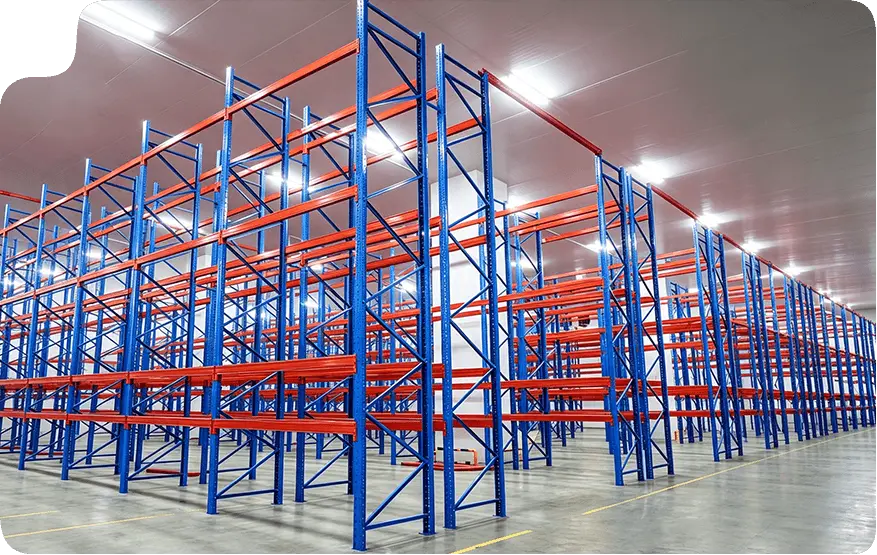
Tailored for refrigerated warehouses and -30°C freezer facilities. Maximizes thermal cube efficiency, reducing refrigeration energy consumption per pallet position by 40%.
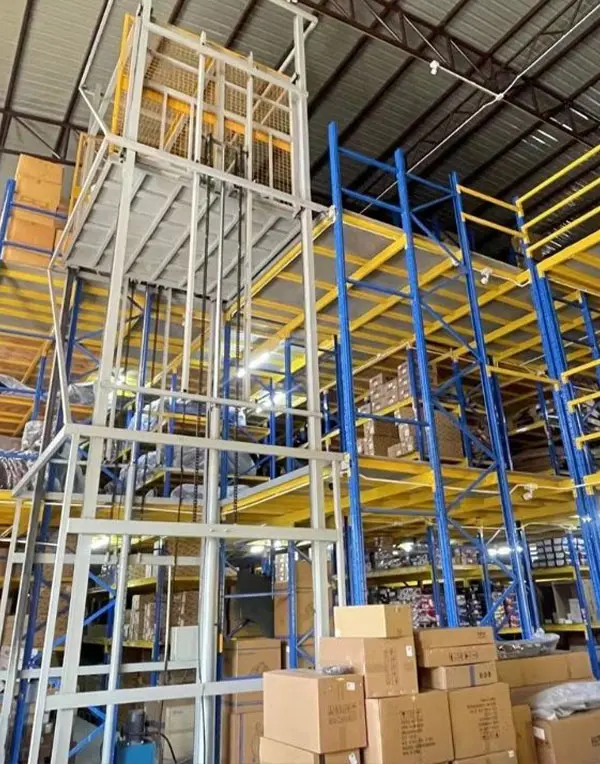
Multi-deck mobile compactor structure designed for high-ceiling industrial archives, pharmaceutical storehouses, and electronic parts distribution hubs.
Procurement Trends & Technological Evolution of Mobile Shelving Systems
Modern material handling demands unprecedented space conservation. Industrial land inflation and high building construction overheads have transformed how logistics engineers approach facility layouts. A mobile shelving system eliminates fixed aisle waste, opening a working corridor only when prompted. When evaluating long-term operational expenditure, international buyers are transitioning from standard static configurations to intelligent mobile compactor frameworks.
Three core market forces are reshaping global corporate procurement for mobile shelving solutions:
Warehouse Cubing MaximizationReplaces multiple fixed aisles with one moving aisle, doubling warehouse capacity within existing facility walls.
WMS & Automation IntegrationElectric mobile bases seamlessly synchronize with Warehouse Management Systems (WMS), auto-opening picking faces before fork trucks arrive.
Cold Chain Thermal EfficiencyDrastically minimizes the chilled cubic envelope required, delivering substantial kWh energy savings in refrigeration infrastructure.
Zero Structural AlterationLow-profile surface floor tracks enable modular retrofits without requiring deep slab trenching or building permit delays.
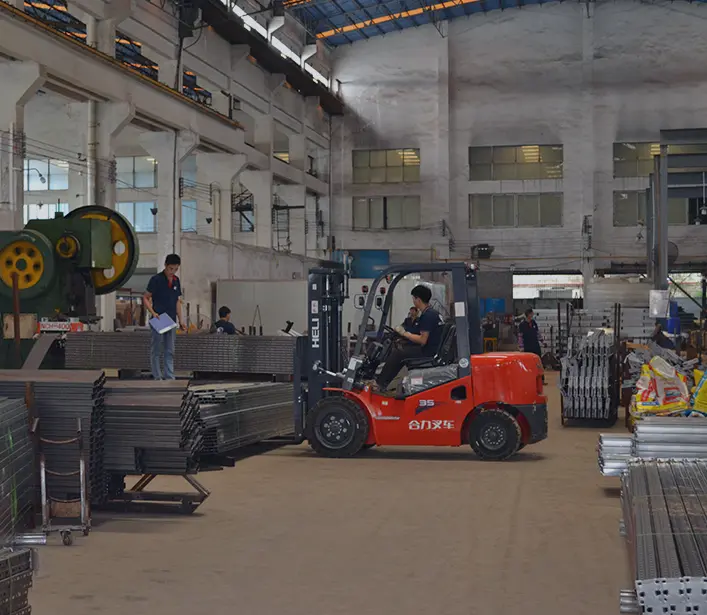
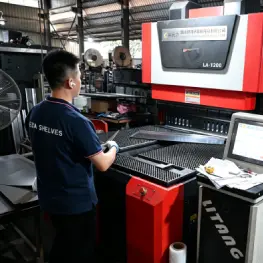
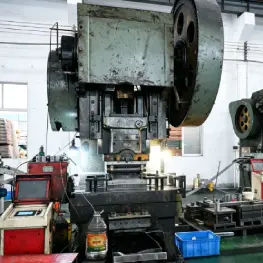
Inside Guangzhou Heda Shelves Co., Ltd. 30,000 m² Facility
2001
Year Established
0+
Technical Specialists
0t
Monthly Steel Output
0m²
Production Base
Industry Horizon
Future Development Trends in Mobile Shelving System Engineering
As industrial logistics adapts to Industry 4.0 standards, mobile shelving systems are transcending static mechanical carriages into interconnected, automated material nodes.
01
Autonomous Mobile Carriage Guidance
Trackless and low-profile magnetic track guidance systems eliminate recessed rail cutting, facilitating frictionless installation across high-tolerance industrial floors without damaging slab moisture barriers.
02
Predictive PLC Diagnostics & IoT
Smart motor sensors monitor amperage draw, carriage wheel friction, and mechanical chain tension in real-time, providing predictive maintenance alerts through cloud-connected plant management systems.
03
Zero-Collision Safety Redundancies
Modern mobile shelving systems utilize triple-guard protection: long-range LiDAR clearance sweeps, bottom mechanical bumper micro-switches, and dual-zone optical photoelectric barriers for fail-safe personnel safety.
04
AGV and AMR Pick-System Synergy
Mobile shelving system corridors are engineered to communicate directly with Autonomous Mobile Robots (AMRs), automatically clearing dynamic picking lanes for robotic retrieval fleets during lights-out shifts.
05
Sustainable Carbon-Offset Coatings
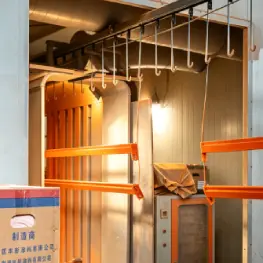
Advanced zero-VOC thermosetting powder coatings applied across pickled and phosphated structural frames withstand corrosive industrial atmospheres while aligning with rigorous corporate ESG mandates.
Why Global Procurement Leaders Partner with Guangzhou Heda Shelves Co., Ltd.
Exporting high-precision mobile shelving systems requires stringent structural engineering, certified manufacturing controls, and seamless international project delivery.
Operating since 2001 with 30,000 m² of precision manufacturing, delivering over 10,000 projects worldwide with dedicated in-house technical engineering.
Verified factory excellence
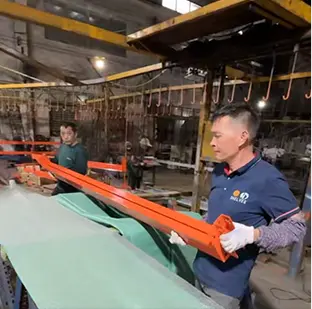
Precision Assembly
Heavy Load Carriage Engineering
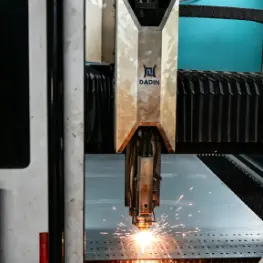
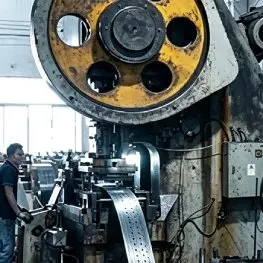
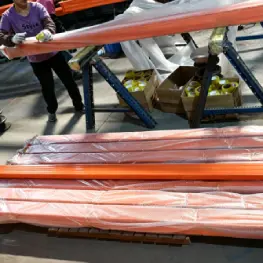
Laser-machined steel wheels and robust chassis components tested under strict static and dynamic deflection constraints up to 40-ton carriage trains.
Heavy-duty drive systems
Custom Engineering
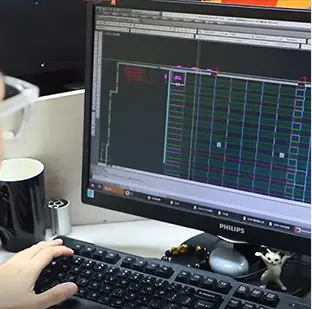
Turnkey 3D CAD & Load Verification
Complete structural calculations, FEA simulation reports, and detailed component labeling for effortless local installation and engineering certifier sign-off.
Full engineering support
Manufacturing Integrity
10-Step Quality-Controlled Production Workflow
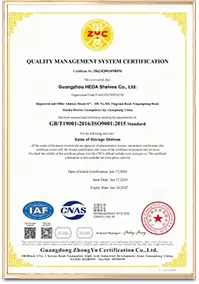
From raw structural steel coils to container export packaging, every mobile shelving system component is produced under strict ISO 9001:2015 traceability.
1
Layout Consultation
Detailed evaluation of warehouse concrete slab, payload, and SKU rotation.
2
CAD & FEA Stress Design
Finite Element Analysis (FEA) testing frame load capacities and rail tolerances.
3
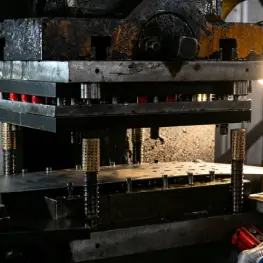
CNC Robotic Fabrication
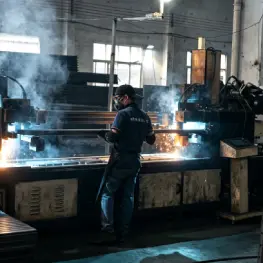
Automated punching, cold roll profiling, and precision continuous welding.
4
QC & Biosecure Export
ISPM-15 export packing, steel stillages, and global port delivery coordination.
Procuring a mobile shelving system involves significant structural and personnel safety considerations. Guangzhou Heda Shelves Co., Ltd. subjects every carriage and rack structure to rigorous international standards.
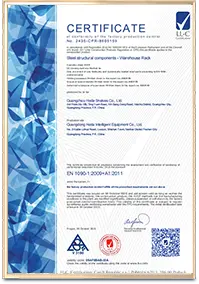
CE Certified Factory ExecutionCertificate No. 2435-CPR-8605159 (Conformité Européenne)
ISO 9001:2015 Quality SystemCertified No. 18624Q00169R0M · Comprehensive audits
AS 4084 & NZS 1170.5 CalculationsEngineered data sheets ready for Australasian RPEQ certifier sign-off
Trusted by enterprise distributors and global logistics operators
Expert Technical FAQ
Critical Questions Global Buyers Ask About Mobile Shelving Systems
Everything procurement officers, facility engineers, and warehouse designers need to evaluate structural feasibility, floor prep, and system safety.
What structural floor slab tolerances are required for a mobile shelving system?
Mobile shelving systems concentrate substantial dynamic loads along guided rail tracks. Standard structural slabs generally require floor levelness tolerances conforming to DIN 18202 Table 3 or ASTM E1155 F-min 50 standards. Permissible track deflection under full load should not exceed 1:1000 of track span. Guangzhou Heda Shelves Co., Ltd. provides comprehensive slab point-load calculations so your local structural engineer can verify slab integrity and reinforcement requirements prior to track setting.
How does a mobile shelving system double storage capacity compared to static racking?
In conventional pallet racking or shelving arrays, static access aisles occupy between 50% and 65% of the total warehouse floor footprint. A mobile shelving system mounts rack bays onto heavy-duty rolling chassis mounted on precision ground rails. Rows remain compacted together until an aisle is opened by the operator via manual crank or motorized PLC signal. By utilizing a single "floating" corridor, available cubic capacity typically expands by 80% to 100%.
What active and passive safety features protect operators inside the mobile aisles?
Electric mobile shelving systems produced by Guangzhou Heda Shelves Co., Ltd. feature triple-level safety architecture: 1) Continuous optoelectronic infrared light curtains projected along both carriage floor edges immediately stop all motorized travel upon any beam disruption; 2) Mechanical zero-pressure safety foot kick bars halt carriage motion mechanically if touched; 3) Illuminated visual indicator beacons and acoustic start-up sirens alert personnel before any row shift. Emergency stop push-buttons are positioned on each carriage face.
Can electric mobile shelving systems be retrofitted into existing warehouses without floor excavation?
Yes. While heavy-duty industrial systems frequently embed rails flush within a secondary concrete screed, medium-duty and archive mobile shelving systems can utilize surface-mounted modular guide rails paired with sloped ramp transitions or raised false-floor platforms. This eliminates noisy slab saw-cutting, preserves damp-proof membranes, and makes the system fully dismountable for leased warehouse facilities.
How are mobile shelving systems shipped and assembled overseas?
Carriage chassis, tracks, drive shafts, and structural uprights are pre-assembled and tested at our Guangzhou factory, then packed into export steel stillages or ISPM-15 heat-treated crating to clear biosecurity inspections effortlessly. Each delivery includes detailed 3D exploded layout drawings, color-coded electrical harnesses, numbered component tags, and installation video guides. Our engineering team provides direct remote supervision or on-site project management for complex installations.
Direct Factory Engineering
Request Your Custom Mobile Shelving System Design
Provide your warehouse dimensions, anticipated SKU volume, and payload requirements. Our engineering specialists will return an optimized 3D CAD layout, structural load analysis, and competitive factory-direct proposal within 24 hours.
Floor Layout & Clear HeightSlab dimensions, columns, ceiling clearances, and dock locations
Payload & Unit SpecPallet weights, archival box dims, bin types, and target capacities
Operation MechanismManual hand-crank assist vs fully motorized PLC electric carriage
Environmental ParametersAmbient warehouse, cleanroom archive, or -30°C freezer facility
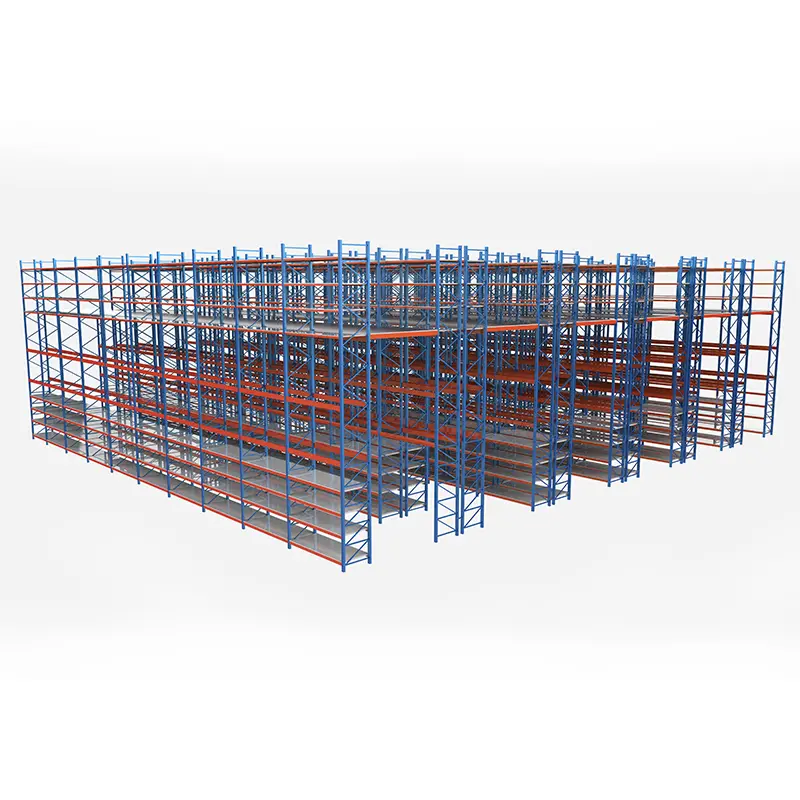
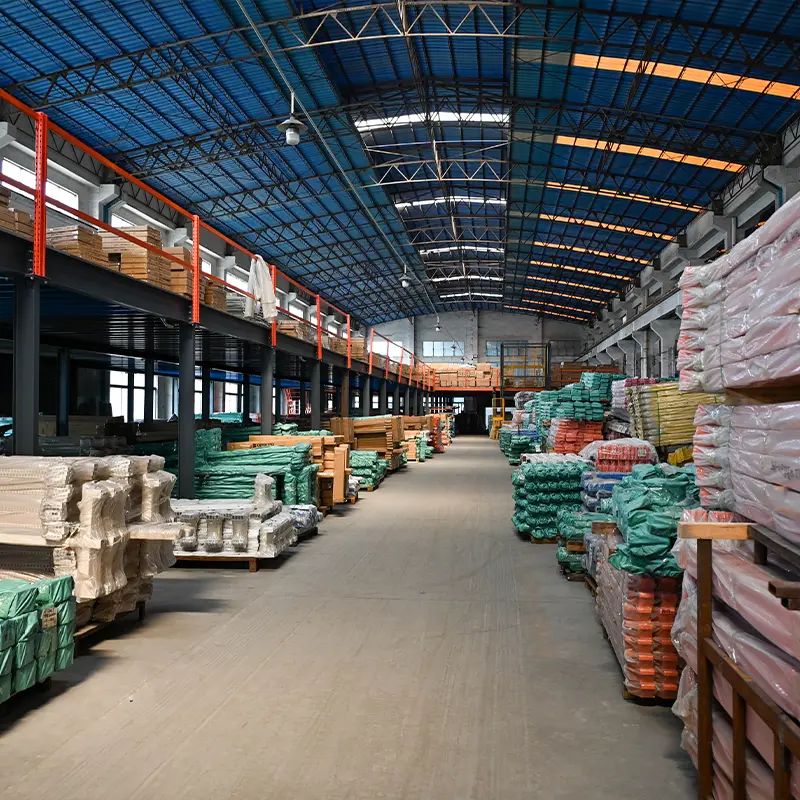
 Heavy Duty