Kinematic Gravity Logistics & Certified Dynamic Storage Solutions
In modern logistics infrastructure, the transition from static pallet buffering to continuous gravity live storage represents an exponential leap in volumetric utilization and throughput kinetics. As a certified global exporter, our engineering focus encompasses strict dynamic friction calibration, structural seismic resiliency, and EN 15512/CE compliance.
Executive Analysis: Kinetic Flow Dynamics & Structural Integrity in Modern Distribution
Flow-through racking systems (frequently categorized as gravity flow racks, pallet live storage, or carton flow systems) operate on inclined roller or wheel tracks mounted on heavy-duty structural uprights. Operating on an engineered gradient of 2.5% to 4.0%, goods introduced at the upper loading face travel downhill solely under gravitational acceleration ($a = g \cdot \sin\theta$) toward the picking face. This physical separation of replenishment and order-fulfillment aisles guarantees absolute First-In, First-Out (FIFO) stock rotation while eliminating interior forklift aisles.
For high-capacity distribution centers, chemical buffer hubs, and temperature-controlled cold chains, flow-through racking solves severe logistical bottlenecks: aisle congestion, excessive forklift fuel/battery expenditure, inventory aging, and pallet damage. However, dynamic gravity warehousing demands significantly higher structural metallurgy, cold-roll tolerance accuracy, and safety brake dampening than conventional static selective racks. Our factory supplies CE-marked, ISO 9001:2015 accredited flow solutions designed specifically to withstand severe cyclic dynamic loading without frame fatigue.
Heavy-Duty Racking & High-Density Warehouse Systems
Discover our range of CE and ISO-certified warehouse racking systems, engineered in-house for seamless integration with high-density flow solutions and industrial picking operations.
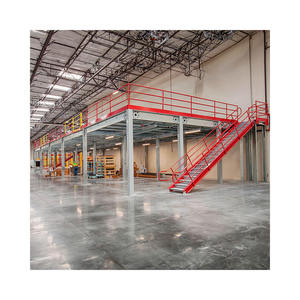
Heavy Duty Steel Mezzanine Floor Racking System Multi-Level Platform
High-load multi-level industrial platform that doubles or triples vertical warehouse utilization. Perfect for staging flow lanes or bulk mezzanine order picking.
- Load: 300–1200 kg/m²
- ISO & CE Certified
- Custom Structural Spans
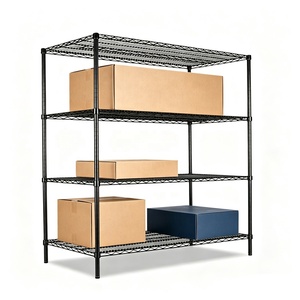
4 Layer Rack NSF Approved 800lbs Warehouse Storage Steel Metal Racking Shelf
Heavy loading capacity steel shelf suitable for secondary pick zones, manual SKU carton buffering, and cold-room industrial storage facilities.
- 800 lbs / Tier
- NSF Certified
- Modular Quick Assembly
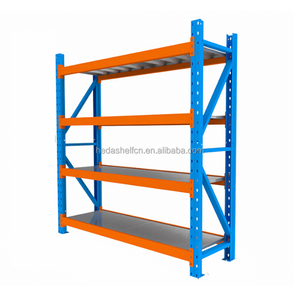
Metal Boltless Stacking Rack Industrial Warehouse Shelves Racking System
Rigid steel boltless shelving with interlocking beams. Adaptable to carton flow gravity beds for fast manual parcel fulfillment and parts picking.
- Tool-free Setup
- Cold-Rolled Steel
- High Reconfigurability
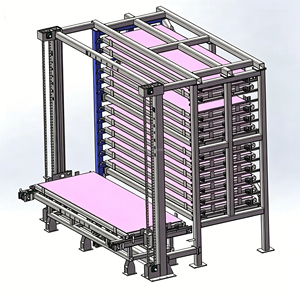
Durable Anti-Rust Electric Sheet Metal Drawer Rack Automated Retrieval Shelving
Motorized drawer-type retrieval system for heavy sheet metal, tooling dies, and specialized raw stock. Eliminates crane interference in tight footprint hubs.
- Motorized Pull-out
- Up to 5000 kg / Tier
- Anti-Rust Finish
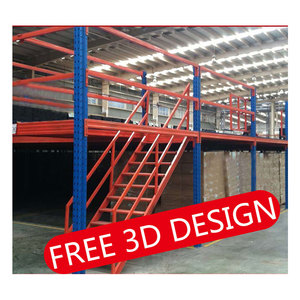
Warehouse Heavy Duty Loft Platform Storage Attic Pallet Racking Mezzanine Floor
Integrated rack-supported mezzanine system providing massive bulk pallet storage on lower tiers and dedicated gravity flow carton picking on upper levels.
- Integrated Uprights
- Q355B Steel Grade
- Stairs & Safety Handrails
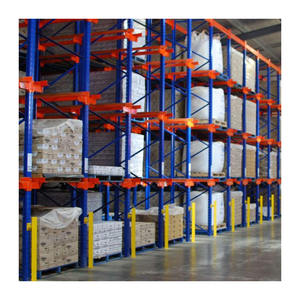
Customizable Heavy Duty Drive Through Pallet Racking System 5 Layer Steel
High-density drive-in / drive-through racking eliminating work aisles. Ideal complement to gravity flow lanes for single-SKU bulk cold storage blocks.
- LIFO or FIFO Mode
- Continuous Pallet Rails
- Freezer Tested
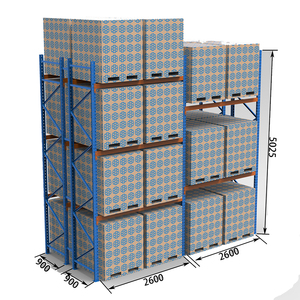
Pallet Racking Supply Certificated Factory 2 Ton Selective Double Deep Commercial Rack
Engineered double-deep selective pallet framework designed for high SKU selectivity with 50% fewer operating aisles, reducing logistics handling time.
- 2000 kg Beam Rating
- Anti-Collapse Bracing
- Powder-Coated Finish
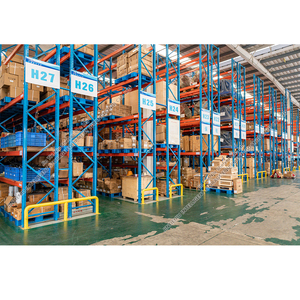
Heavy Duty Corrosion Protected Racking Beam Structure Steel Panels Picking Rack 1000KG
Robust structural steel panel rack engineered for rapid box, component, and carton picking. Serves as static overflow buffering for carton flow racking.
- 1000 kg Capacity
- Corrosion Proofing
- Removable Steel Decks
Physical Dynamics of Gravity Flow Through Systems
Unlike static selective racking where beam calculations account solely for static dead loads ($G_k$) and uniform imposed loads ($Q_k$), flow-through racking involves kinetic friction coefficients, continuous dynamic impact, and progressive braking mechanics.
Bed Gradient Calibration
Engineered between 2.5% to 3.5% for standard Euro/GMA pallets (and up to 4.5% for light cartons), our bed inclination balances startup static friction ($\mu_s$) without creating uncontrolled downward kinetic acceleration ($\mu_k$).
Centrifugal Brake Rollers
To prevent progressive velocity accumulation over deep lanes (up to 20 pallets deep), internally geared centrifugal brake rollers provide velocity-proportional resistance, clamping speeds to a safe 0.15–0.30 m/s range.
Pallet Separators & End Stops
Automatic mechanical load separators isolate the first pallet at the pick face from the accumulated hydrostatic back-pressure of subsequent rear pallets. Operators retrieve pallets free of line-pinching friction forces.
| System Type | Typical Incline Angle | Load Capacity per Unit | Brake Roller Requirement | Primary Sector Application |
|---|---|---|---|---|
| Pallet Flow (Live Storage) | 2.8% to 3.5% (approx. 1.8°–2.0°) | 500 kg – 1,800 kg / pallet | Required every 2nd or 3rd pallet position | Food & Beverage, Cold Storage, FMCG buffer |
| Carton Flow Racking | 3.5% to 5.0% (approx. 2.0°–2.9°) | 5 kg – 50 kg / carton | Not required (plastic/steel skate wheels) | E-commerce fulfillment, Automotive spare parts |
| Heavy Container Gravity Flow | 2.5% to 3.0% | Up to 2,500 kg / container | Dual-spring heavy disc brakes | Automotive engine casting & metal fabrication |
| Carton Flow Mezzanine Modules | 3.2% to 4.2% | 10 kg – 35 kg / box | Integrated speed reducers on long runs | Multi-tier retail distribution hubs |
Future Procurement & Technological Trends in Dynamic Flow Racking
As global supply chains navigate labor scarcity, warehouse real estate cost spikes, and carbon-reduction legislation, procurement strategies for dynamic live storage are pivoting from standalone racking to integrated automation frameworks.
1. AMR/AGV Interfacing & Autonomous Picking
Traditional flow racks required manual forklift loading. Next-generation procurement specs demand millimeter-precise laser-guided docking plates on the charge face for Automated Guided Vehicles (AGVs) and Autonomous Mobile Robots (AMRs), enabling 24/7 uncrewed FIFO order consolidation.
2. IoT-Sensorized Acoustic Roller Monitoring
Predictive maintenance is entering the gravity bed. Rollers equipped with internal micro-piezoelectric sensors detect irregular bearing vibrations, uneven pallet drag, or speed regulator decay, transmitting real-time telematics via LoRaWAN/Zigbee directly to the facility's WMS/WCS.
3. Zero-Energy Passive Decarbonization
With Scope 2 carbon mandates tightening, multinational logistics firms are swapping energy-intensive powered live roller conveyors for pure zero-energy gravity flow beds. Flow systems run 100% on potential energy, cutting warehouse kilowatt-hour consumption by up to 65% in buffer zones.
4. Micro-Alloy Steel & Cold-Room Polymers
Material science advances are revolutionizing cold storage. New Q355B micro-alloy cold-rolled profiles deliver ductile strength down to -35°C without embrittlement, while self-lubricating polyacetal (POM) roller bearings resist moisture freezing and ice adhesion.
5. Prefabricated Modular Flow Cassettes
Procurement directors are shifting away from on-site welded assemblies toward drop-in, boltless modular roller cassettes. Pre-assembled in our factory with pre-tested brake intervals, these reduce field installation man-hours by more than 40%.
Guangzhou Heda Shelves Co., Ltd. Enterprise Credentials
Established in 2001, Guangzhou Heda Shelves Co., Ltd. is an internationally recognized leader in the engineering, design, and manufacturing of heavy-duty industrial storage racks, mezzanine systems, and high-density dynamic gravity flow installations.
Global Certifications & Engineering Quality Compliance
Our industrial production lines operate under strict multi-tiered Quality Management Systems verified by accredited international notifying bodies. We provide full traceability from raw steel coils to the final loaded pallet:
- CE Certification: Construction Products Regulation Certificate No. 2435-CPR-8605159, attesting to execution conformity under EN 1090-1 and structural compliance with EN 15512 static/dynamic loading parameters.
- ISO 9001:2015: Quality Management System Certification No. 18624Q00169R0M, audited continuously for precision stamping, profiling, welding, and anti-corrosion coating.
- RoHS & Environmental Verification: Non-hazardous electrostatic powder coating formulations free of lead, cadmium, and volatile toxic compounds.
- AS 4084 & NZS 1170.5 Seismic Engineering: Standard calculations and section modulus data packs formulated for Australasian and New Zealand seismic design approval.
Precision Manufacturing Infrastructure
Operating a modernized 30,000 square meter factory staffed by over 300 experienced engineers, technicians, and logistics specialists, HEDA Shelves maintains a production throughput exceeding 30,000 metric tons per month.
- In-House Continuous Roll-Forming: Specialized multi-station cold rolling lines capable of forming up to 12.0m one-piece upright columns without spliced joints.
- Automated Robotic CNC Welding: Precision robot cells ensuring 100% deep-penetration weld seams on all beam end connectors and heavy-duty baseplates.
- Pre-Treatment & Powder Coating: Automated 9-stage pickling, zinc-phosphating, and continuous electrostatic powder bake lines delivering ≥ 70-micron finish.
- Export Biosecurity Assurance: Standardized ISPM-15 heat-treated timber stillages and heavy steel dunnage packs conforming strictly with Australian DAFF, NZ MPI, and EU phytosanitary borders.
10-Tier Precision Manufacturing & Quality Control Protocol
Yield and tensile strength spectrometry on Q235B / Q355B steel coils.
High-precision laser and rotary shear cutting to exact coil strip widths.
High-speed automated continuous hydraulic punching of pitch patterns (50/75mm).
Progressive cold bending for heavy duty structural bracings and channel frames.
Continuous multi-roller profiling of omega uprights and box step beams.
Automated deburring, shot blasting, and edge rounding to remove scale.
CO₂ gas-shielded automated multi-axis robotic welding of beam connector clips.
Hot alkaline degreasing, acid pickling, and protective zinc phosphating immersion.
Automated electrostatic thermosetting epoxy-polyester powder cure at 200°C.
Deflection testing, film wrapping, steel banding, and ISPM-15 dunnage verification.
Frequently Asked Questions: Sourcing Flow Through Racking
Answers to common structural engineering, import compliance, and operational layout challenges encountered by international procurement managers.
What specific technical documentation is required to verify CE certification for flow-through racking?
How do you calculate the optimal lane gradient for different pallet materials (wood vs. plastic)?
Can your racking systems be engineered for high-seismic zones such as New Zealand or the Pacific Rim?
What is the standard ocean freight lead time and how are shipments protected against corrosion?
How does a gravity pallet flow system compare to a Radio Shuttle system in terms of Total Cost of Ownership (TCO)?
What information does HEDA require to provide a free 3D CAD layout within 24 hours?
Plan Your Warehouse Flow System with Licensed Engineers
Connect directly with Guangzhou Heda Shelves Co., Ltd.'s dynamic storage design desk. Obtain free 3D layout renderings, load-deflection calculation packages, and direct factory export pricing tailored to your facility parameters.