Engineered Industrial Racking Systems
Tested under rigorous FEM and EN standards, these heavy-duty storage configurations deliver high volumetric utilization, pallet safety, and seamless warehouse workflow integration.
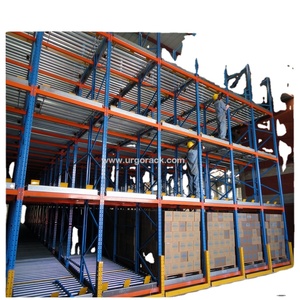
High Efficiency Order Picking Racking System, Gravity Flow Roller Racking System
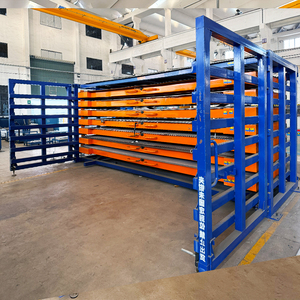
Industrial Steel Sheet Storage Rack with Roll-Out Shelves for Metalworking Shop, Factory Warehouse
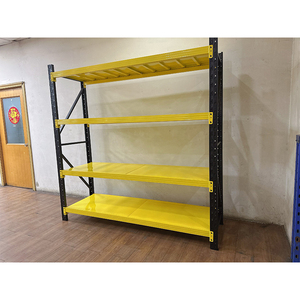
Factory Metal Display Shelf Industrial Warehouse Storage Rack Systems Heavy Duty Shelf Rack
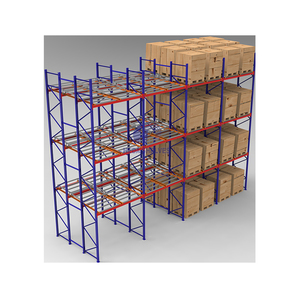
High-Density Steel 5-Layer Push-Back Pallet Racking System Heavy-Duty Warehouse Storage Solution
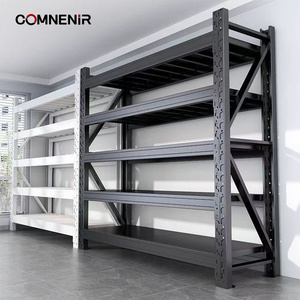
Industrial Shelving Warehouse Rack Heavy Duty Pallet Racking System for Distribution Centers CE Certified
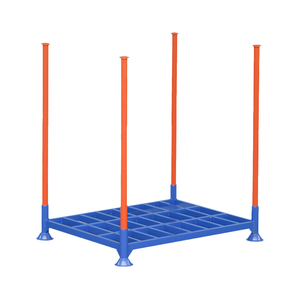
Heavy Duty Warehouse Metal Storage Rack Multi-Function Customized Steel Stack the Racking Intubated Stack Rack
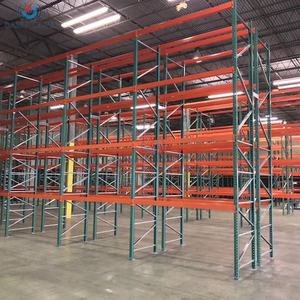
Selective Pallet Racking Pallet Racking Push Back Push Back Pallet Racking System
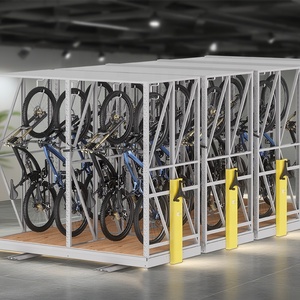
High Density Compact Mobile Shelving Storage System Manual Mobile Compactor for Sports Equipment Mobile Racking
Engineering Excellence in Heavy Industrial Racking: The CE Regulatory Paradigm
In modern supply chain architecture, static storage structures are no longer treated as passive metal shelving. Within high-throughput distribution hubs, automated fulfillment centers, and refrigerated cold chains, racking functions as a dynamically loaded structural entity. Under European and international structural directives, an industrial racking installation is classified as vital load-bearing steelwork governed by stringent safety thresholds. Sourcing from CE certified industrial racking systems factories & suppliers ensures that material composition, cold-formed section modulus, load deformation limiters, and connection fatigue resistances conform strictly to harmonized technical regulations.
The CE mark on warehouse racking certifies full compliance with Construction Products Regulation (EU) No 305/2011 (CPR), supported by EN 15512 (Steel static storage systems – Adjustable pallet racking systems – Principles for structural design), EN 15620 (Tolerances, deformations and clearances), and EN 15635 (Application and maintenance of storage equipment). Unlike conventional fabricated steel, structural racking utilizes thin-walled, high-tensile cold-formed steel sections (predominantly Q235B, Q355B, and EN 10025 grades) characterized by complex perforation arrays along upright columns. These perforations allow beam adjustability but induce localized buckling, torsional flexure, and distortional phenomena that can only be safely calculated through empirical testing and second-order finite element analysis (FEA).
The Structural Physics: Upright Deflection & Seismic Ductility
When engineering pallet systems carrying static loads up to 5,000 kg per beam level and overall bay capacities exceeding 30,000 kg, frame stiffness is governed by the moment-rotation performance of the beam-to-column connector. Guangzhou Heda Shelves Co., Ltd. implements cold-rolled 5-hook and 6-hook interlocking end-connectors with integral safety pins. This engineered geometry minimizes loose connector slack and optimizes joint rotational stiffness (spring stiffness $C_{d}$), keeping beam deflection below 1/200th (and in automated operations, 1/300th) of the clear span.
Furthermore, seismic engineering for active zones across New Zealand (NZS 1170.5), Australia (AS 4084), and Southern Europe requires customized baseplate anchor spacing, heavy-duty tubular X-bracing, and dynamic ductility factors ($q$-factors) that absorb seismic kinetic energy without sudden structural yield.
Tensile Strength & Metallurgy
Strict utilization of continuous strip steel from premier mills with certified yield strengths ($f_y \ge 355\text{ MPa}$), full elongation tests, and verified metallurgical purity for cold-bending integrity.
Perforation Mechanical Stability
Uprights are punched with computer-controlled continuous tooling at 50mm or 75mm pitches, engineered to avoid stress concentrations and resist shear-web buckling under maximum upright axial compression.
Surface Passivation & Finish
Complete 9-stage pre-treatment incorporating chemical degreasing, zinc-phosphating, and automated electrostatic thermosetting epoxy-polyester powder baking (60–90μm thickness) for superior corrosion and scratch resistance.
Engineering Selection & System Recommendation Matrix
Determining the ideal racking architecture requires balancing floor space footprint, floor load capacities, SKU turnover cycles, accessibility speed, and handling equipment capabilities. The table below outlines technical benchmarks across key industrial storage systems to guide engineering procurement teams.
| System Architecture | Floor Space Efficiency | Pallet Selectivity | Handling Rotation | Typical Beam/Level Capacity | Primary Industrial Application |
|---|---|---|---|---|---|
| Selective Pallet Racking | 40% – 50% | 100% Direct Access | FIFO / LIFO | 1,000 – 4,500 kg | General Warehousing, FMCG, 3PL Distribution, Retail Logistics |
| Push-Back Racking (2–6 Deep) | 70% – 80% | Medium (1 SKU per lane) | Strict LIFO | 1,000 – 2,500 kg per cart | Cold Storage, Food Processing, High-Volume Medium-Turnover SKUs |
| Gravity Pallet Flow Roller | 75% – 85% | Lane Dedicated | Strict FIFO | 800 – 2,000 kg per lane | Perishable Goods, Dairy, Pharmaceuticals, High-Velocity Pick Faces |
| Drive-In / Drive-Through | 65% – 75% | Low (Per Lane) | LIFO (Drive-In) / FIFO | 1,000 – 2,000 kg | Seasonal Bulk Buffers, Raw Beverage Ingredients, Frozen Cold Rooms |
| Radio Shuttle Automation | 80% – 90% | Automated Batch Access | Flexible FIFO & LIFO | 1,500 – 2,500 kg | Automated Deep-Lane Storage, High-Throughput Meat & Produce Plants |
| Heavy Duty Cantilever | 50% – 65% | 100% Direct Longitudinal | Free Access | 500 – 3,000 kg per arm | Timber Packs, Structural Steel Tubing, Bar Stock, Extrusions, Sheet Metal |
| Rack-Supported Mezzanine | 160% – 250% (Multi-Tier) | 100% Manual / Cart Access | Direct Picking | 300 – 1,000 kg/m² | E-commerce fulfillment, Automotive Spare Parts, High-SKU Carton Picking |
Strategic Procurement Trends: The Next Horizon in Warehouse Logistics (2025–2030)
The global warehousing landscape is undergoing transformative shifts driven by land scarcity, supply chain regionalization, and rising labour costs. Procurement directors and supply chain engineers are navigating fundamental shifts in how high-bay storage hardware is evaluated, purchased, and integrated:
1. Vertical Density Maximization Over Horizontal Footprint
With industrial land valuations reaching unprecedented highs in primary metropolitan belts across North America, Europe, Australia, and East Asia, warehouse ceiling heights are moving from standard 8–10 meters up to 14–24 meters. High-bay Very Narrow Aisle (VNA) systems and Automated Storage and Retrieval Systems (ASRS) require rack uprights rolled to micro-tolerances. Mill tolerances must be held to fractions of a millimeter to prevent cumulative vertical plumb-line deviations over multi-level tiers.
2. The Integration of Autonomous Mobile Robots (AMR) & Hybrid Shuttles
Traditional pallet handling relying solely on manually driven counterbalance or reach trucks is being augmented by autonomous guided vehicles (AGVs) and autonomous mobile shuttles. This evolution places critical mechanical demands on rack run rails, pallet stops, and guidance channels. Racking manufacturing must integrate tight-tolerance laser-cut docking guides, optical sensor clearance windows, and floor-level deflection barriers that ensure autonomous navigation reliability.
3. Life-Cycle Carbon Emissions & Green Steel Sourcing
Corporate ESG mandates and Carbon Border Adjustment Mechanism (CBAM) compliance in the European Union are transforming supplier vetting. Major enterprise buyers now demand certified raw steel traceability reports, low-carbon electric arc furnace (EAF) options, non-toxic heavy metal-free powder coatings (RoHS compliant), and recyclable structural materials. Long-term durability and resistance to structural degradation directly lower replacement frequency and life-cycle carbon footprints.
4. Seismic Resiliency & Stringent Building Codes
Insurance underwriters and municipal building authorities increasingly require full dynamic stress simulation for industrial rack installations. Storage systems installed in earthquake-prone zones must demonstrate energy dissipation capabilities through cold-formed ductile beam clips, expanded footplates, heavy anchor embedment depths, and cross-bay structural ties. Supplying engineering calculation packages signed by qualified structural specialists has become a mandatory prerequisite for global project permits.
Why Enterprise Sourcing Managers Choose Guangzhou Heda Shelves
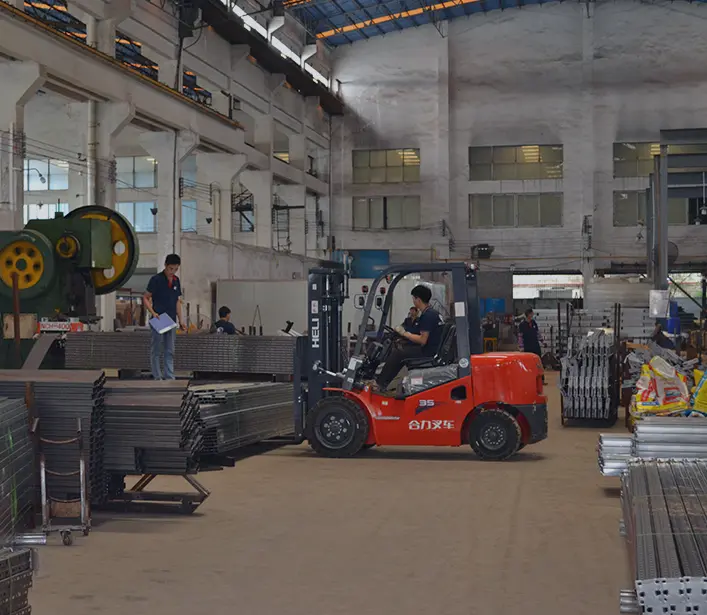
Established in 2001, Guangzhou Heda Shelves Co., Ltd. has developed into an internationally recognized engineering and manufacturing leader for high-tolerance industrial storage structures. Spanning a modern 30,000 m² production base staffed by over 300 technical specialists, our monthly cold-forming and structural fabrication capacity exceeds 30,000 metric tons.
The Heda Technical Advantage
We eliminate communication gaps and costly onsite modifications by functioning as an end-to-end engineering partner. Every layout begins with detailed structural modeling tailored to warehouse column spacings, building expansion joints, dock clearances, sprinkler arrays, and forklift turn radiuses.
- Complimentary 3D & CAD Layouts: Rapid 24-hour turnaround on comprehensive layout schemes optimizing pallet position density.
- Rigorous Standard Compliance: Designs developed with reference to CE (EN 15512), ISO 9001:2015, Australian Standard AS 4084, and American RMI principles.
- Biosecurity-Ready Packaging: Fully compliant ISPM-15 treated dunnage or dedicated heavy-duty steel transport stillages ensuring seamless customs clearance at Australian DAFF, New Zealand MPI, EU, and US ports.
- Direct Engineering Consultation: Complete calculation reports including base-plate anchor shear values, upright axial loads, and seismic load coefficients for your local engineering sign-off.
Our 10-Stage Precision Manufacturing Workflow
Quality assurance is embedded into every millimeter of our manufacturing chain. Uprights, box beams, and diagonal braces undergo continuous automated inspection across ten discrete production milestones:
Raw Material QC
Tensile yield, coil thickness, and chemical composition spectrometer verification.
Precision Slitting
High-speed CNC coil uncoiling, leveling, and high-tolerance longitudinal slitting.
Continuous Punching
Automated multi-station high-speed progressive punching of 50mm/75mm upright pitch.
Cold Roll Forming
24-station precision roll-forming lines ensuring exact cross-section profile geometry.
Beam Forming
Automated interlocked twin-C profile roll welding for heavy-duty box beams.
Robotic Welding
Multi-axis robotic GMAW welding of beam end-connectors with zero spatter.
Shot Blast / Polish
Mechanical surface scale removal and descaling to ensure optimal surface anchoring.
Phosphating Rinse
Multi-stage immersion degreasing, acid pickling, rust removal, and zinc-phosphating.
Electrostatic Coat
Thermosetting epoxy-polyester powder application cured at 200°C for extreme durability.
Final QC & Pack
Coating adhesion, thickness gauge testing, component bundle tagging, and export stillaging.
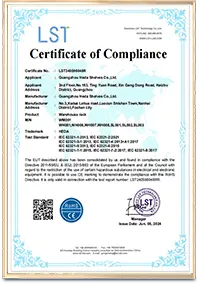
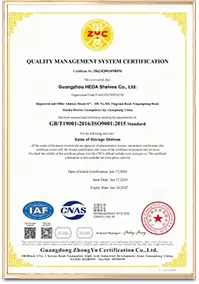
Verified Compliance Certificates
Transparency is foundational to our enterprise partnerships. All testing protocols and production processes are independently audited by accredited European notified bodies:
Technical & Commercial Frequently Asked Questions (FAQ)
Essential guidance for engineering consultants, warehouse directors, and international procurement managers sourcing industrial racking systems.
How does CE certification under EN 15512 protect commercial purchasers?
CE certification ensures that the racking manufacturer operates a certified Factory Production Control (FPC) system. Under EN 15512, all load capacity declarations are backed by physical stub-column testing, beam-to-connector bending tests, and shear resistance calculations rather than arbitrary estimates. This protects purchasers against sudden structural collapse, guarantees compliance with occupational health and safety laws, and provides insurers with verified load credentials.
What structural parameters are required to calculate warehouse slab point loading?
Our structural engineering team requires: (1) Concrete slab thickness and reinforcement detailing, (2) Subgrade modulus of reaction ($k$-value) or allowable concrete compressive bearing capacity ($f'c$), (3) Center-to-center upright bay spacing, and (4) Maximum total bay dead + live load. We calculate the footplate surface area and base anchor shear/pull-out forces to ensure the concentrated post loads do not punch through or crack the slab.
Can Heda racking be certified for seismic zones (e.g., NZS 1170.5 or Eurocode 8)?
Yes. Seismic engineering requires adjusting the cold-formed upright profile, upgrading baseplate steel grades, widening footplate bolt centers, and incorporating heavy-gauge diagonal spine bracing. Based on site-specific Spectral Acceleration coefficients ($S_s, S_1$), soil class, and importance levels, we provide customized FEA models and calculation packages for review by local certified engineers.
What surface finishes are recommended for sub-zero cold stores and humid environments?
For dry ambient warehouses, our 60–90μm electrostatic epoxy-polyester powder coat provides outstanding scratch and abrasion resistance. For cold storage freezers (-30°C) or high-humidity facilities (e.g., coastal ports, agricultural processing), we supply continuous pre-galvanised components (Z275 coating mass) or heavy-duty hot-dip galvanised structural components conforming to ISO 1461, eliminating micro-corrosion beneath the coating.
How are export shipments packed to meet international quarantine and biosecurity laws?
All export shipments leaving our Guangzhou plant are bundled on custom heavy-duty steel channel stillages or fumigated heat-treated timber bearing the official ISPM-15 IPPC stamp. This rigorous protocol prevents biosecurity quarantine stoppages and inspection re-treatment penalties at major destination ports such as Sydney, Melbourne, Auckland, Rotterdam, Hamburg, Los Angeles, and Long Beach.
What is the standard production lead time and international sea freight transit window?
Standard project production turnaround averages 15 to 25 working days depending on total steel volume, color customization, and accessories. Direct sea freight from nearby South China ports (Nansha, Huangpu, Shenzhen) takes approximately 12–18 days to Oceania ports, 20–28 days to the US West Coast, and 28–35 days to principal European container terminals. Full tracking and customs documentation (Bill of Lading, Commercial Invoice, Packing List, Certificate of Origin) are provided proactively.
Design Your High-Efficiency Warehouse Layout Today
Collaborate directly with Guangzhou Heda Shelves structural engineers. Submit your warehouse floor plan, ceiling clear height, pallet dimensions, and operational throughput targets to receive a fully engineered 2D/3D CAD layout and commercial proposal within 24 hours.