Heavy Duty
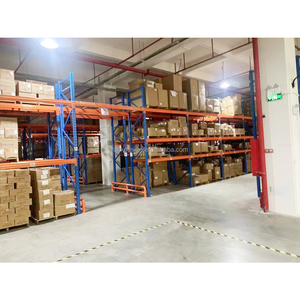
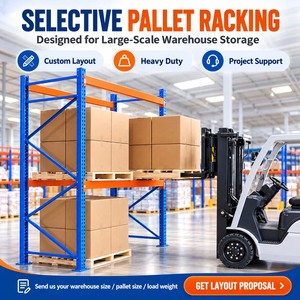
Industrial High Bay Selective Heavy Duty 24" Upright Pallet Rack
Upright: 90×70 / 120×95mm
Load: Up to 5,000 kg/tier
CE Certified
Explore our certified industrial warehouse storage modules, mobile-ready configurations, and heavy-duty structural components manufactured to EN 15512 and ISO 9001:2015 rigorous standards.
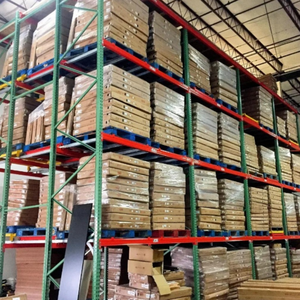
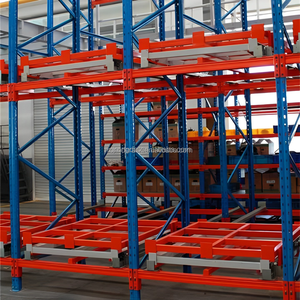
In contemporary logistics engineering, conventional static selective racking reserves upwards of 60% of floor area exclusively for vehicular access aisles. A CE Certified Movable Pallet Racking System (often recognized in automated warehousing as Motorized Mobile Racking or MOVO) eliminates redundant working aisles by mounting structural racking superstructure onto motor-driven, wheel-mounted mobile chassis that travel smoothly over recessed floor guidance rails.
By consolidating rows into a single dynamic block and opening a single aisle via intelligent remote or PLC command only when required, movable pallet racking achieves an instantaneous 80% to 100% surge in warehouse pallet storage capacity within the exact physical building perimeter, or cuts required cold-storage energy footprints by nearly 50%.
Guangzhou Heda Shelves Co., Ltd. engineers movable pallet racking superstructures conforming strictly to EN 15095 (Power-operated mobile shelving and racking safety requirements), EN 15512 (Cold-formed thin gauge steel design), and relevant international seismic design codes including AS 4084:2023 and NZS 1170.5. The entire mobile structure incorporates dual-flanged forged steel wheels machined to precision tolerances, synchronized drive shafts coupled directly with SEW or Nord helical-bevel gearmotors, and integrated multi-zone photoelectric optical curtains that enforce emergency stoppage within milliseconds of optical path interruption.
Detailed thermodynamic, economic, and volumetric utilization parameters benchmarked across common industrial warehouse racking topologies.
| Storage Topology | Footprint Area Utilization | Direct SKU Selectivity | Cold Store Energy Savings | Forklift Fleet Reqs | Compliance Standard |
|---|---|---|---|---|---|
| Movable Pallet Racking (MOVO) | 85% – 92% Maximum | 100% Random Access | 45% – 50% Reduction | Standard Counterbalance / Reach | CE (EN 15095) / AS 4084 |
| Conventional Selective Racking | 35% – 42% Low | 100% Random Access | Baseline (0% Savings) | Standard Counterbalance / Reach | EN 15512 / AS 4084 |
| Drive-In / Drive-Thru Racking | 65% – 75% High | Poor (LIFO / Block Stack) | 15% – 20% Reduction | Specialized Mast Cabins | EN 15620 / FEM 10.2.07 |
| Push Back Pallet Racking | 60% – 70% Medium-High | Moderate (Lane LIFO) | 18% – 22% Reduction | Standard Counterbalance | EN 15512 / RMI MH16.1 |
| Radio Shuttle Cart Racking | 78% – 85% High | Batch-Based FIFO/LIFO | 30% – 35% Reduction | Specialized Shuttle Transporters | CE Machinery / ISO 12100 |
Strategic vectors shaping international capital expenditure, cold-chain operations, and warehouse automation architectures from 2026 through the next decade.
With global industrial electricity tariffs elevating cold storage OPEX, procurement teams are rapidly abandoning static aisles. Movable pallet racking condenses refrigerated cubic meters by up to 50%, utilizing special low-temperature steel alloys (Q355D/E) and synthetic lubricants rated to -35°C that maintain peak mechanical viscosity without fracturing.
Modern procurement specifications mandate that movable racking PLC architectures (Siemens S7-1500 / Allen-Bradley) expose open industrial Ethernet interfaces (PROFINET, Modbus TCP, OPC UA). This enables automated reach trucks and AMRs to wirelessly call and open aisles automatically prior to arrival, slashing cycle times.
International tier-one safety auditors now reject non-certified mobile base imports. Procuring CE-marked systems guarantees compliant functional safety performance (PL d / SIL 2 rating), full perimeter multi-beam optical light grids, integrated rail sweepers, and audible/visual aisle deployment warnings that avert operator crushing hazards.
Supply chain operators increasingly demand mobile systems engineered for existing slab retrofits. Emerging procurement packages focus on ultra-flat guide rails directly laser-aligned and grouted into shallow concrete slab chases (under 120mm depth) using high-early-strength non-shrink epoxy grouts, preventing major warehouse shutdowns.
In seismically active markets such as New Zealand (NZS 1170.5) and the European Mediterranean, buyers specify automated mobile bases equipped with seismic sensors. When earth tremors exceed 0.05g, the entire mobile bank automatically switches to emergency idle, interlocking wheels with floor rails to damp base moments and prevent harmonic rack collapse.
Next-generation movable chassis incorporate continuous motor current transducers and wheel-rail vibration monitors. The collected telematics predict motor gearbox backlash, rail track debris obstructions, or structural beam deflection imbalances weeks before mechanical seizure, enabling automated maintenance ticket generation.
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. is an established industry pioneer delivering heavy-duty certified storage infrastructures, customized OEM/ODM fabrication, and turnkey engineering packages to over 130 countries worldwide.
Our mega-manufacturing footprint in Guangzhou houses continuous automated cold-roll-forming profile lines, high-precision laser tube cutting stations, robotic welding cells, and high-capacity electrostatic powder coating lines with an annual output exceeding 360,000 tons.
We furnish verifiable third-party certification: CE Certification No. 2435-CPR-8605159 conforming to EN 15095/Machinery Directives, and ISO 9001:2015 Quality Management System No. 18624Q00169R0M. Full metallurgical test reports and weld testing certifications are supplied with every bill of lading.
Our technical department comprises structural analysis specialists, electrical PLC software programmers, and warehouse spatial designers. We provide comprehensive free 3D CAD modeling, finite element analysis (FEA) beam simulation, and slab loading reports within 24–48 hours of project consultation.
Eliminating broker markups and intermediaries, our direct export model offers highly competitive capital cost savings of 25% to 40% compared to Western domestic fabricators, while maintaining premium Q235B/Q355B prime certified steel grades with superior tensile strength.
Shipments comply fully with international phytosanitary rules (ISPM-15 heat-treated dunnage) and robust steel transport stillages designed to simplify quarantine clearance across port authorities in Australia (DAFF), New Zealand (MPI), Europe, and North America.
Every shipment contains coded element tags matching step-by-step 3D assembly guides. We provide remote real-time tele-engineering assistance, PLC network flash updates, and on-site factory installation supervisors for large-scale logistics hub deployments.
HEDA Shelves operates with absolute transparency. Our heavy structural uprights, mobile mechanical carriages, and motor drive consoles undergo rigorous finite element verification, load testing, and independent quality inspections before packaging.
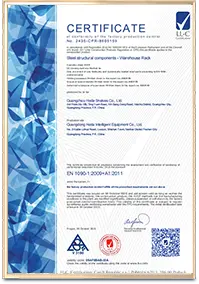
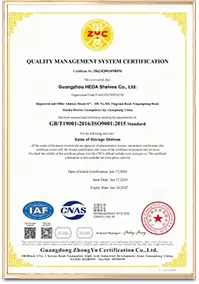
From certified steel coil intake to non-destructive weld testing, every structural component is tracked through strict ISO 9001:2015 stage gates.
Spectrometric tensile and yield verification of certified Q235B/Q355B hot-rolled sheet.
CNC slitting into calibrated ribbon widths with micro-tolerances under ±0.2mm.
High-speed hydraulic punching dies create continuous 50mm/75mm adjustment pitch slots.
Multi-stand continuous cold roll mills bend steel into stiffened omega upright profiles.
Box beam roll-forming with double-seam interlock delivering superior torsion resistance.
Automated multi-axis robotic welders bond beam end connectors with deep penetration.
Multi-stage immersion cleaning baths strip mill scale, applying chemical bonding primers.
Electrostatic GEMA powder coating baked at 200°C for superior scratch and salt resilience.
Assembly of forged dual-flange wheel blocks, high-torque gearboxes, and rail aligners.
Steel strap bundling with protective corner guards and ISPM-15 fumigated timber dunnage.
Direct technical and commercial answers addressing slab engineering, floor tolerances, safety certifications, and logistics implementation.
Movable pallet racking systems require precise floor levels to ensure wheel carriages operate smoothly without excessive drive motor strain. Slabs typically must comply with DIN 18202 Table 3 Group 4 or TR34 Free Movement (FM2) standards. Floor rail installation can be achieved by cutting shallow chases into an existing cured slab or casting rails directly into a new secondary screed pour.
Conforming to CE Machinery Directive 2006/42/EC and EN 15095, our mobile bases feature continuous optical light barrier grids at foot level (200mm) and upright height across each movable base aisle face. If a forklift operator, pedestrian, or discarded pallet breaks the optical beam during base movement, power to the variable-frequency motor drives is instantly cut, and fail-safe electromagnetic brakes engage.
Yes. Mobile racking is widely utilized in sub-zero refrigerated facilities because condensing aisles reduces chilled air volumes by up to 50%. For sub-zero installations, we specify fine-grain structural steels exhibiting high Charpy V-notch impact toughness (e.g., Q355D/E), anti-condensation heating strips inside electrical enclosures, and specialized low-temperature synthetic lubricants inside IP65-rated drive gearmotors.
All movable bases are fitted with secondary mechanical clutch releases. In the event of an electrical blackout, an integrated hand-crank ratchet or auxiliary manual towing adapter allows maintenance staff to safely disengage the drive gears and manually separate carriages, ensuring essential pallets remain accessible for emergency order processing.
We provide a complete structural engineering dossier with every export shipment. This includes certified raw steel mill certificates, section modulus calculations for uprights and box beams, finite element deflection profiles, and localized seismic tie-back calculations. This technical package allows your certified Australian or New Zealand engineer to sign off the installation quickly.
Standard factory fabrication for customized movable pallet racking orders (10 to 50 mobile bases) averages 25 to 35 calendar days. Ocean freight from our South China shipping terminal (Nansha/Shekou) to major global ports runs approximately 12–18 days to Australia/New Zealand, 22–30 days to Western European hubs (Rotterdam, Hamburg), and 18–26 days to US West Coast terminals.
Yes. Our electrical control cabinets utilize high-reliability industrial microprocessors (Siemens S7 series) featuring open communication protocols. Through standard Modbus TCP or Ethernet/IP interfaces, your WMS can dynamically pre-position aisles based on scheduled pick lists or automated reach truck guidance sequences, eliminating operator wait times.
For standard ambient distribution warehouses, our durable 70–90 micron electrostatic epoxy-polyester powder coat provides outstanding abrasion resistance. For tropical regions (e.g., Queensland, Pacific Islands) or fertilizer and chemical warehouses, we supply structural uprights and chassis hot-dip galvanized to ISO 1461 standards (exceeding 85 microns coating thickness), guaranteeing decades of corrosion protection.
Connect directly with HEDA Shelves' technical engineering department. Share your warehouse CAD drawing, clear ceiling height, pallet unit weights, and forklift specifications to receive an engineered 3D layout simulation and detailed cost quotation within 24 hours.