Top-Tier Industrial Storage & Movable Racking Solutions
Factory-direct high-density storage solutions engineered to maximize volumetric utilization, accelerate FIFO/LIFO turnover, and satisfy stringent global structural benchmarks including AS 4084, EN 15512, and RMI standards.
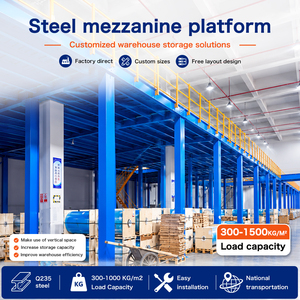
Heavy-Duty Warehouse Mezzanine Floor Storage Rack Platform
- Capacity: 300 – 1,000 kg/m²
- Multi-tier vertical expansion
- Heavy cold-rolled structural steel
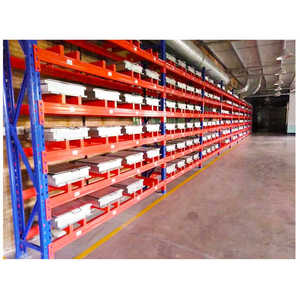
High-Density Drive-In Pallet Storage Narrow Lane Rack System
- Up to 80% footprint reduction
- Engineered for cold chain & batch SKUs
- Deep lane continuous pallet rails
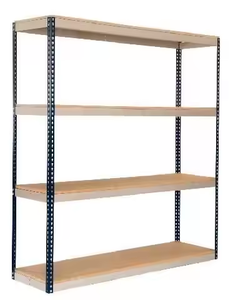
Customized Light & Medium-Duty Steel Warehouse Storage Shelving
- Capacity: 100 – 350 kg/level
- Boltless fast-clip configuration
- Scratch-resistant epoxy powder coat
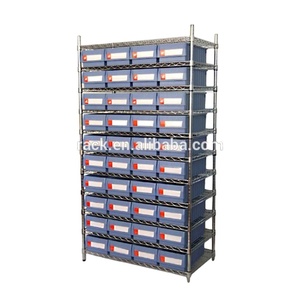
Multi-Layer 800lbs Heavy-Duty Industrial Wire Storage Rack
- Heavy wire grid load distribution
- High ventilation & sprinkler passthrough
- NSF hygiene compliant finish
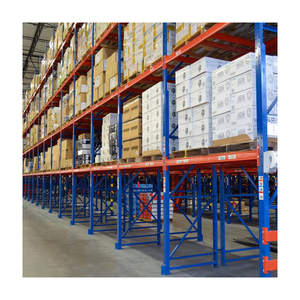
Wholesale Industrial Heavy-Duty Selective Pallet Racking
- 100% direct pallet selectivity
- Load: 1,000 – 4,500 kg per level
- AS 4084 / CE structural calculation
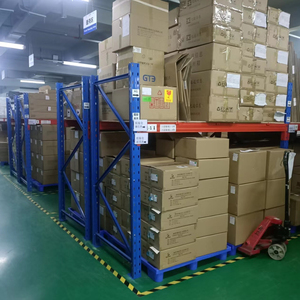
5-Layer Adjustable Heavy-Duty Bolted Pallet Racking Structure
- 75mm/50mm pitch height adjustment
- Reinforced interlocking safety pins
- Upright thickness up to 2.5mm
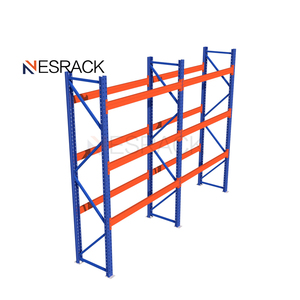
Custom Multi-Tier Heavy-Duty Industrial Selective Storage Racks
- High-tensile Q235B & Q355B steel
- Custom beam spans up to 3900mm
- Heavy row-spacers & upright protectors
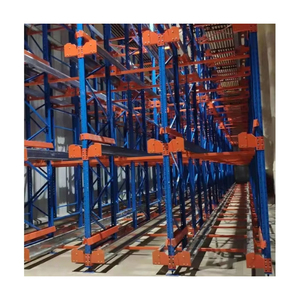
High-Efficiency Radio Shuttle Automated Deep-Lane Pallet System
- Autonomous radio runner shuttle cart
- Zero forklift travel inside storage aisles
- Seamless WMS / PLC system integration
Kinematics, Floor Tolerances & Steel Grade Mechanics of Movable Racking
A deep technical appraisal of movable racking (electrical mobile racking & runner shuttle platforms) versus static layouts, evaluating volumetric density index, floor slab deflection tolerances, and seismic safety factors.
Modern industrial logistics requires reconciling two fundamentally conflicting priorities: maximizing volumetric footprint utilization while maintaining rapid SKU accessibility. Conventional selective static pallet racking dedicates as much as 60% of total floor surface area to operational forklift aisles. In high-value footprint sectors—such as sub-zero cold chain facilities, dangerous goods bunkers, and urban 3PL fulfillment hubs—maintaining empty aisles carries crippling operational expenditure (OPEX) in thermal leakage and square-meter rental costs.
Movable warehouse racking (MOVO / motorized mobile base systems) mitigates this inefficiency by mounting conventional heavy-duty superstructure frames onto electrically driven, heavy-duty mobile bogies running along sub-floor embedded guide rails. By dynamically opening a single operational access aisle on demand via PLC optical sequencing or radio frequency identification (RFID) dispatch, movable storage systems instantly compress spatial footprints by 80% to 90% compared to static selective frameworks, effectively doubling usable pallet capacity without expanding real estate boundaries.
| Racking Architecture | Storage Density Index | Pallet Selectivity | Forklift Travel In-Rack | Cycle Throughput Speed | Seismic Damping Compliance | Typical Capex / Pallet |
|---|---|---|---|---|---|---|
| Electric Movable Racking | Ultra-High (85-92%) | 100% (Individual Aisle Open) | None (Outer Face Only) | Moderate – Controlled | Class 1 (Automatic Lock Interlocks) | $$$ (Medium-High) |
| Radio Shuttle Runner | Ultra-High (80-90%) | Lane Dependent (FIFO/LIFO) | Zero (Autonomous Carrier) | Very High (Fast) | Class 1 (Rigid Self-Braced Block) | $$$$ (Automation Grade) |
| Drive-In / Drive-Thru | High (70-80%) | Poor (Last-In-First-Out) | High Impact Exposure | Low (Slow Cautious Travel) | Requires Reinforced Base Plates | $ (Economical) |
| Push-Back Cart Racking | Moderate-High (65-75%) | Moderate (2-6 Deep Carts) | Aisle Face Only | Moderate-Rapid | Standard Base Fixtures | $$ (Moderate) |
| Rack-Supported Mezzanine | Vertical Doubled (100%+) | 100% Selective / Hand Pick | Pedestrian / Order Picker | High (Multi-tier parallel picks) | Full Moment-Resisting Frame | $$$ (Structural Grade) |
| Standard Selective Rack | Baseline (40-45%) | 100% Direct Immediate | Full Dedicated Aisles | Rapid Standard | Standard Anchor Patterns | $ (Base Level) |
Mechanical Metallurgy & Structural Tolerances
Guangzhou Heda Shelves Co., Ltd. manufactures heavy industrial upright columns and box-welded beams utilizing prime cold-rolled steel coils graded to Q235B ($F_y = 235\text{ MPa}$) and high-stress structural Q355B ($F_y = 355\text{ MPa}$, equivalent to ASTM A572 Grade 50 and European S355JR). For movable racking systems, torsional rigidity and column camber/sweep tolerances are strictly calibrated within $L/1000$ limits. Because a moving racking bank exerts intense localized wheel-point loads (often exceeding 8 to 15 metric tons per bogie assembly onto embedded guidance rails), slab flatness and levelness according to DIN 18202 Table 3 Group 4 or ASTM E1155 ($F_F \ge 50, F_L \ge 45$) must be verified to prevent derailment, premature flange wear, or excessive motor amp draw.
Every movable chassis manufactured by HEDA features fail-safe optical beam curtains along aisle approaches, dual emergency trip bars at ground level, seismic accelerometer triggers that mechanically lock brake cams during tectonic events, and soft-start/stop variable frequency drives (VFD) that protect top-heavy palletized loads against acceleration-induced dynamic toppling.
25 Years of Factory-Direct Engineering Excellence & Global Export Scalability
Established in 2001, Guangzhou Heda Shelves Co., Ltd. operates a premier 30,000 m² production facility equipped with high-precision roll-forming lines, automated punching arrays, and robotic weld cells.
10-Stage Precision Manufacturing & Quality Control Pipeline
Every component—from base plate to beam lock—undergoes rigorous metallurgical and dimensional inspection prior to containerization.
Raw Coil Testing
Spectrometric & tensile yield testing of prime Q235B/Q355B coils.
Slitting & Cutting
CNC high-speed slitting with edge deburring within ±0.1mm tolerance.
Column Punching
Continuous multi-station high-speed automatic punch line.
Cold Roll-Forming
Progressive 22-roller cold bending ensuring zero micro-fractures.
Profile Straightening
Automated laser alignment eliminating residual longitudinal twist.
Robotic Welding
CO&sub2; shielded automatic robot arms for beam connector plates.
Acid Pickling
Multi-tank chemical degreasing, rust removal, and water rinsing.
Phosphating Bath
Micro-crystalline phosphate conversion coating for corrosion arrest.
Electrostatic Powder
Thermoset epoxy curing at 180–200°C; 80–120μm uniform thickness.
QC & Bundling
Deflection testing, film wrap, steel strapping onto sea-freight stillages.
Emerging Engineering & Procurement Trends in Movable Warehouse Racking
Intralogistics procurement is transitioning from static steel tonnage buying to digitized, modular, and climate-resilient storage ecosystems.
Cold Chain Decarbonization
With industrial refrigeration accounting for 60% of cold store operating expenditure, moving racks allow cooling cubic volumes to shrink by 45%. Future procurement will demand low-temperature-tolerant alloy steel resilient against ductile-to-brittle transitions at -30°C.
AMR & AGV Integration
The shift away from human-driven reach trucks toward Autonomous Mobile Robots (AMRs) mandates that movable racking systems incorporate API-based handshake protocols. Automated open/close aisle triggers now synchronize directly with fleet dispatch software.
IoT Structural Health Sensing
Modern enterprise specifications increasingly specify embeddable strain-gauge telemetry and tilt sensors on upright bases. Real-time impact logs alert warehouse operators immediately to forklift collisions, preventing progressive structural collapse before it occurs.
CBAM & Circular Metallurgy
Under the European Carbon Border Adjustment Mechanism (CBAM) and green supply-chain mandates, global buyers require mill certificates validating scrap-to-steel recycled content, lower blast-furnace emissions, and VOC-free electrostatic powder coat chemistries.
The Shift Toward Modular Hybrid Densification
Rather than relying exclusively on a single racking philosophy, high-throughput fulfillment centers now combine heavy selective pallet bases, upper-level radio shuttle deep storage channels for reserve stock, and rack-supported mezzanine walkways for rapid tier-1 manual piece picking. By sourcing from a direct manufacturer with end-to-end tooling versatility, supply chain planners cut procurement lead times, standardize interchangeable spare parts (such as locking beam pins, footplates, and column anchors), and capture significant economies of scale across multi-facility overseas rollouts.
Technical & Commercial Guidance for Overseas Racking Buyers
Answers to key engineering, seismic compliance, floor slab prerequisites, and container logistics questions asked by international supply-chain procurement teams.
Plan Your High-Density Storage Project with HEDA Engineers
Send us your warehouse CAD floor plan, ceiling clear heights, and pallet specifications. Our intralogistics design team will deliver a comprehensive 3D layout rendering, pallet position calculation, and detailed factory quote—free of charge within 24 hours.