Featured Industrial & Tall Pallet Racking Units
From single-bay selective units to high-density semi-automated deep lane profiles, examine our top 8 factory-engineered racking systems precision-built in our 30,000 m² workshop.
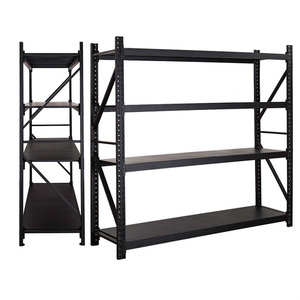
Boltless 5-Layer Steel Rack System Heavy Duty Shelving Units
Constructed with high-tensile cold-rolled steel, this boltless assembly framework guarantees quick deployment and rugged multi-tiered manual picking stability.
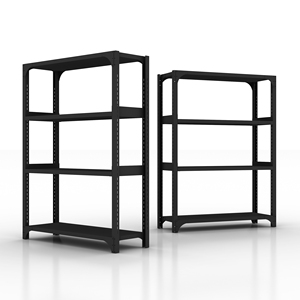
Cheap Metal Light Duty Rack, Steel Light Duty Pallet Racking
Budget-optimized warehouse storage unit configured for manual box loading, intermediate picking bins, and high-frequency light stock management.
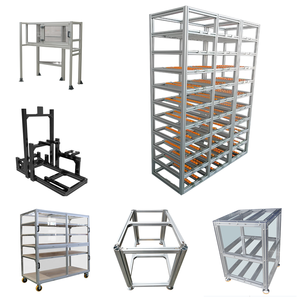
All-in-One Industrial Aluminum Profiles Framing Display Flow Rack Stand
Engineered for cleanroom or production peripherals, featuring extruded high-grade aluminum profiles, modular protective guard enclosures, and adaptable flow channels.
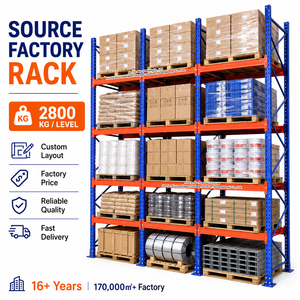
2800KG 5 Levels High Bay Industrial Pallet Racking Heavy Duty System
Engineered specifically for tall warehouse verticality. Verified to safely sustain 2800KG per beam tier across 5 vertical storage bays under heavy forklift cycles.
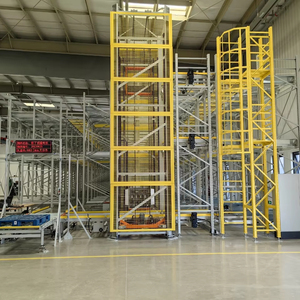
Intelligent Selective Pallet Rack With Efficient Conveying System
Integrated with automated vertical transport, automated guided vehicles, or roller lines for rapid cross-dock dispatching and reduced warehouse footprint overhead.
Steel Warehouse Rack Systems Storage with Shelving Units and Stairs
A complete multi-tier structural platform leveraging bottom vertical uprights as column supports, multiplying usable floor areas through integrated structural stairs.
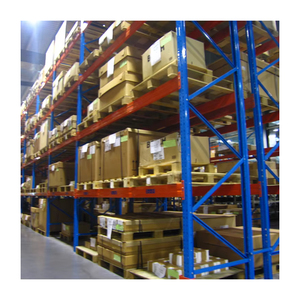
Heavy Duty Rack Industrial Pallet Storage Warehouse Metal System
Versatile selective racking solution built for 100% pallet accessibility. Features robust teardrop or diamond slot upright punchings for beam repositioning.
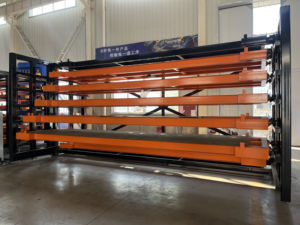
Multi-Tier Carbon Steel Powder Coated Anti-Rust Racking System
Treated through a comprehensive 10-step pickling, phosphating, and electrostatic powder coating cycle to withstand cold storage humidity and saline port conditions.
Why Import Tall Pallet Racking from Our China Factory?
Managing tall racking imports exceeding 12m clear heights demands strict engineering controls, verified metallurgy, and full alignment with international safety standards.
Rigorous Structural Engineering (AS 4084 & RMI Referenced)
Every high-bay rack is modelled using finite element analysis (FEA). We calculate section properties, beam deflection thresholds under L/200 limitations, upright torsion resistance, and frame stability under both dynamic forklift impact and site-specific seismic parameters.
30,000 m² Facility & 30,000 Tons Monthly Output
Established in 2001 in Guangzhou, HEDA Shelves utilizes automated continuous profile roll-forming mills, automated CNC punching, robotic welding stations, and a closed-loop electrostatic powder coating tunnel guaranteeing consistent weld penetration and coating adhesion.
Verified Certifications: CE & ISO 9001:2015
Unlike trading houses, we publish transparent verification credentials: CE Certification No. 2435-CPR-8605159 and ISO 9001:2015 Registration No. 18624Q00169R0M. Complete raw material mill certificates (MTC) accompany every container.
Biosecurity & Strict Export Dunnage Packaging
Exporting heavy steel components requires moisture-controlled sea stowage. We utilize reinforced steel stillages, heavy plastic wrapping, and certified ISPM-15 heat-treated timbers to ensure rapid port clearance through biosecurity agencies like Australian DAFF and NZ MPI.
Complimentary 3D CAD & Optimization Simulation
Send us your warehouse CAD floor plan, column grid intervals, beam clear heights, and material handling unit (MHE) specs. Within 24-48 hours, our technical engineering team delivers custom layout designs maximizing cubic pallet positions by 25% to 40%.
Engineering Tall Pallet Racks: Safety, FEA, and Deflection Limits
Tall racking installations (heights above 8 to 15 meters) introduce critical physical forces absent in standard shelving. Understanding these structural criteria protects supply chain assets and operator lives.
Upright Column Geometry & Critical Buckling Length
As rack upright columns increase in height, structural capacity is constrained primarily by Euler buckling rather than steel compressive yield strength. In tall installations, horizontal and diagonal frame bracings must be engineered with minimal unbraced lengths ($L_{cr}$).
Our upright sections are formed through continuous cold-rolling from premium Q235B / Q355B micro-alloyed carbon coils. Profiles incorporate multiple stiffening ribs along the web and flanges, drastically elevating torsional rigidity and warping resistance under dynamic forklift interaction.
Additionally, anchor footings are expanded with dual-anchor heavy baseplates transferring moment forces directly into warehouse concrete slabs without localized spalling or anchor bolt shear failure.
| Height Class | Standard Upright | Safety Anchor Spec | Recommended Beam Connection |
|---|---|---|---|
| Standard (<6m) | 80 x 60 x 1.8mm | Single M10 x 80mm | 3-Hook Wedge Connector |
| High Bay (6-10m) | 100 x 70 x 2.0mm | Dual M12 x 100mm | 4-Hook Dual-Claw Pins |
| Super Tall (10-16m+) | 120 x 95 x 2.5-3.0mm | Heavy 4-Bolt Base Plate | 5-Hook Robotic Weld Connector |
| Automated High Bay | Custom Boxed Upright | Chemical Capsule Anchoring | Bolted Heavy Splice Connection |
| Test Parameter | Global Requirement | HEDA Shelves In-House Quality Standard |
|---|---|---|
| Deflection Limit | Max Span / 200 | Controlled Span / 250 (Conservative Margin) |
| Safety Factor | 1.4 - 1.5 against yield | 1.65 Structural FEA verification factor |
| Powder Coating | 60-80 microns | 80-110 microns thermo-cured polyester |
| Impact Resistance | Post-protectors optional | Reinforced column wrap guards standard |
Seismic Engineering & Horizontal Load Dissipation
In seismic-active zones across the Pacific Rim, tall racking behaves as a non-building structural entity susceptible to harmonic resonance during ground acceleration. Standard static load tables are insufficient for seismic installations.
HEDA Shelves performs dynamic structural modeling calculating response spectrum analysis based on local seismic ground hazard coefficients ($C_h$). For seismic requirements, we integrate:
- High-capacity top-tie bracing across rack aisles to equalize lateral sway.
- Heavy-duty row spacers transforming adjacent single runs into interconnected rigid trusses.
- Energy-dissipating base plates calibrated to absorb cyclical shear displacement.
Future Procurement Trends for Tall Racking Systems
Modern distribution logistics is experiencing a generational shift. As industrial real estate land premiums surge, warehouse procurement executives must design for automation, green materials, and extreme verticality.
Convergence of Pallet Racks & Shuttle AS/RS
Procurement is shifting away from purely manual selective tall racks toward hybrid radio shuttle systems. Semi-automated deep-lane shuttles minimize forklift traffic inside tall bays, reducing post strikes and slashing order retrieval cycle times by over 50%.
14m+ Very Narrow Aisle (VNA) Adoption
To counteract rising warehouse lease costs per square meter, logistics managers are raising clear ceiling heights. VNA tall racking reduces aisle widths down to 1.6 - 1.8 meters, delivering up to 60% cubic density gains when paired with turret trucks or wire-guided reach machines.
High-Performance Sub-Zero Thermal Coatings
With perishable food e-commerce booming, demand for refrigerated tall racks is accelerating. High-humidity freezing conditions cause micro-cracks in low-tier coatings. Buyers now specify specialized anti-embrittlement zinc primers and heavy galvanization.
Full Digital Traceability & Factory QA Audits
Procurement heads increasingly reject unverified middleman vendors. Enterprise clients demand raw steel coil batch testing (MTC), certified chemical composition analyses, automated ultrasonic weld tests, and real-time remote factory video inspections.
Recyclable Green Steel & Low VOC Finishes
Corporate ESG goals are impacting warehouse equipment specifications. HEDA Shelves utilizes closed-loop powder recycling, zero-emission pretreatment cleaning lines, and responsibly sourced, 100% recyclable structural carbon steel.
HEDA's 10-Step High-Bay Racking Manufacturing Workflow
Every component destined for your facility undergoes a standardized, repeatable manufacturing sequence ensuring dimensional tolerance within tenths of a millimeter.
Raw Steel QA
Spectrometry & tensile yield verification on Q235B coils.
Slitting & Cut
CNC high-precision slitting into strip widths.
CNC Punching
Continuous 50mm/75mm teardrop/diamond pitch punching.
Roll Forming
Multi-station cold rolling forming complex upright bends.
Beam Profiling
Box & interlocking step-beam seam fabrication.
Robotic Welding
Carbon dioxide shielded automatic welding of end connectors.
Shot Blasting
Surface rust removal achieving SA2.5 roughness profile.
Phosphating
Chemical acid pickling & anti-corrosion barrier bath.
Powder Coating
Automatic electrostatic curing at 180°C - 200°C.
Stillage Packing
Component strapping into modular steel handling pallets.
Frequently Asked Questions on Importing China Tall Racking
Detailed answers addressing engineering compliance, shipping transit, biosecurity certifications, and on-site assembly for overseas EPC projects.
We do not provide vague assertions. For every project, our engineering department provides comprehensive calculation reports specifying steel grade tensile properties, weld throat thickness, safety factor against buckling, and deflection performance under full rated live load. These documents enable third-party certifiers and local site engineering officials to grant immediate regulatory compliance sign-offs.
Racking components are long, heavy, and awkward to handle. Rather than loose bundling, our upright frames and beam packs are pre-bundled on specialized heavy-gauge steel stillages with lifting channels. This design allows your destination yard forklifts to unload a 40HQ container in under 45 minutes without scratch damage or bending risks.
Yes. We regularly manufacture custom upright depths (e.g., 850mm, 1000mm, 1100mm, 1200mm) and clear beam spans (such as 2590mm, 2743mm, 3810mm) specifically calculated for pallet overhang requirements, internal flue spaces, and in-rack fire sprinkler clearance regulations.
Standard production for custom high-bay systems of 1 to 5 shipping containers typically completes in 20 to 28 business days. Transit time from South China seaports (Guangzhou / Shenzhen) averages 14-25 days to Australia/NZ, 20-30 days to the US West Coast, and 28-35 days to European hubs.
Yes. We act as the dedicated manufacturing backbone for storage equipment brands globally. We can match your corporate RAL powder coating colors, embed custom punched logo markings, and supply neutral or private-labeled engineering safety rating plates on all shipments.
We supply a complete document pack including Clean On-Board Ocean Bills of Lading, detailed itemized Packing Lists matching piece-level bundle marks, Commercial Invoices, and Official Certificates of Origin (e.g., Form A, Form E, ChAFTA) allowing eligible buyers to claim preferential tariff treatments.