Featured Industrial Warehouse Racking Systems
As an established heavy-duty racking exporter and OEM manufacturer, we supply certified cold-rolled structural steel systems, drive-in frames, mezzanine solutions, dynamic push-back carts, and mobile bases engineered for maximum volume utilization and load safety.
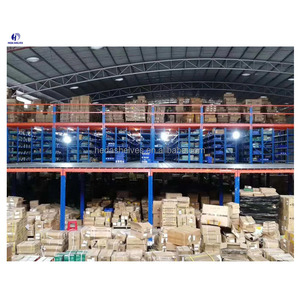
Heavy-duty structural uprights transform vertical warehouse airspace into modular picking and multi-tier pallet storage decks with integrated safety gates.
Phosphated and electrostatic epoxy coated heavy-duty steel beam profiles delivering rigid stability up to 4,500 kg per level for multi-pallet logistics.
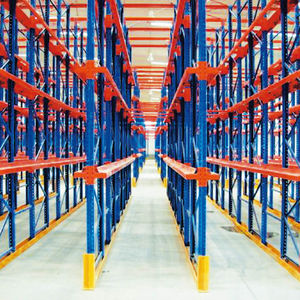
Maximum spatial efficiency eliminating conventional forklift aisles. Designed specifically for batch inventory, cold rooms, and identical SKU consolidation.
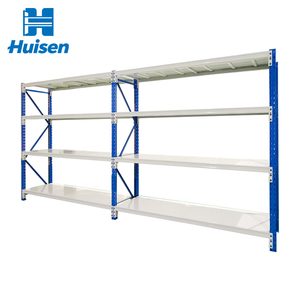
Tool-less pitch adjustment engineered for distribution centers, e-commerce fulfillment hubs, and spare parts catalog storage requiring rapid hand picking.
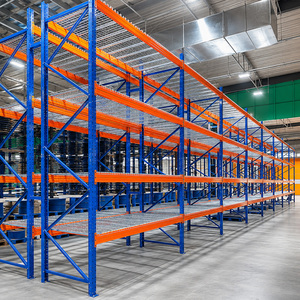
Heavy structural load distribution designed for irregular automotive packaging, engine components, sub-assemblies, and high-frequency staging docks.
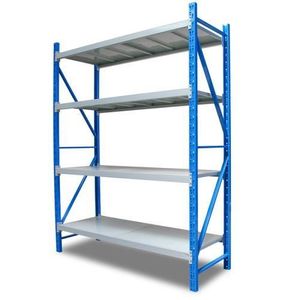
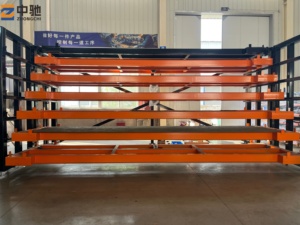
Open-span front column architecture carrying up to 3,000 kg per arm for timber profiles, structural steel tubing, extruded plastic pipe, and metal coils.
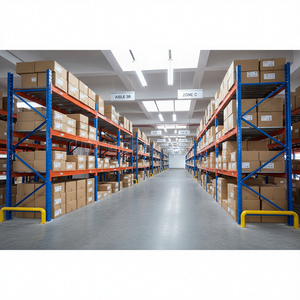
Telescoping nested cart mechanism operating on gravity inclination. Stores 2 to 6 pallets deep per lane while isolating each level's distinct picking face.
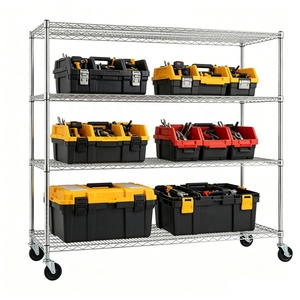
Heavy-duty movable wire storage carts equipped with smooth-gliding locking polyurethane casters, certified for food hygiene, laboratories, and cleanroom handling.
Engineering Whitepaper: High-Density Movable Pallet Racking Systems
Modern supply chain real estate costs demand higher cubic density. Custom OEM movable pallet racking (also known as Mobile Pallet Racking or Powered Mobile Base Systems) shifts heavy racking superstructures along in-floor guide rails, compressing traditional multiple access aisles into a single dynamically opened corridor.
Structural Chassis & Dual-Flange Wheels
Unlike standard static frames bolted directly to concrete floor slabs, movable racking relies on custom-welded structural steel base carriages (welded box girders or cold-formed channels). These motorized carriages rest on precision-machined dual-flange steel wheels running on embedded, flush-mounted floor rails. Floor rail leveling tolerances must adhere to stringent DIN 18202 standards (often within ±1.5 mm across a 30-meter track) to guarantee zero crabbing or lateral drift during full-capacity movements.
Synchronized Multi-Drive Geared Motors
Long mobile carriage assemblies—often stretching from 20 to 80 meters and bearing total live loads exceeding 800 metric tons—require distributed planetary geared motors interconnected via a centralized programmable logic controller (PLC). Variable Frequency Drives (VFD) govern dynamic acceleration and deceleration ramps, preventing kinetic pallet load tipping. Safety laser perimeter scanners, photoelectric light curtains, and mechanical emergency trip-bars instantly halt motion should any obstruction enter the active aisle.
Thermal & Cold Storage Thermodynamic Balance
Movable pallet racking delivers its fastest ROI within cold storage facilities (−25°C to −30°C) where operational refrigeration overhead scales directly with total refrigerated building volume. By consolidating storage footprints by 40% to 50%, operators cut down heat dissipation surface area and power consumption. Electrical enclosures use IP65 hermetic sealing, low-temperature gear oils, heating elements in control panels, and specialized low-temperature impact-resistant ductile steel alloys (Q355D/E).
Engineering Matrix: Movable Racking vs. Traditional High-Density Formats
| Storage Architecture | Floor Space Utilization | SKU Selectivity Ratio | Stock Rotation Logic | Forklift Damage Exposure | Cold Store Thermodynamic Score |
|---|---|---|---|---|---|
| Powered Movable Racking | 85% – 90% (Ultra High) | 100% (Direct Access to Every Pallet) | FIFO or LIFO Fully Configurable | Extremely Low (Trucks never enter racks) | Optimal (Minimum cubic refrigeration footprint) |
| Standard Selective Racking | 40% – 50% (Aisle Intensive) | 100% (Individual Access) | FIFO / LIFO Direct | Moderate (High exposure in picking aisles) | Poor (High volume of cooled air in aisles) |
| Drive-In / Drive-Through | 70% – 80% (High Density) | 15% – 25% (Honeycombing Loss) | LIFO Strictly (Unless drive-through) | High (Trucks operate inside rack bays) | Good (Low empty volume, high density) |
| Push-Back Nested Carts | 65% – 75% (Medium-High) | 40% – 60% (Lane Dedicated) | LIFO (Gravity nested retrieval) | Low (Forklift remains in front aisle) | Moderate (Deep storage without floor power) |
| Radio Shuttle Automation | 80% – 85% (Very High) | 30% – 50% (Batch Grouping) | FIFO / LIFO Dynamic | Very Low (Autonomous shuttle handling) | Very Good (High speed, deep lane storage) |
Future Procurement Trends: What Global Buyers Must Factor for 2026–2030
Procurement directors, supply chain VPs, and third-party logistics (3PL) infrastructure consultants are transitioning from measuring simple "cost per pallet position" to adopting a comprehensive Total Cost of Ownership (TCO) lifecycle approach.
WMS & AGV/AMR Fleet Integration
Movable pallet racking is moving away from purely manual pendant or button actuation. Modern projects integrate with automated guided vehicles (AGVs) and autonomous mobile robots (AMRs). The Warehouse Management System (WMS) communicates over industrial Wi-Fi or 5G to open the requested aisle automatically as the AGV approaches, eliminating truck waiting idle times and boosting hourly throughput.
Seismic Damping & Dynamic Base Isolation
In seismically active markets—such as New Zealand (NZS 1170.5), Japan, the US West Coast, and parts of Europe (EN 1998)—racking failure risks catastrophic inventory loss and human danger. OEM engineering now integrates base-level seismic decoupling dampers and hydraulic kinetic absorption mechanisms into the mobile carriage chassis to absorb ground acceleration waves before they transfer into the top tiers.
Hybrid Modular Retrofitting
Rising construction costs and long permit schedules favor brownfield conversion over new site builds. Buyers increasingly specify modular mobile bases capable of reusing existing uprights and beams. Standard static selective racking frames are remounted onto engineered powered carriages, upgrading capacity from 5,000 pallet positions to over 9,200 within identical warehouse exterior boundaries.
Smart IoT Structural Health Monitoring
Embedded strain gauges, optical deflection sensors, and vibration monitoring nodes track beam deflection, structural tilt, and bearing wear in real time. Maintenance alerts signal potential bearing misalignment, track fouling, or accidental forklift impacts before mechanical failure occurs, ensuring uninterrupted operation for 24/7 fulfillment facilities.
Guangzhou Heda Shelves: Your Trusted OEM/ODM Manufacturing Partner
Established in 2001, Guangzhou Heda Shelves Co., Ltd. operates an advanced 30,000-square-meter manufacturing plant in Guangdong, China, staffed by more than 300 experienced engineers, CNC tooling specialists, and skilled assembly operators. We export warehouse storage and mobile racking solutions across Australia, New Zealand, Europe, Southeast Asia, the Middle East, and the Americas.
Full Traceability: 10-Step Heavy Racking Production Workflow
Our automated production lines deliver structural accuracy across every millimeter of column punching, beam roll-forming, and robotic welding.
Spectrometric and tensile verification of certified Q235B/Q355 high-strength steel coils.
CNC uncoiling and laser-guided longitudinal slitting to exact section strip widths.
High-speed multi-stage hydraulic stamping presses punching 50mm / 75mm teardrop & diamond hole patterns.
Continuous 24-station roll-forming lines shaping omega uprights and step beam channels.
Automated robotic arm CO2 shielded arc welding of 3-to-5 tooth beam connectors and baseplates.
Mechanical shot blasting and deburring to eliminate micro-burrs and surface impurities.
Multi-tank automated immersion for degreasing, ultrasonic water rinsing, and anti-corrosive phosphating.
Swiss Gema powder coating spray booths applying 60–100μm durable polyester-epoxy film.
180°C to 200°C baking ovens ensuring thorough resin cross-linking, hardness, and scratch resistance.
Dimension verification, batch load testing, bundle strapping, and steel-stillage container loading.
Procurement & Technical Frequently Asked Questions (FAQ)
Essential guidance for project engineers, warehouse directors, and supply chain managers assessing movable and high-density racking installations.
What slab structural requirements and floor tolerances are needed for movable pallet racking? +
Movable pallet racking concentrates substantial live and dead loads across wheel tracks rather than distributing them over numerous baseplates. The concrete floor slab must accommodate point loads typically ranging from 40 kN to over 150 kN per wheel depending on system height and number of storage tiers.
Floor flatness is governed by international standards such as DIN 18202 or EN 15620. In-floor rails can be installed via three common methods: cast-in during the initial concrete slab pour, saw-cut into existing slabs, or laid above slabs within a secondary topping screed. Our engineering department provides complete track-recess drawings, anchor bolt specifications, and rebar reinforcement recommendations to share with your civil structural engineer.
Can HEDA custom-engineer racking to meet AS 4084 (Australia) and NZS 1170.5 (New Zealand)? +
Yes. We routinely design and export racking tailored to Australian Standard AS 4084:2023 (Steel Storage Racking) and New Zealand seismic guidelines. We verify frame stability against limit-state design principles, compute elastic buckling limits, and supply complete beam section property tables, connection test curves, and baseplate load calculations.
For New Zealand sites located in high seismic hazard zones (e.g., Wellington, Christchurch), we incorporate reinforced frame bracing, enlarged structural baseplates, heavy chemical undercut anchors, and heavy-duty row connectors to accommodate seismic ductility requirements.
What safety protocols prevent mobile carriages from closing on personnel or equipment? +
Every motorized mobile racking system uses redundant, multi-layered safety hardware meeting European CE Machinery Directives (EN ISO 13849-1). Safety systems include:
- Optical Light Curtains: Positioned at the entry face of each movable aisle, instantly cutting power to carriage drive motors if a forklift or worker breaches the aisle boundary while in motion.
- Infrared Optical Distance Scanners: Installed along the lower carriage sides to detect debris, stray pallets, or dropped tools on the guide tracks.
- Mechanical Kick Plates / Trip Bars: Full-length bottom sensors along both sides of every mobile carriage that immediately trigger an emergency stop upon contact.
- Manual Emergency Stop Consoles: Mounted on each carriage end column and on remote wall panels.
What typical lead times apply from design approval to container arrival? +
Standard fabrication runs between 20 and 30 working days following final sign-off of CAD layout drawings and load specifications. Shipping transit times vary by destination port:
- Australia / New Zealand: 14 to 24 days sea freight (Sydney, Melbourne, Brisbane, Fremantle, Auckland).
- Southeast Asia: 7 to 12 days (Singapore, Port Klang, Bangkok, Manila).
- Middle East: 18 to 26 days (Jebel Ali, Dammam, Jeddah).
- Europe & North America: 25 to 38 days (Rotterdam, Hamburg, Los Angeles, Savannah).
We supply advance bills of lading, detailed packing manifests, component itemization lists, and Form A / ChAFTA certificates of origin to support expedited customs clearance.
How does HEDA handle OEM branding and distributor private labeling? +
As an OEM/ODM manufacturer, we support storage integration specialists, material handling equipment dealerships, and regional racking brands worldwide. Our services include customized beam connector punch patterns, branded load rating plaques, unique RAL color electrostatic powder coatings, and custom-printed shipping carton labels matching your brand identity.
Request Your Custom Warehouse Layout & Engineering Quote
Send our engineering team your warehouse dimensions, clear height under sprinklers, pallet specifications, and target storage capacity. We typically return a detailed 3D CAD proposal and factory-direct price quotation within 24 hours.