Featured Industrial Warehouse Shelving & Racking Systems
Engineered from cold-rolled Q235B and high-yield Q355B structural steel, our load-tested racking series accommodates heavy mechanical tooling, high-velocity distribution pallets, and multi-tier picking facilities.
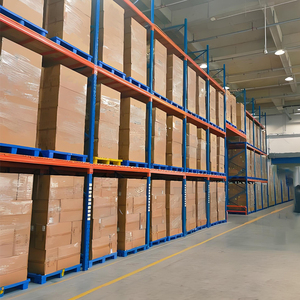
Long Span Heavy Duty Pallet Rack 1000kg–4000kg Capacity
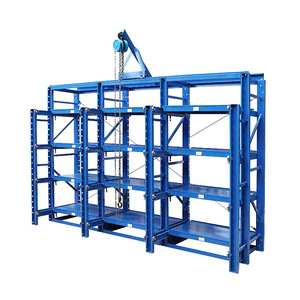
Fully Open Intelligent Mold Rack with Pull-Out System
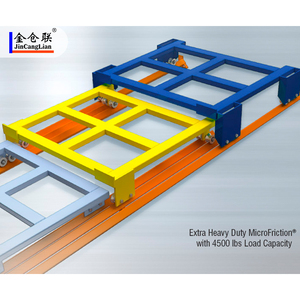
Push-Back Racking with 2~5 Movable Nested Carts
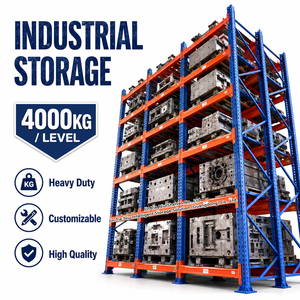
4000KG Heavy Duty Pallet Rack System Adjustable Beam
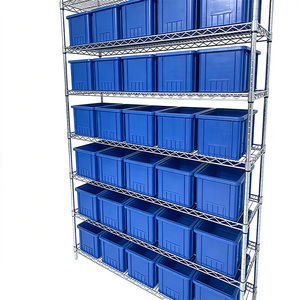
High Quality 7 Layers 250kg Factory Metal Storage Shelving
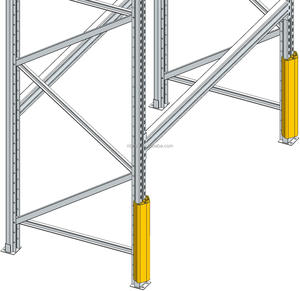
Flexible Upright Column Protector Anti-Collision Shield
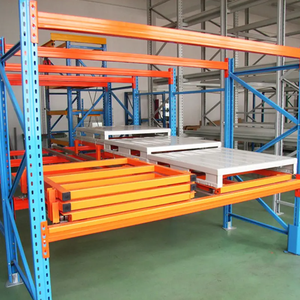
Push Back Pallet Rack with Heavy Duty Roller Tracks
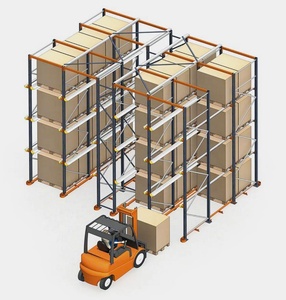
High-Density Q235 Drive-In Deep Lane Storage Racking
Engineering Integrity of Heavy Industrial Shelving Systems
Modern distribution logistics demands structural warehouse storage frameworks engineered well past baseline static loads. At Guangzhou Heda Shelves Co., Ltd. (HEDA Shelves), our OEM and ODM manufacturing pipelines strictly adhere to AS 4084:2023 (Steel Storage Racking), EN 15512, and RMI (Rack Manufacturers Institute) guidelines. Every pallet rack upright profile, interlocking step beam, and cantilever arm undergoes sophisticated Finite Element Analysis (FEA) to eliminate shear failure points and mitigate live impact vulnerabilities in high-throughput fulfillment environments.
The structural efficacy of industrial metal shelving rests upon the chemistry and tensile resilience of its coil feedstock. While low-grade commercial shelving relies on uncertified hot-rolled strips prone to micro-fissures during cold profiling, our facility exclusively forms profiles from certified Q235B and high-yield Q355B cold-rolled structural steel coils. Cold-roll continuous profiling optimizes the metallurgical grain boundary distribution across punch perforations, ensuring our 50mm and 75mm teardrop and diamond upright patterns maintain cross-sectional moment capacity under significant seismic and dynamic torsional forces.
| Structural Parameter | Light & Medium Longspan | Selective Heavy Pallet Racking | High-Density Dynamic Systems |
|---|---|---|---|
| Steel Formulation | Cold-Rolled Carbon Q235B | Certified Q235B / Q355B High-Yield | Structural High-Tensile Q355B |
| Nominal Yield Strength (MPa) | ≥ 235 MPa | ≥ 235 – 355 MPa | ≥ 355 MPa (Minimum) |
| Maximum Deflection Ratio | L / 250 under uniform load | L / 200 under rated pallet load | L / 300 under dynamic transit |
| Upright Profile Geometry | C-Section Omega Open Punch | Multifold Omega Closed/Perforated | Reinforced Box Rib Structural Column |
| Surface Pre-Treatment | Pickling & Zirconium Phosphating | 9-Stage Continuous Immersion | Electrostatic Zinc Rich Undercoat |
| Coating Thickness & Standard | 60–80 µm Electrostatic Powder | 70–90 µm TGIC Polyester Powder | Hot-Dip Galvanized ≥ 85 µm (Outdoor/Chill) |
| Seismic Verification Standard | Static Building Code Equivalent | AS 4084 / NZS 1170.5 Ductility | FEMA 460 / Dynamic Spectrum Analysis |
Beyond structural steel grades, safety margins are deeply influenced by connection mechanics. Our proprietary 3-claw and 4-claw cold-stamped beam end connectors feature high-precision safety locking pins engineered to withstand an upward dislodgement shear force exceeding 5.0 kN. This prevents catastrophic beam detachment when forklifts operate at maximum reach clearance inside narrow aisle (VNA) corridors.
10-Stage Precision Industrial Racking Production Process
Operating inside an automated 30,000 m² Guangzhou production facility, our comprehensive in-house fabrication loop guarantees total metallurgical traceability, zero component substitution, and consistent international compliance.
Coil Spectrometry
Optical emission chemical assay to verify tensile, carbon & silicon levels.
CNC Slitting & Cutting
High-tolerance uncoiling and laser edge trimming to ±0.2mm precision.
Automated Punching
Continuous hydraulic stamping of precision 50mm/75mm upright pitch matrices.
Cold Profile Rolling
Multi-station progressive roll forming without micro-fracturing outer flanges.
High-Frequency Welding
Robotic multi-pass seam welding of box beams and heavy flange connectors.
Automated Polishing
Mechanical blast derusting and weld seam dressing to eliminate surface burs.
Chemical Pre-Treatment
9-stage ultrasonic degreasing, pickling, rinsing, and zirconium phosphating.
Powder Coating Line
Automated Swiss Gema electrostatic spray booth with thermosetting polymers.
High-Temp Curing
Gas-fired 200°C tunnel curing achieving 2H scratch hardness and salt-spray defense.
Stillage Packing & QC
Deflection load validation, ISPM-15 wooden framing, or heavy steel pallet stillages.
Future Procurement Trends in Industrial Shelving & Racking
Global supply chain disruptions, soaring logistics square-meter costs, and warehouse automation mandates are reshaping how commercial facility operators procure bulk racking assets.
1. ASRS & Shuttle-Ready Upright Profiling
Procurement teams are shifting away from manual-only static bays. Modern selective and deep-lane racking must now feature laser-guided dimensional tolerances under ±1.0 mm per 10 meters of vertical climb. Our OEM factory produces high-precision rail interfaces and integrated guide-wire anchor brackets directly engineered for autonomous 4-way radio shuttles and automated guided vehicles (AGVs), future-proofing physical assets against upcoming robotic retrofits.
2. Advanced Seismic & Dynamic Ductility Mandates
Following updated seismic mapping standards in Australasia (NZS 1170.5, AS 4084:2023) and North America (FEMA), racking procurements mandate verified energy-dissipation baseplates and heavy diagonal portal bracing. HEDA Shelves engineers integrate bespoke ductile base shoes, chemical anchor embedment calculations, and high-tensile anchor configurations that allow dynamic structural flexing under seismic excitation without sudden catastrophic column buckling.
3. Low-VOC Finishes & Circular Supply Traceability
ESG compliance is fast becoming a hard pre-qualification standard for Tier-1 multi-national 3PL contracts. Our finishing operations eliminate volatile organic solvents, utilizing 100% TGIC-free recyclable polyester powders cured via recuperative natural-gas baking chambers. Furthermore, complete mill test certificates (MTC) trace every steel consignment from certified state-owned blast furnaces directly to customer shipping containers.
How to Select the Optimal Warehouse Industrial Shelving System
Selecting warehouse racking is an engineering equation balancing cubic density, picking throughput, and stock rotation economics. A mismatch leads to chronic bottlenecks, fork-truck mast impacts, or severe structural underutilization:
1. Ultra-High SKU Diversity with 100% Selectivity: If your logistics model demands instant access to thousands of discrete product lines (such as wholesale hardware, automotive parts centers, or fast-fashion 3PLs), standard Selective Pallet Racking remains undisputed. Paired with counterbalanced or reach trucks, it yields rapid picking cycle times with low capital equipment overhead.
2. Uniform Goods with Cold-Chain Density: In temperature-controlled frozen and refrigerated warehouses where maintaining sub-zero air volume costs an operational premium, open aisles represent waste. Here, Drive-In Racking and Push-Back Racking compress footprints by 65% to 85%. Push-back systems utilizing precision gravity-sloped nested carts allow multi-pallet deep storage per level while eliminating the risk of forklift operators driving deep inside dark upright tunnels.
3. Heavy Industrial Dies and Tooling Storage: Storing injection molds, metal stamping dies, and machine parts on conventional wood or wire decking invites deck collapse. Our specialized Intelligent Pull-Out Mold Racking incorporates 100% extraction drawer slides rated for 2,000 kg per shelf, equipped with mechanical dead-lock safeties and bridge crane compatibility, allowing overhead sling lifting straight to injection machines.
Frequently Asked Questions for Warehouse Racking Buyers
Direct, engineer-verified answers to critical structural, logistics, compliance, and custom manufacturing inquiries.
?Can you engineer custom punching and OEM profile compatibility?
Yes. As an OEM and ODM primary manufacturer, HEDA Shelves can machine custom roll-forming tooling to match proprietary upright hole profiles (such as 50mm metric, 75mm British Standard, 76.2mm teardrop, or Dexion-style diamond punch matrices). If you need to integrate new bays seamlessly into an existing warehouse installation, send our engineering department a cross-section sample or CAD section drawing.
?How do your racking structures achieve AS 4084:2023 compliance?
Our engineering team performs limit-state calculations analyzing frame instability, beam deflection ratios ($L/200$), and torsional-flexural buckling in accord with AS 4084 guidelines. We supply comprehensive structural data packs, including steel mill tensile test certificates, section modulus properties ($Z_x, Z_y$), and certified load application charts to enable your local Australian or New Zealand chartered professional engineer (CPEng) to issue site compliance sign-off.
?How are sea container shipments prepared to prevent moisture and transit rust?
Ocean container shipments crossing humid equatorial routes risk condensate "container rain." We prevent corrosion by applying dry electrostatic pre-cure coats, industrial shrink wrapping around upright bundles, silica gel desiccant packs within air cavities, and rigid steel strap binding on heavy steel stillages. Heavy-duty timber dunnage is strictly heat-treated and heat-stamped in compliance with international ISPM-15 biosecurity protocols.
?What warehouse slab specifications are required for heavy-duty pallet racks?
For standard 3,000–4,000 kg beam level configurations spanning up to 8–10 meters in frame height, the industrial concrete floor slab typically requires a minimum compressive strength of 25 to 30 MPa with a minimum slab thickness of 150mm to 200mm. We engineer oversized steel column baseplates ($150 \times 150 \times 6\text{mm}$ to $200 \times 200 \times 12\text{mm}$) to disperse concentrated foot point loads well below your concrete punch-shear threshold.
?What is the lead time for full container load (FCL) custom OEM projects?
Standard OEM fabrication cycles for full 20GP or 40HQ container orders range between 15 to 25 business days from final 3D CAD layout approval. Transit times vary from 12 to 24 days to Oceania ports (Sydney, Melbourne, Auckland), 25 to 35 days to North America (Long Beach, Vancouver), and 28 to 38 days to Northern Europe (Rotterdam, Hamburg). Turnkey tracking documentation is dispatched concurrently.
?Can your racking components be hot-dip galvanized for corrosive settings?
Yes. While our multi-stage electrostatic thermoset powder coat is ideal for standard ambient distribution centers and clean packaging plants, we supply complete Hot-Dip Galvanized (HDG) frames, beams, and pallet supports for open-air timber yards, coastal salt-laden environments, agricultural chemical warehouses, and severe condensation sub-zero blast freezers to ISO 1461 standards.