Featured Racking Systems & Industrial Equipment
Factory-direct OEM and ODM production lines engineered for harsh industrial environments, cold storage distribution centers, and multi-tier logistics hubs.
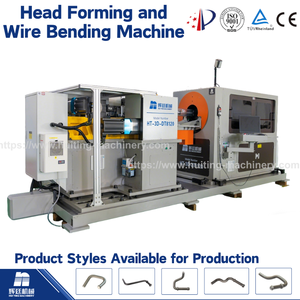
Huiting High Precision 8-Axis Automatic CNC Motor Integrated Head Forming Wire Bending Machine Automotive Stainless Steel
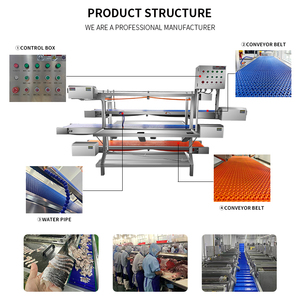
High-capacity Production Line Seafood Cooling Tunnel Fish Killing Workbench Vegetable Fruits Candies Flour Seafood Grain Product
Light Gauge Steel Frame 40Ft Container Expandable House 4 Bedroom Luxury Tiny Waterproof Turnkey Prefab Home Cabin
K2 Free Shipping Electric Forklift 2.5Ton CE ISO EPA Rough Terrain Sturdy Forklift Cheap Price Powerful
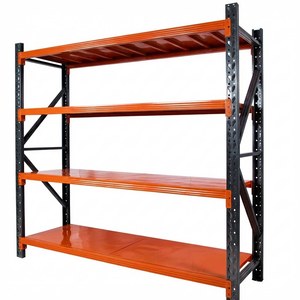
Durable Cold Rolled Steel Heavy Duty Multi-Layer Pallet Rack Warehouse Storage Solution High Loading Capacity Epoxy Racking
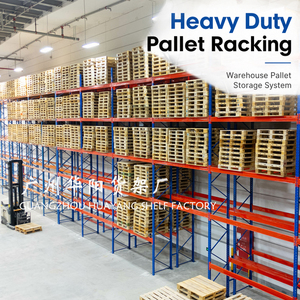
3000KG Per Level Heavy Duty Pallet Rack Industrial Warehouse Storage Steel Shelving Adjustable Pallet Racking System
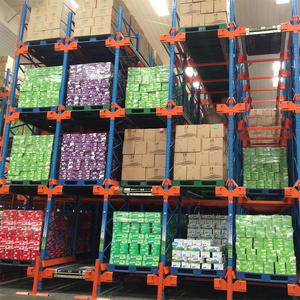
China Factory Direct Heavy Duty Steel Shelving Warehouse Automatic Two-Way Radio Shuttle Rack System Pallet Racking for Storage
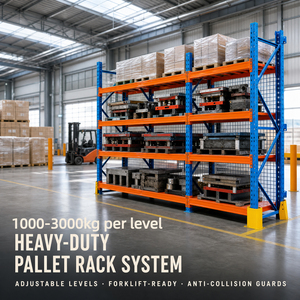
Heavy Duty Pallet Racking Adjustable Heavy Load Capacity 2000kg/3000kg Cold Rolled Steel Powder Coated 1 Year Warranty
Erecting Mechanics, Load Dissipation & Engineering Tolerances
Modern pallet racking systems are not static steel frames; they are dynamic, engineered spatial structures governed by strict continuum mechanics, torsion-resistance profiles, and seismic yield criteria.
Continuous Omega Upright Profiling
Cold roll-formed with up to 13 mechanical bending facets. This multi-rib geometry distributes axial forces across the column cross-section, drastically mitigating local torsional flexural buckling under extreme static vertical loads.
Moment-Resistant Beam End Connectors
Features stamped 3-claw and 4-claw high-tensile connection plates welded seamlessly to interlocking twin-C box beams. Integrated spring-loaded safety locking pins prevent vertical accidental dislodgement caused by high-reach mast snagging.
Deflection Tolerance Ratios (L/200)
Load-bearing step and box beams are pre-cambered and calibrated to an allowable vertical flexure limit of strictly less than L/200 (Span Length / 200) under full design working loads, safeguarding automated shuttle sensors and forklift clearances.
Seismic Dissipation & Dynamic Base Anchorage Engineering
Metallurgical Integrity: Q235B vs Q355B Cold-Rolled Substrates
Material performance is the core foundation of operational safety. Our manufacturing facility leverages primary coil mill partnerships to guarantee uniform grain structure and strict chemical composition.
| Steel Grade Standard | Yield Strength (ReH / MPa) | Tensile Strength (Rm / MPa) | Elongation at Break (A50 %) | Primary Racking Component Application |
|---|---|---|---|---|
| Q235B (ASTM A36 Equiv.) | ≥ 235 MPa | 370 – 500 MPa | ≥ 26% | Standard pallet beams, horizontal frame braces, diagonal bracing struts, wire mesh decking. |
| Q355B (ASTM A572 Gr. 50 Equiv.) | ≥ 355 MPa | 470 – 630 MPa | ≥ 22% | High-bay upright columns (>10m height), heavy dynamic shuttle rails, cantilever load arms. |
| Hot-Dip Galvanized Coil (DX51D+Z) | ≥ 260 MPa | 360 – 510 MPa | ≥ 24% | Outdoor cantilever racks, agricultural fertilizer depots, marine coastal port cold stores. |
| High-Tensile Cold Strip (SPCC/ST12) | ≥ 210 MPa | 270 – 410 MPa | ≥ 38% | Precision-formed beam connector teeth, spring safety locks, roll-formed drop-in shelf panels. |
Corrosion Prevention & Automated Electrostatic Powder Coating Line
Warehouse Storage Procurement Trends (2025–2030)
Global supply chain instability, escalating industrial square-meter lease rates, and accelerating warehouse automation are fundamentally reshaping how industrial racking systems are specified, procured, and deployed.
1. Vertical Densification & High-Bay AS/RS Transition
With prime logistics industrial real estate rents surging across major logistics corridors (e.g., Sydney, Melbourne, Auckland, Los Angeles, Rotterdam), greenfield warehousing is rapidly pivoting from standard 7.5m clear heights to 14m–24m ultra-dense vertical architectures. Erecting pallet racking is increasingly required to function simultaneously as the core rack-supported building superstructure (clad-rack systems), directly integrating automated stacker cranes, high-speed rail systems, and ceiling sprinkler mains.
2. Automation-Ready Hybrid Systems & Radio Shuttle Lanes
Forklift-intensive selective layouts are giving way to semi-automated 2-way and 4-way deep-lane Radio Shuttle racking. In cold storage distribution (-25°C) and beverage processing hubs, deep-lane shuttle racks allow operators to consolidate pallet positions by up to 80% while eliminating forklift transit inside storage bays, minimizing structural column impact damage and reducing operational labor expenditure.
3. Factory-Direct OEM/ODM Disintermediation
Enterprise end-users, 3PL contractors, and regional racking installation contractors are bypassing intermediary trading brokers. By executing direct mill-to-port OEM contracts with certified manufacturers like Guangzhou Heda Shelves Co., Ltd., procurement teams achieve 25%–38% cost efficiency, obtain uncompromised mill test certificates (MTC), and gain customized slotting dimensions adapted specifically for non-standard local pallets (such as Australian 1165mm x 1165mm pallets or European 1200mm x 800mm formats).
4. Carbon Footprint Accountability & Circular Lifecycle
ESG compliance protocols are enforcing lifecycle traceability across supply chain hardware. High-tensile cold-formed steel sections maximize yield load per kilogram of consumed metal, reducing embodied carbon during smelting and freight. In addition, boltless erection mechanisms facilitate non-destructive disassembly, secondary site re-erection, and full material recyclability without structural degradation.
Comparative Engineering Matrix: Pallet Racking Classifications
Selecting the optimal structural geometry requires evaluating warehouse volumetric efficiency against stock throughput velocity, SKU diversity, and mechanical handling equipment (MHE) constraints.
| Racking Architecture | Floor Space Utilization | SKU Selectivity Ratio | Inventory Rotation Profile | Recommended Operating Sector |
|---|---|---|---|---|
| Selective Pallet Racking | 40% – 50% (Standard Aisle) | 100% Direct Access | FIFO (First-In, First-Out) | Multi-SKU 3PL warehouses, e-commerce retail distribution, pharmaceutical depots. |
| Double Deep Racking | 55% – 65% (Deep Storage) | 50% Immediate Access | LIFO (Last-In, First-Out) | Bulk dry goods, paper packaging reserves, medium-turnover reserve pallet holding. |
| Drive-In / Drive-Through | 70% – 80% (Dense Block) | Low Access (Single Lane) | LIFO (Drive-In) / FIFO (Drive-Thru) | Cold storage chillers/freezers, raw ingredient manufacturing, low-SKU seasonal holding. |
| Radio Shuttle Automation | 80% – 90% (Ultra-Dense) | Controlled Deep-Lane | Flexible FIFO & LIFO Programmed | High-throughput beverage plants, meat & seafood processing, central fast-moving distribution. |
| Gravity Pallet Flow | 75% – 85% (Dynamic Roller) | High (Lane-End Picking) | Strict Automatic FIFO | Perishable foods, dairy produce, short shelf-life chemicals, fast buffer picking lines. |
| Cantilever Racking Systems | Variable Linear Area | 100% Unobstructed Front | Free Selective Loading | Timber yards, aluminum extrusions, steel tubing, PVC pipe and structural rebar handling. |
Guangzhou Heda Shelves Co., Ltd.: Direct Manufacturing Authority
Since 2001, our facility has served as an OEM/ODM manufacturing engine for global distributors, structural contractors, and commercial developers across Australia, New Zealand, Europe, and the Americas.
Independent Third-Party Certification
Our systems possess accredited CE Certification (No. 2435-CPR-8605159) and rigorous ISO 9001:2015 Quality Management System Certification (No. 18624Q00169R0M), ensuring verified compliance that withstands civil engineering sign-offs.
Full 3D CAD & Structural Calculation Packs
We provide comprehensive BIM Revit files, 3D DWG schematics, beam cross-sectional inertia calculations, and safe working load (SWL) load plaques customized for facility permit approvals before cutting steel.
Export Containerization & Biosecurity
Shipments comply with strict import bio-security regimens (Australian DAFF and New Zealand MPI). Components are secured in heavy custom steel stillages or fumigated timber under ISPM-15, eliminating port inspection delays.
Our Standard 10-Step End-to-End Production Workflow
Raw Material Inspection
01Spectrometric chemistry & mechanical tensile verification on all incoming prime steel master coils.
Precision Slitting & Cutting
02High-speed rotary longitudinal slitting to exact strip tolerance widths within ±0.1mm tolerance.
CNC Column Punching
03Automated multi-stage continuous punch dies punching teardrop or diamond pitch holes at exact 50mm/75mm centers.
Cold Bending Forming
04Progressive multi-pass cold roll-forming lines creating rigid omega uprights and interlocking box beam sections.
Profile Calibration
05Secondary roll-forming checks to guarantee zero column camber, sweep, or longitudinal twisting along full lengths.
Robotic Welded Joinery
06Panasonic robotic CO2 gas-shielded automated welding cells attaching connector claws to beam tubes without porosity.
Surface Pre-Treatment
077-stage immersion line: degreasing, pickling, rinsing, and chemical zinc-phosphating conversion bath.
Electrostatic Powder Spray
08Gema automated spray guns applying 60–90 μm uniform thermoset epoxy-polyester coatings.
High-Temp Polymer Curing
09200°C tunnel curing ensuring resilient chemical bonding, high impact elasticity, and scratch resistance.
Final QC & Stillage Pack
10Coating adhesion checks, dimensional audits, steel bundling, barcode tagging, and export container loading.
Frequently Asked Questions: B2B Engineering & Export Verification
Key technical answers for procurement directors, structural engineers, and warehouse logistics managers considering offshore direct-mill manufacturing.
1. How does your OEM erecting pallet racking comply with Australian Standard AS 4084-2023 and European FEM 10.2.02?
2. What structural adaptations are implemented for cold storage facilities operating down to -30°C?
3. How does Guangzhou Heda Shelves verify load capacity limits before exporting containers?
4. What international customs documentation and certificates of origin do you provide?
5. Can you manufacture custom slotted uprights and beam connectors to retrofit existing competitor racking?
6. How do you prevent packaging damage and ocean freight condensation during maritime transit?
7. What is the typical lead time from CAD drawing sign-off to port arrival?
8. What on-site installation support and layout guidance do you offer offshore contractors?
Request Your Custom 3D CAD Racking Layout & Engineering Quote
Supply our structural engineers with your clear ceiling heights, building slab specifications, pallet loading limits, and forklift models. Within 24 hours, our engineering department will formulate a complete CAD elevation design, slotting density optimization matrix, and direct factory-mill cost breakdown.