Industrial Racking & High-Density Systems Matrix
Engineered for structural durability and extreme vertical density. Explore our core OEM/ODM production lines certified for logistics hubs, distribution centres, cold-storage, and high-cube facilities.
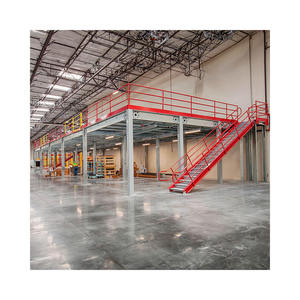
Multi-Level Mezzanine Racking Platform System
- Load: 300 - 1,000 kg/m² UDL
- Integrated staircases & safety gates
- Custom beam profiles & cold-rolled deck
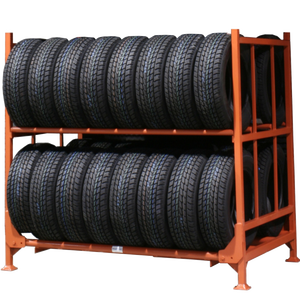
Heavy Duty Foldable Steel Stacking Storage Rack
- 4-way forklift pocket entry
- 85% return-shipping space saving
- Anti-corrosive powder/galvanized
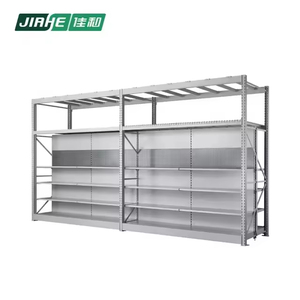
Heavy Duty Hypermarket Industrial Shelving
- Hybrid retail & bulk top pallet bays
- 500 - 1,500 kg layer capacity
- 50mm pitch adjustable beam levels
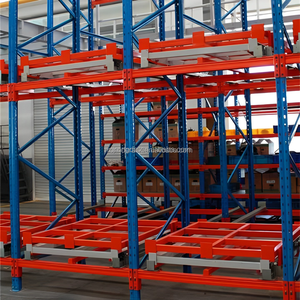
Precision Push Back Pallet Racking System
- 2 to 6 deep pallet nesting carts
- Heavy duty steel track bearings
- Single aisle load and extraction
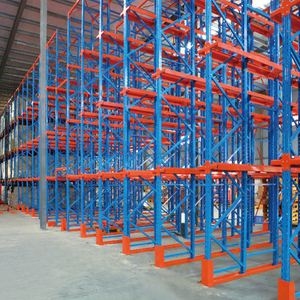
High-Cube Drive-In Continuous Pallet Racks
- Up to 85% cubic space utilization
- One-piece structural cantilever arms
- Ideal for cold storage & batch SKUs
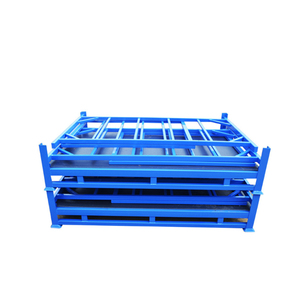
Heavy Plate Stacking Cage & Tire Racks
- High yield strength Q235B cold rolled
- Interlocking cup feet for stacking
- Demountable / foldable post system
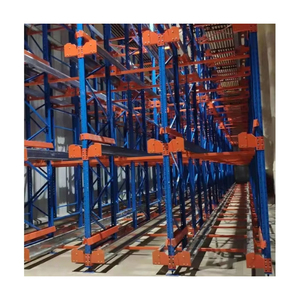
High-Efficiency Radio Pallet Shuttle System
- Autonomous radio shuttle carrier
- Zero forklift aisle transit risk
- FIFO and LIFO logical routing
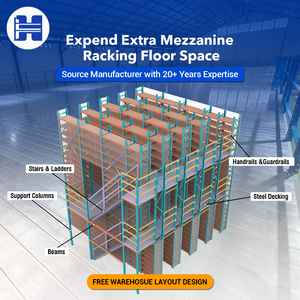
Heavy Duty Rack-Supported Mezzanine Floor
- Uprights function as structural pillars
- Multi-tier order fulfillment floors
- Heavy gauge perforated steel planks
1. Engineering Fundamentals of Industrial High Bay Racking Systems
In modern supply chain architecture, modern industrial warehouses demand optimization of the vertical envelope. The transition from conventional low-profile floor storage to engineered high bay racking systems—ranging from 12 meters to over 40 meters in rack-supported clad buildings—demands stringent mechanical tolerances, finite element analysis (FEA), and advanced metallurgical consistency. OEM and ODM manufacturing of high bay racking is not merely a steel transformation process; it is structural civil engineering under dynamic and seismic stress conditions.
High bay systems, particularly when configured for Very Narrow Aisle (VNA) wire-guided turret trucks or fully automated Automated Storage and Retrieval Systems (ASRS), operate under tight deflection criteria. Where standard selective racking accommodates beam deflection allowances of $L/200$, automated high bay systems require stiffening to $L/300$ or $L/400$ to prevent optical obstruction of robotic sensors and automated crane end-effectors. Every millimeter of horizontal column sway or base-plate displacement translates to systemic throughput failure at heights above 15 meters.
2. Future Procurement & Technological Evolution Trends (2025–2035)
Procurement directors and supply chain engineers evaluating high bay racking systems face rapid shifts driven by automation, land scarcity, and carbon accounting regulations. In global logistics hubs across Australia, North America, and Europe, high bay infrastructure is evolving from passive steel shelving into dynamic, intelligent building envelopes.
3. Industrial Technical Comparison & Engineering Selection Matrix
Selecting the appropriate high bay racking architecture requires balancing floor space footprint, operating clear height, inventory velocity (FIFO vs LIFO), SKU selectivity, and automated material handling equipment (MHE) integration. The following matrix illustrates the performance envelope of core systems produced in our certified manufacturing facility.
| Storage System Type | Operating Height | Storage Density | Selectivity | MHE Compatibility | Standard Load/Pallet | Compliance Standards |
|---|---|---|---|---|---|---|
| Automated High-Bay (ASRS) | Up to 45.0 Meters | Maximum (>90%) | 100% Direct | Stacker Cranes / Shuttles | 500 – 2,000 kg | FEM 9.831 / EN 15620 / AS 4084 |
| Very Narrow Aisle (VNA) | Up to 18.0 Meters | Very High (75%) | 100% Direct | Man-Up / Man-Down VNA | 800 – 1,800 kg | AS 4084 / ANSI-RMI MH16.1 |
| Radio Shuttle System | Up to 24.0 Meters | Ultra High (85%) | Batch / Deep Lane | Autonomous Shuttle + Reach | 500 – 1,500 kg | CE Machinery Directive / ISO 9001 |
| Drive-In / Drive-Through | Up to 12.0 Meters | High (70%) | LIFO / Last-In | Counterbalance / Reach | 1,000 – 1,500 kg | EN 15512 / ISO 9001:2015 |
| Push Back Racking | Up to 10.0 Meters | Moderate-High | Lane Dependent | Standard Reach Truck | 1,000 – 1,400 kg | AS 4084 / RMI Standards |
| Rack-Supported Mezzanine | Up to 16.0 Meters (Multi-tier) | Maximum Cube | Tier Specific | Order Pickers / Conveyors | 300 – 1,000 kg/m² | EN 1090-1 / CE / AS 4084 |
4. Enterprise Manufacturing Advantages: Guangzhou Heda Shelves Co., Ltd.
Established in 2001, Guangzhou Heda Shelves Co., Ltd. has grown into an international engineering and fabrication powerhouse for industrial storage solutions. Spanning an integrated 30,000 square meter intelligent manufacturing facility supported by over 300 technical engineers and precision fabricators, the company operates with an in-house capacity of 30,000 metric tons per month.
Certified Compliance Authority
Fully accredited under CE Certification No. 2435-CPR-8605159 and ISO 9001:2015 Quality Management System No. 18624Q00169R0M. Systems are engineered with reference to AS 4084, FEM, and ANSI/RMI criteria, backed by verifiable calculations for local structural engineers.
End-to-End Roll-Forming Production
Ten automated manufacturing stages: from uncoiling high-strength steel coils, CNC punching, precision cold-bending, continuous roll-profiling, robotic welding, to an in-line 10-stage pickling, phosphating, and electrostatic powder coating finishing line.
Export Logistics & Biosecurity Security
Equipped for ocean logistics serving major global terminals (Sydney, Melbourne, Auckland, Rotterdam, Long Beach). All timber components comply with ISPM-15 heat-treatment stamping, preventing DAFF/MPI port quarantine delays.
5. Strategic Procurement & Engineering FAQ for Buyers
How does HEDA ensure AS 4084 and NZS 1170.5 compliance for Australian and New Zealand sites?
What floor slab tolerances are required for high-bay racking systems exceeding 12 meters?
What surface protection systems are provided for cold-storage and coastal environments?
What are the lead times for custom OEM/ODM high bay production and sea-freight dispatch?
Can you manufacture private-label racking components compatible with existing global profiles?
How does HEDA prevent biosecurity and timber packaging delays during customs border control?
Request a Structural Engineering Consultation & 3D Layout
Provide your building CAD drawings, ceiling clear heights, seismic zone parameters, and pallet profiles. Our engineering office delivers an optimized layout, capacity calculation, and detailed factory-direct quotation within 24–48 hours.