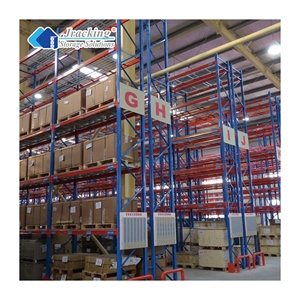
 Heavy Duty Steel
Jracking EU Standard Pallet Racking
Certified structural framework with optimized cold-rolled profiles engineered to accommodate integrated upright crash protection barriers.
Product DetailsExplore heavy-duty column buffers, elastomeric dampeners, barrier frameworks, and certified systems engineered to minimize warehouse risk and safeguard inventory throughput.
Heavy Duty Steel
Certified structural framework with optimized cold-rolled profiles engineered to accommodate integrated upright crash protection barriers.
Product Details Floor Anchored
Reinforced steel corner casing distributing ground shear stress away from vulnerable uprights during aggressive counterbalanced forklift turning.
Product Details Impact Absorbing
Engineered elastomeric polymer construction dampens bottom rack beam shock, minimizing direct structural abrasion and edge racking damage.
Product Details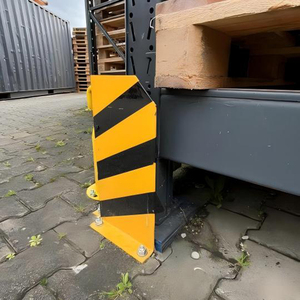 Direct Defense
High-visibility safety yellow powder-coated barrier featuring floor anchors engineered to withstand multi-directional industrial reach truck hits.
Product Details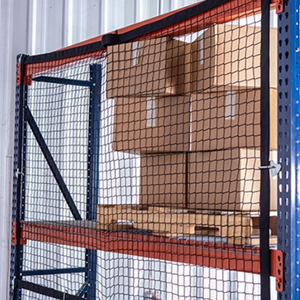 Fall Containment
Industrial nylon rope mesh engineered to prevent push-through warehouse incidents and catch unstable unit loads in high-bay pick tunnels.
Product Details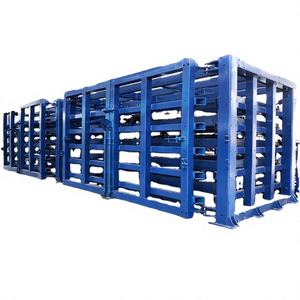 Integrated Tech
Dynamic high-density electric system fitted with automated safety shut-off sensors, optical laser guards, and electrostatic discharge safeguarding.
Product Details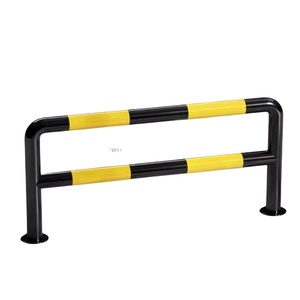 Aisle Protection
Continuous reinforced wrap-around barrier system defending entire row ends from dynamic transverse turning impacts by material handlers.
Product Details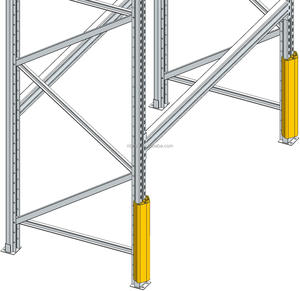 Snap-On Polymer
TUV and SGS tested shock-dissipating polymer shield gripping posts seamlessly, dispersing point-load forces without cracking concrete slabs.
Product DetailsIn modern industrial intralogistics, pallet rack uprights represent critical load-bearing structural columns holding thousands of kilograms overhead. When a loaded forklift strikes an unprotected upright at even 3 km/h, the resultant kinetic impulse easily exceeds the local yield strength of standard cold-formed structural steel profiles. Without protective buffers, this local buckling precipitates catastrophic progressive collapse across an entire storage bay.
Modern pallet rack protection manufacturers specialize in decoupling the barrier system from the column itself. By installing floor-anchored structural shields or snap-on viscoelastic polymer dampeners, forces from material handling equipment (MHE) are diverted into concrete subfloors or elastic matrix deformation rather than the rack profile.
| Protection Technology | Impact Absorption Mechanism | Subfloor Stress Index | Maintenance & Lifecycle | Primary Application Zone |
|---|---|---|---|---|
| Structural Steel Casing (Floor-Bolted) | Rigid physical deflection & ground shear diversion | High (risk of concrete anchor spalling) | Requires realignment or repainting after collision | Main perimeter transit aisles & tunnel crossovers |
| Viscoelastic Polymer (Snap-On) | Dynamic molecular elasticity & form memory recovery | Zero (zero contact with concrete floor) | Maintenance-free; snaps directly into place | Intermediate pick aisle columns & narrow aisles |
| Heavy Tubular End Barriers | Continuous structural beam cross-redirection | Evenly distributed dual-anchor pad dispersion | Heavy structural lifespan; modular replaceable rails | Row ends facing heavy forklift turning radiuses |
| Tensile Nylon Netting Modules | Progressive web elongation & dynamic containment | Zero (tied directly onto upright structural framing) | Periodic inspection for weave integrity & sag | High-bay backstops & pedestrian safety walkways |
Procurement teams often underestimate the cascading costs associated with rack damage. Replacing an upright frame is not merely an equipment cost—it demands unloading neighboring bays, hiring third-party structural certifiers, halting inventory operations, and risking workplace safety violations. Investing in a vetted pallet rack protection manufacturer cuts long-term MRO expenditure by over 73% across a facility's multi-year operational horizon.
As global supply chains expand and high-density automation increases warehouse operating velocity, rack protection has evolved from static painted accessories into engineered facility integrity systems. Enterprise buyers must plan for three major structural trends driving modern warehousing:
Modern supply operations increasingly favor specialized engineered polymers like HDPE and modified urethanes. These units deflect forklift forks on impact, dampening force through molecular shear and returning to their initial geometry without permanent dents or structural strain.
With Autonomous Mobile Robots operating alongside high-reach trucks, modern protection hardware features matte, non-glare, safety-yellow textures that integrate seamlessly with LiDAR scanners, eliminating ghost obstacle detections while preventing structural frame scuffs.
Next-generation floor-anchored steel guards incorporate elastomeric base bushings that dampen the kinetic snap-back of vehicle collisions, stopping micro-fractures in concrete slabs and eliminating loose anchor bolt heads around turn radiuses.
Direct technical answers addressing the real structural considerations engineering directors, safety auditors, and facility managers face when specifying warehouse rack guards.
Floor-bolted steel casings are essential at row ends, picking tunnels, and main drive aisles where high-tonnage counterbalanced trucks maneuver at speed. Snap-on polymer guards excel inside high-density narrow aisles where internal clearances are tight and direct floor drilling is restricted by slab rebar or heating pipes.
Both AS 4084 and EN 15635 dictate that upright protectors must stand independent of the rack column, be at least 400 mm in height, and absorb a non-directional kinetic impulse without transferring buckling loads into the upright post. All our specialized protections are certified to meet or exceed these thresholds.
Standard cold plastics fracture under cold-room impacts. For cold storage and freezer applications (-25°C to -30°C), we manufacture using ultra-high-density polymers formulated with specialized plasticizers or hot-dip galvanized cold-grade structural steels that resist low-temperature embrittlement.
Every shipment is packaged on dedicated steel cradles or ISPM-15 heat-treated certified timber. Complete packing manifests, material mill certificates, and preferential certificates of origin accompany shipments to prevent customs delays across Australia, New Zealand, Europe, and North America.
Since 2001, Guangzhou Heda Shelves Co., Ltd. has grown into an international manufacturing partner trusted across Australia, New Zealand, Europe, and the Pacific. We bridge the gap between heavy structural engineering and customized safety accessories.
Operating scalable, in-house roll forming, automated laser cutting, precision CNC stamping, and robotic welding lines delivering up to 30,000 tons of structural equipment every month.
All facilities and production lines operate under accredited ISO 9001:2015 Quality Management (No. 18624Q00169R0M) alongside verified CE Construction Certification (No. 2435-CPR-8605159).
Our in-house team of more than 300 technical engineers analyzes your warehouse layouts, turning facility floor plans into accurate 3D structural CAD blueprints within 24 hours.
Connect with our technical design engineers for full product specifications, AS 4084 load tables, and factory-direct project estimates.
Get Catalog