[email protected] Supplying Australia, New Zealand & the Pacific Islands
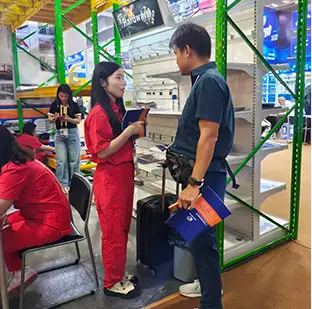
Safety Engineering Since 2001

Chemical Storage Racking System: Engineered Safety & Bunded Compliance

Factory-direct high-density heavy duty racking with certified spill containment, anti-corrosive finishes, and international AS 4084 / CE compliance.

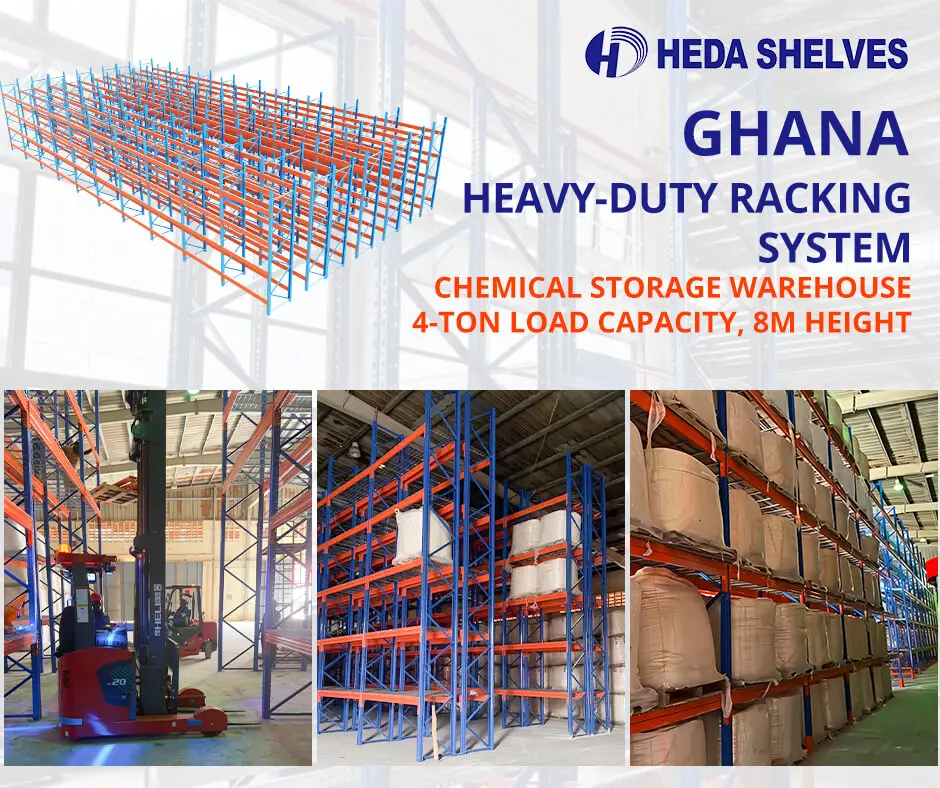
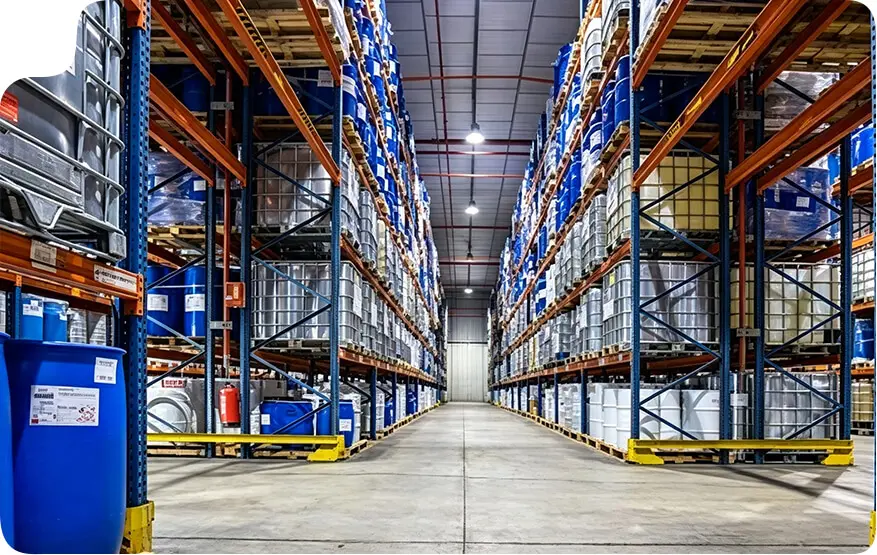
Chemical storage racking system for drums and IBC containers
Dangerous Goods Ready

Drum Cradles, Spill Trays & Galvanised Structural Profiles

Prevent hazardous soil and facility contamination with built-in liquid retention sumps and certified dynamic beam deflection limits.

Heavy duty steel racking manufactured by Guangzhou Heda Shelves Co., Ltd.
CE & ISO 9001:2015

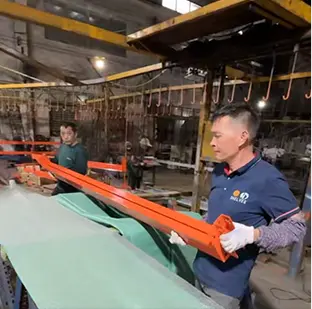
30,000 m² Production Facility. 30,000 Tons Monthly Capacity.

From precision steel slitting and robot welding to 10-step anti-corrosion coating, every batch meets stringent international audits.

  • DG Secondary BundingCertified leak containment catchments
  • Corrosion ProtectionHot-dip galvanised & thermoset epoxy
  • Point-Load EngineeringTailored for heavy IBC & 205L drum stacks
  • Global Regulatory ComplianceAS 4084, EN 15512 & NFPA 30 ready
Comprehensive Product Systems

Industrial Chemical Storage Racking System Recommendations

Chemical and hazardous goods storage presents severe physical and chemical challenges: heavy liquid densities, concentrated drum point loads, corrosive vapours, and mandatory containment legislation. Explore our field-tested racking configurations.

Request Custom Sump Sizing
Chemical storage selective pallet racking with bunded sumpsSelective Storage

Bunded Selective Pallet Racking

The global benchmark for multi-SKU chemical warehouses. Designed with integrated galvanised containment bunds beneath each bay to collect corrosive accidental spills instantly.

  • 100% SKU selectivity
  • Under-beam spill trays
  • AS 4084 / EN 15512
Get chemical layout & pricing
Horizontal drum cradles and IBC racking modulesDrums & IBCs

Heavy-Duty Drum & IBC Modules

Engineered for high concentrated loads of 1,000L IBC totes and 205L chemical steel drums. Features curved drum chocks, heavy cross-ties, and reinforced tubular support saddles.

  • 1,000–3,500 kg / level
  • No roll-off chocks
  • Dispensing spigots ready
Get chemical layout & pricing
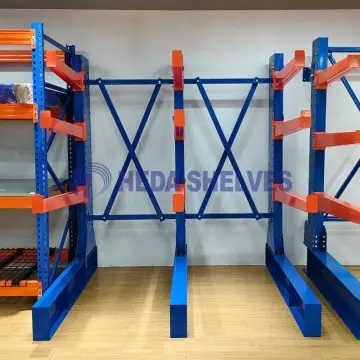
Galvanised cantilever racking for chemical cylindrical goodsCorrosive Yards

Hot-Dip Galvanised Outdoor Cantilever

Designed for chemical processing facilities, fertiliser distributors, and outdoor acid yards. Fully hot-dip galvanised according to ISO 1461 to resist extreme atmospheric oxidation.

  • ISO 1461 Galvanised
  • Cylinders & drums
  • Up to 3,000 kg / arm
Get chemical layout & pricing
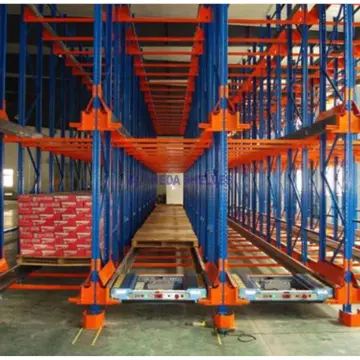
High density radio shuttle racking for bulk industrial chemicalsExplosion-Proof

ATEX-Ready Radio Shuttle Racking

Automated deep-lane high density storage for massive single-SKU chemical processing. Features isolated mechanical tracks and optional ATEX-rated components for Zone 2 safety zones.

  • Zero forklift rack impact
  • FIFO or LIFO operation
  • Anti-static roller guides
Get chemical layout & pricing
Narrow aisle chemical storage racking with guide railsVNA High Bay

Very Narrow Aisle (VNA) Chemical Racking

Maximises vertical storage cubage in specialised climate-controlled chemical facilities. Equipped with floor mechanical guidance rails or inductive wire guidance to protect uprights.

  • Clear heights up to 14m
  • Sprinkler flue spacing
  • Upright corner armour
Get chemical layout & pricing
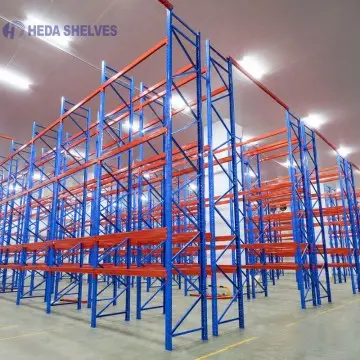
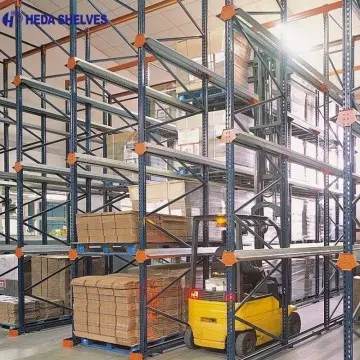
High density drive-in chemical storage rackingBulk Storage

Drive-In Chemical Bulk Racks

Eliminates access aisles for high-volume non-reactive bulk raw ingredients, polymer resins, and packaged pigments. Heavy-duty ground guide angles protect column uprights from forklifts.

  • High volume raw storage
  • Heavy floor anchors
  • Reinforced top ties
Get chemical layout & pricing
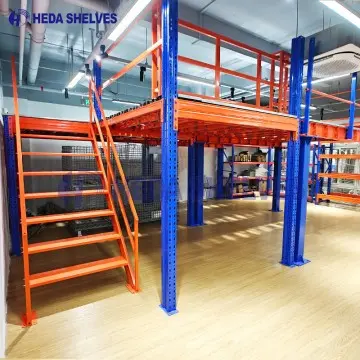
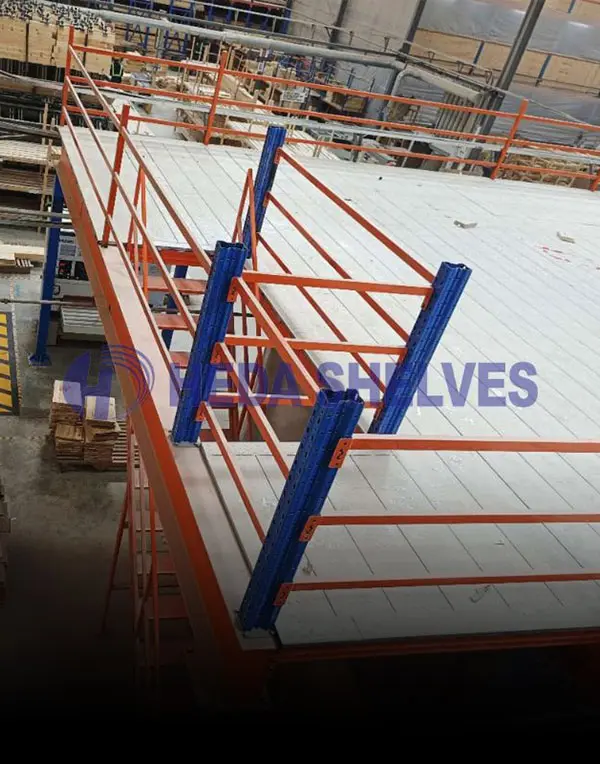
Mezzanine floor for chemical laboratory and samplingLaboratory

Chemical Mezzanine & Mixing Platform

Heavy duty structural steel platforms engineered to support bulk dosing tanks, sampling rooms, and QA testing laboratories above the main chemical warehouse floor.

  • 500–1,200 kg / m²
  • Chemical-proof decking
  • Safety handrail kickplates
Get chemical layout & pricing
Multi-tier chemical parts and small container shelving systemSmall Packs

Multi-Tier Reagent & Small Pack Shelving

Designed for chemical testing facilities, agrochemical retail outlets, and pharmaceutical distribution centres managing thousands of high-potency small liquid bottles and powders.

  • Adjustable shelf dividers
  • Integrated fire sprinklers
  • Anti-tip column baseplates
Get chemical layout & pricing
Market Intelligence & Engineering Trends

Chemical Storage Racking Trends: Procurement & Technology Shifts

As global chemical storage regulations tighten under OSHA, REACH, and Safe Work Australia mandates, international procurement leaders are pivoting away from generic pallet racking toward custom-engineered, bund-integrated systems.

Future Procurement Trends Shaping Chemical Warehousing

1. Strict Decoupling of Generic vs. Hazardous Storage Specifications: Procurement teams no longer purchase generic pallet racking for chemical warehouses. Specifications now require strict verification of steel tensile yield, localized point-load deflection thresholds (under L/200 or L/300 deflection standards), and certified compatibility with toxic, flammable, or oxidising contents.

2. Direct-from-Factory Integration of Secondary Containment: Rather than sourcing third-party polyethylene spill trays that deteriorate or fail under point loads, global EPC contractors are mandating factory-fitted steel sump bunds welded and tested for hydrostatic seal integrity directly from the manufacturer.

3. Advanced Duplex Protective Finishes: Warehouses handling fertilisers, caustic alkalis, and inorganic acids are moving from standard polyester coatings to heavy-duty duplex surface treatments—combining hot-dip galvanising with high-adhesion chemical-resistant epoxy topcoats to eliminate pitting corrosion at bolt connections.

4. In-Rack Automated Fire Suppression & Flue Space Controls: Future chemical warehousing tenders mandate calibrated 75mm–150mm transverse and longitudinal flue spaces permanently secured by structural rack back-stops, accommodating integrated NFPA 30 ceiling and in-rack ESFR sprinkler lines.

Technology Development & Structural Safety Evolutions

1. Smart Load & Deflection Sensor Integration: The evolution of IoT-enabled racking now allows procurement teams to install stress-strain micro-sensors directly within chemical rack uprights and critical cross-beams. These sensors send alerts before micro-fractures develop due to dynamic liquid surging inside bulk IBC totes during loading cycles.

2. FEA Non-Linear Dynamic Seismic Simulation: Seismic risk represents the catastrophic tipping point in chemical storage. Modern chemical racking systems must be mathematically simulated using 3D Finite Element Analysis (FEA) to calculate the precise sloshing inertia of liquid drums during seismic events (NZS 1170.5 and AS 1170.4 compliance).

3. Automation and Isolated Dangerous Goods Shuttles: To reduce chemical exposure risks for forklift operators in volatile atmospheres, facilities are rapidly adopting semi-automated explosion-proof radio shuttle carriers operating inside cold or high-density chemical storage tunnels.

4. Closed-Loop Circular Steel Accountability: Multinational corporate ESG directives now evaluate steel coil mill origins, non-toxic pre-treatment chemistry (chromium-free conversion coatings), and 100% recyclability of end-of-life racking steel frames.
Enterprise Strength & Engineering Authority

Guangzhou Heda Shelves Co., Ltd.: 25 Years of Precision Racking Manufacturing

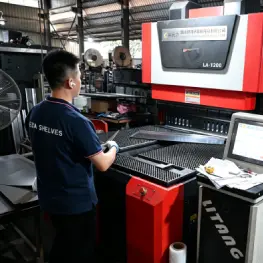
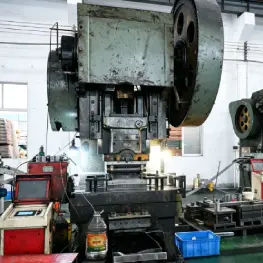
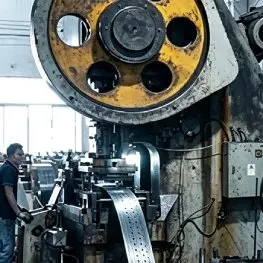
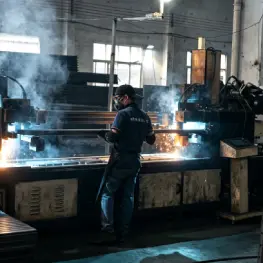
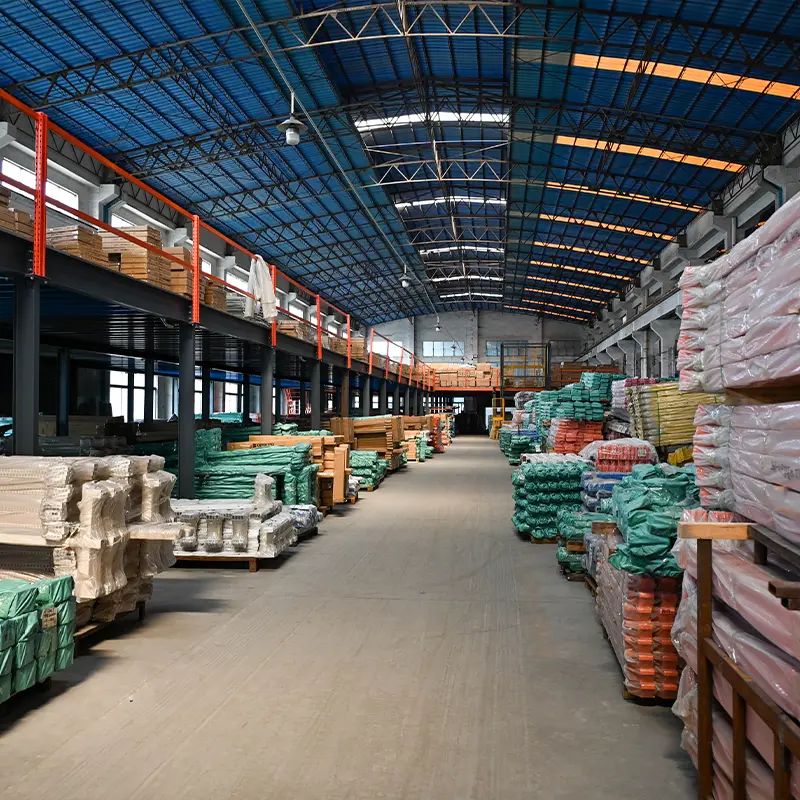
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has established itself as an engineering-led manufacturing leader in heavy-duty industrial storage equipment. Operating an expansive modern facility of over 30,000 square meters, our factory is powered by advanced automated CNC roll-forming lines, laser profiling centers, robotic welding cells, and high-efficiency continuous electrostatic powder-coating systems.

With an annual output capability exceeding 30,000 metric tons per month and a dedicated workforce of over 300 experienced engineers, structural technicians, and manufacturing professionals, Guangzhou Heda Shelves Co., Ltd. delivers engineered reliability for high-risk industrial facilities. We partner closely with logistics hubs, chemical processing plants, and racking distributors worldwide to provide fully certified, safety-verified storage solutions that stand up to rigorous regulatory scrutiny.

  • 10,000+ Completed ProjectsProven industrial warehousing installations
  • 30,000 Tons Monthly OutputHigh-volume capacity with strict QC tolerance
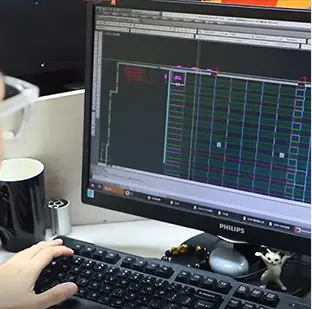
  • Free 3D & CAD LayoutsEngineered within 24 hours of site enquiry
  • Full Standards ComplianceAS 4084, CE, ISO 9001:2015 & RoHS certified
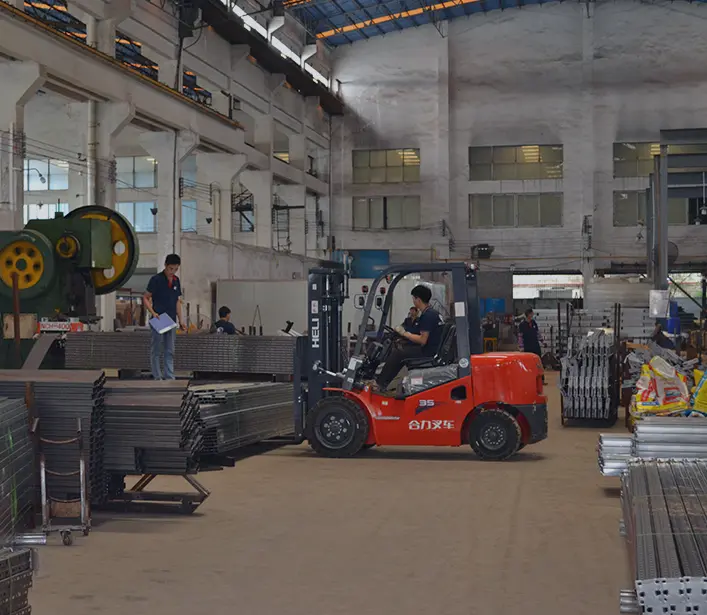
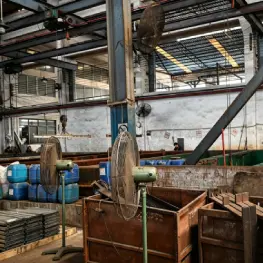
Guangzhou Heda Shelves Co., Ltd. racking production plant Inside Guangzhou Heda Shelves Co., Ltd. 30,000 m² Plant
  • 2001
    Year Established
  • 0+
    Racking Engineers & Techs
  • 0t
    Monthly Steel Capacity
  • 0m²
    Factory Footprint
Production Excellence

Strict 10-Step Quality Control & Surface Treatment

Chemical storage requires immaculate steel integrity. Guangzhou Heda Shelves Co., Ltd. monitors every micro-millimeter of raw material through cold-forming, welding, automated pickling, and powder coating.

1
Chemical project consultation

Consultation & MSDS Review

We review your chemical MSDS, pallet weights, containment regulations, and forklift dimensions.

2
3D CAD chemical racking design

3D Layout & FEA Modeling

Accurate 3D layouts, sprinkler flue allowances, structural beam calculations, and bund sizing.

3
Chemical racking precision manufacturing

Precision Manufacturing

Certified Q235B/Q355B coil slitting, cold-bending profile forming, and automated multi-point welding.

4
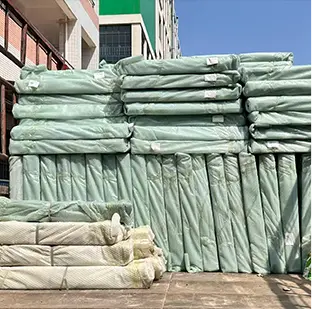
Export container shipping

Export Logistics & Support

Biosecurity-compliant ISPM-15/steel packaging, clear marking, and on-site engineering instructions.

Standardised Workflow

Inside Our 10-Step Heavy Industrial Production Line

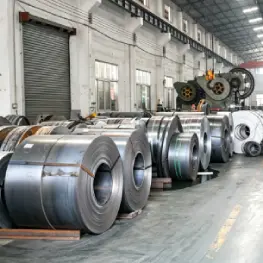
Raw steel coil materials
Step 01

Raw Material Mill Testing

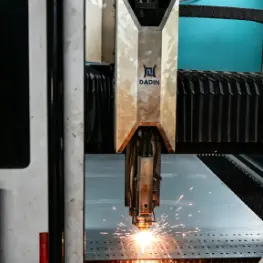
Precision steel cutting
Step 02

Laser & Precision Slitting

Automated upright column punching
Step 03

High-Speed Pitch Punching

Cold bending forming
Step 04

Cold Bending & Forming

Profile roll forming
Step 05

Upright & Beam Roll Forming

Steel polishing
Step 06

Weld Edge Shot Blasting

Robotic welding
Step 07

Robotic Bracket Welding

Pickling and phosphating pre-treatment
Step 08

Acid Pickling & Phosphating

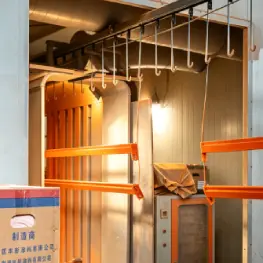
Electrostatic powder coating line
Step 09

Chemical Epoxy Coating

Quality control and export shipping
Step 10

Final Load Test & Packing

Rigorous Global Certification

Audited Quality Management & Structural Safety

At Guangzhou Heda Shelves Co., Ltd., transparency builds long-term engineering trust. We provide verifiable quality management credentials and mill test certifications with every chemical racking order.

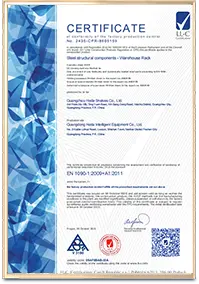
  • CE Structural CertificationNo. 2435-CPR-8605159 (EN 1090-1 / EN 15512)
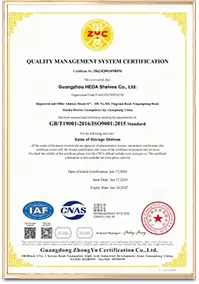
  • ISO 9001:2015 Quality SystemCertificate No. 18624Q00169R0M · Audited Facility
  • RoHS Chemical Safety ComplianceHazardous coating substances strictly eliminated
Request Verification Pack
ISO certification mark CE certification mark RoHS certification mark
Guangzhou Heda Shelves Co., Ltd. CE certificate
Guangzhou Heda Shelves Co., Ltd. ISO 9001 certificate
Guangzhou Heda Shelves Co., Ltd. RoHS certificate
Guangzhou Heda Shelves Co., Ltd. product test report

Trusted by chemical distributors and industrial manufacturers globally

Purchaser Questions & Answers

Frequently Asked Questions on Chemical Storage Racking Systems
Key technical, structural, and regulatory criteria that supply chain engineers, risk assessors, and international procurement directors evaluate before ordering.


Ask an Engineer directly
What engineering standards govern industrial chemical storage racking systems?
Chemical storage racking must satisfy both structural steel standards (such as AS 4084 in Australasia, EN 15512/EN 15620 across Europe, and ANSI MH16.1 in North America) and dangerous goods codes such as AS/NZS 3833, NFPA 30 (Flammable and Combustible Liquids Code), and OSHA 1910.106. These regulations dictate permissible beam deflection limits, fire flue spaces, seismic floor anchorages, and minimum bund containment capacities (typically required to hold at least 110% of the single largest container or 25% of the aggregate volume stored).
How does Guangzhou Heda Shelves Co., Ltd. prevent chemical corrosion on steel racking frames?

We execute an intensive 10-step surface pre-treatment workflow in our factory. After mechanical blasting, steel profiles undergo industrial acid pickling to eliminate mill scale, followed by zinc phosphating and a continuous electrostatic application of high-durability epoxy-polyester powder. For aggressive acidic environments, fertiliser distribution warehouses, and high-humidity coastal ports, Guangzhou Heda Shelves Co., Ltd. provides full hot-dip galvanisation complying with ISO 1461, ensuring lasting metallurgical corrosion resistance for over 20 years.

How do you accommodate high-point loads from 1,000L IBC tanks and chemical drums?

Unlike standard wooden pallets where loads are distributed evenly across beam surfaces, 1000L IBCs concentrate over 1,200kg across small footprint feet or steel corners, and four 205-litre drums produce heavy localized shear stress. We manufacture structural box beams with heavier material gauges (up to 2.5mm–3.0mm), reinforce bays with welded heavy-gauge underside pallet support bars, and supply specialized curved drum cradles that securely prevent rolling or point deflection.

Can chemical racking systems be designed for high seismic active zones?

Yes. Our engineering department uses Finite Element Analysis (FEA) to account for liquid sloshing dynamics (convective and impulsive liquid loads) inside storage drums during seismic acceleration. We reinforce column profiles with enlarged floor baseplates, heavy duty chemical epoxy foundation anchors, dual diagonal back-bracing trusses, and reinforced horizontal row spacers in accordance with NZS 1170.5 or AS 1170.4 parameters.
What engineering documentation and quality certificates accompany global shipments?

Every overseas shipment manufactured by Guangzhou Heda Shelves Co., Ltd. includes certified mill test certificates (MTC) for Q235B/Q355B steel, official CE declaration of performance (Certificate No. 2435-CPR-8605159), ISO 9001:2015 audit reports, structural design calculation packages, 3D and 2D CAD site installation plans, and AS 4084 / EN compliant Safe Working Load (SWL) plaques for end-of-aisle mounting.

Engineered Safety Consultation

Request Your Engineered Chemical Racking Layout

Partner with Guangzhou Heda Shelves Co., Ltd. to optimize your chemical storage density while exceeding national compliance mandates. Our senior design engineers return a complimentary 3D CAD proposal and load calculation within 24 hours.

Building DimensionsWarehouse CAD, clear heights & fire zones
Chemical ClassificationMSDS classes, corrosive levels & bunding volumes
Container Specifications205L drums, 1,000L IBCs, or carboys
Pallet Load WeightsMaximum unit weight per storage position
Material Handling FleetCounterbalance, reach truck, or VNA turret specs
Geographic FactorsSeismic zoning and outdoor coastal weather requirements