Engineered Warehouse Racking Portfolio
Precision-engineered high-bay and dynamic racking systems optimized for maximum cubic volume utilization, automated crane integration, and seismic safety compliance worldwide.
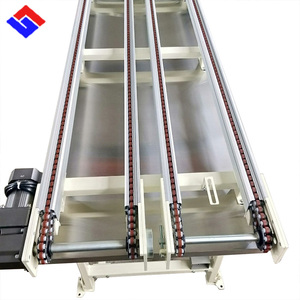 ASRS Integration
Aluminum Rail Motorized Duplex Chain Pallet Flow Conveyor
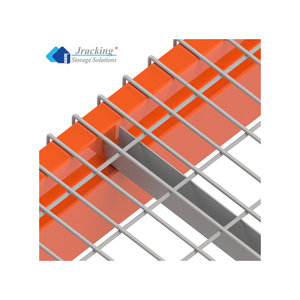 Fire Safety Compliant
Selective Pallet Rack with Waterfall Wire Mesh Decking
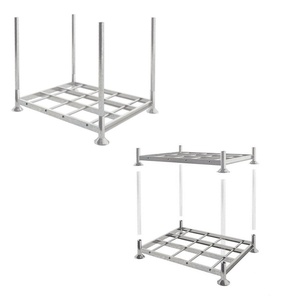 Extreme Duty
Heavy Duty Modular Steel Truck Tire & Stacking Racks
 Semi-Automated
Intelligent Wireless Radio Shuttle Robot Racking System
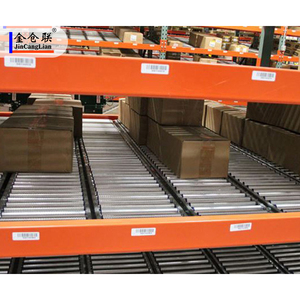 FIFO Flow
Dynamic Live Gravity Pallet Flow Storage Racking
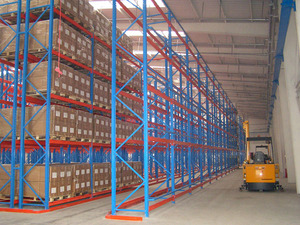 LIFO Storage
Telescopic Multi-Layer Push-Back Pallet Rack System
 Intralogistics ASRS
Intelligent Warehouse Automation 4-Way Shuttle Racks
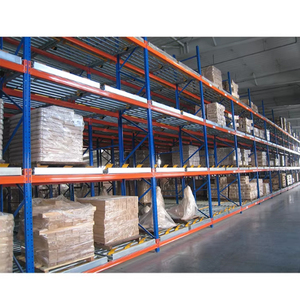 Roller Track
Heavy Duty FIFO Flow-Through Pallet Roller Racking
Engineering White Paper: Structural Integrity & Compliance in High Bay Warehousing
Modern distribution centers, automated 3PL mega-hubs, and cold storage facilities increasingly depend on vertical storage optimization exceeding 15 to 40 meters in free-standing height. In these extreme load environments, high-bay racking ceases to be passive steel shelving and acts as a primary load-bearing structural skeleton. As an authoritative manufacturer and exporter, Guangzhou Heda Shelves Co., Ltd. builds high-bay pallet racking under strict conformity with the European Construction Products Regulation (CPR 305/2011), holding validated CE Certification (No. 2435-CPR-8605159), along with ISO 9001:2015 quality management governance.
High bay installations, particularly Clad-Rack Warehouse Structures (rack-supported buildings where racking supports wall claddings and roof wind loads), require meticulous finite element analysis (FEA). Structural stability is verified against global dynamic load benchmarks, primarily EN 15512 (Steel static storage systems – Adjustable pallet racking systems – Principles for structural design), EN 15620 (Tolerances, deformations and clearances), and the australasian AS 4084 code. Upright columns are manufactured from cold-formed high-tensile steel grades such as Q355B and S355MC, profiled through multi-stage CNC rolling mills to preserve microstructural yield strength and prevent torsional buckle under heavy axial loads.
| Technical Parameter | Conventional High Bay Racking | Automated Crane High-Bay (ASRS) | HEDA High-Tensile Standard |
|---|---|---|---|
| Operating Height Limit | Up to 15 Meters (VNA Forklift) | Up to 40+ Meters (Staker Crane) | Up to 42 Meters (Custom Engineered) |
| Structural Deflection | Beam Deflection ≤ L/200 | Beam Deflection ≤ L/300 or L/400 | FEM 9.831 / EN 15620 Class 100-300 Compliant |
| Manufacturing Steel Grade | Q235B Structural Carbon | Q355B / S355MC Micro-Alloyed | Certified High-Yield S355 Cold-Formed Steel |
| Seismic Damping & Anchor | Standard Wedge Expansion Anchors | Engineered Chemical Resins | Dual Chemical Anchoring + Slotted Baseplates |
| Tolerance Deviations | ± 3.0 mm per upright tier | ± 1.0 mm cumulative over 30m | Laser-Guided CNC Punching Precision ± 0.5 mm |
When engineering high-bay structures for high-seismic risk regions (such as New Zealand's Wellington fault line according to NZS 1170.5, or seismic zones throughout Southeast Asia and the Mediterranean), cross-aisle bracing, spine bracing trusses, and energy-dissipative base anchors are integrated into the primary CAD engineering pack. Every consignment supplied by HEDA Shelves comes backed by raw mill test certificates (MTC EN 10204 Type 3.1), comprehensive structural calculations, and installation torque maps for critical anchor bolts.
Future Sourcing & Procurement Trends
Warehouse directors, procurement consultants, and 3PL enterprises must balance upfront capital expenditure with total lifecycle survivability. Critical transformations are dominating industrial racking procurement through 2030.
Convergence of Racking with Automation (ASRS)
Purely manual forklift racking is being replaced by hybrid or semi-automated architectures. Sourcing strategies now prioritize standard pallet frames compatible with retrofittable radio shuttles, 4-way robotic shuttles, and automated guided vehicles (AGVs) without tearing down existing upright frameworks.
Life-Cycle Assessment (LCA) & Green Steel
Global supply chain tenders increasingly evaluate environmental product declarations (EPD) and embodied carbon. Procuring warehouse racking produced via energy-efficient electric arc furnaces (EAF) with heavy-metal-free thermosetting powder coatings prevents cross-border carbon border tax penalties.
Supply Chain De-risking & Direct Sourcing
Enterprise logistics hubs bypass tiered intermediary brokers to source factory-direct from certified manufacturers. Direct factory engagement guarantees transparent structural calculations, certified material grades, complete custom stamping, and significantly lower project costs.
Technological Evolution: Next-Generation Warehouse Racking Systems
The logistics hardware sector is undergoing an engineering transition spurred by rising industrial land valuations and the rapid growth of autonomous logistics robots. High bay racking is developing into a responsive, modular, and digitally verified operational asset through several key innovations:
1. Sub-Millimeter Geometric Tolerances for Robotic Handling: Automated Storage and Retrieval Systems (ASRS), including high-speed stacker cranes traveling up to 4 m/s horizontal acceleration, cannot tolerate the deflection rates acceptable in conventional counterbalanced forklift bays. In compliance with FEM 9.831 and EN 15620 Class 100 to 300 tolerances, automated profile cold-rolling lines at HEDA achieve strict column straightness (deviation under 1/1000 of length) and hole punch repeatability within ±0.1 mm, preventing crane shuttle jams.
2. Advanced Protective Surface Finishes: Standard indoor industrial powder coating fails rapidly in extreme humidity, offshore tropical islands, or refrigerated environments. Modern high bay racking incorporates continuous automatic multi-stage chemical pretreatment (acid pickling, zinc phosphating, and deionized passivating rinses) followed by high-voltage electrostatic polyester powder coating. In aggressively corrosive environments, continuous pre-galvanized coils or ISO 1461 hot-dip galvanization are utilized for lifetime corrosion resistance.
3. Dense Radio Shuttle & Autonomous 4-Way Shuttle Racks: Radio shuttle systems bridge the gap between static drive-in racks and multi-million dollar ASRS cranes. A self-powered carrier moves along customized guide rails beneath stored pallets, controlled via Wi-Fi or tablet interfaces. The operator deposits goods at the bay opening while the shuttle transports, stacks, and aligns items deeper in the channel, drastically lowering lift truck travel distance, eliminating racking upright impact damage, and doubling storage density.
Why Partner with Guangzhou Heda Shelves Co., Ltd.
Founded in 2001, HEDA Shelves has expanded into a global storage infrastructure leader with a 30,000 square meter state-of-the-art production base and over 300 dedicated professionals.
Verified CE Certification
Certified under CE No. 2435-CPR-8605159 and ISO 9001:2015. Every structural load table, column section property, and beam weldment is traceable and certified for regulatory inspections worldwide.
Massive Industrial Scale
30,000 m² centralized fabrication facility delivering over 30,000 metric tons of finished racking components each month. We handle multi-thousand-pallet turn-key megaprojects without production bottlenecks.
Free 3D & Structural CAD
Our in-house structural engineering team delivers free, complete 3D visualization and finite-element CAD space layouts within 24 to 48 hours, fully modeled around your specific pallet sizes and building columns.
Biosecurity & Export Packing
Shipments destined for Oceania, North America, and Europe are packaged in solid steel stillages or ISPM-15 heat-treated dunnage, guaranteeing zero delays at strict biosecurity customs check-points.
Complete Tariff Documentation
We supply full preferential tariff documentation, including commercial invoices, certificates of origin (ChAFTA, RCEP, Form A/E), and packing manifests to optimize import duties and clearance speed.
Global Installation Oversight
Every component is stamped with an erection tag cross-referenced to assembly drawings. We provide clear installation manuals, remote video guidance, and on-site engineering supervisors for international turnkey projects.
End-to-End 10-Step Quality Controlled Manufacturing Chain
Every beam, upright column, brace, and baseplate is manufactured under one roof under strict ISO 9001:2015 tracking.
Raw Steel Testing
Chemical & tensile verification of all hot-rolled coils.
Precision Slitting
Automatic steel cutting to tight geometric margins.
CNC Punching
Automated column pitch punching at high repeatable speed.
Multi-Pass Rolling
Continuous cold roll-forming with up to 24 rollers.
Profile Straightening
Hydraulic tensioning to ensure zero twist or camber.
Surface Polishing
Mechanical deburring and high-velocity shot blasting.
Robotic Welding
Shielded gas robotic seam welding on beam connectors.
Chemical Phosphating
Multi-bath acid pickling and anti-corrosion pretreat.
Powder Coating
Electrostatic curing at 200°C for wear-resistant finish.
Final QC & Pack
Load sampling, bundle strapping, and containerization.
High Bay Racking Procurement FAQ
In-depth structural, compliance, and logistics answers for warehouse engineers and procurement officers.
Ready to Engineer Your High Bay Storage Infrastructure?
Submit your warehouse floor layout, storage profile, and operational parameters. Our senior structural design engineers will deliver a free 3D CAD proposal, load analysis, and competitive factory-direct quote within 24 hours.