Precision-Engineered Pallet Shuttle Systems & High-Density Racks
Direct-from-factory intelligent storage configurations. Certified under European Standard EN 15512, AS 4084, and ISO 9001:2015, each structure is optimized for high-velocity distribution hubs, FMCG cold chains, and automated warehousing.
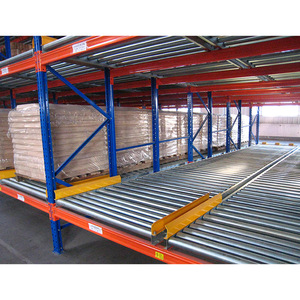
FIFO High Efficient Warehouse Storage Gravity Pallet Flow Racks
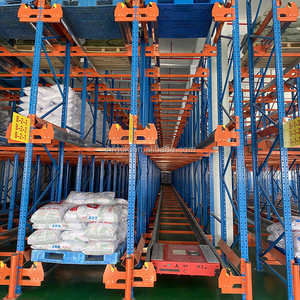
Advanced High-Density AS/RS Pallet Shuttle Rack System
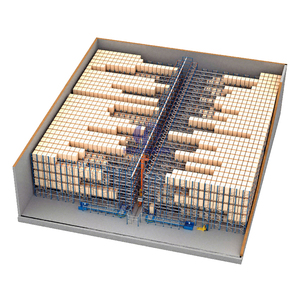
Cold Storage AS/RS 4-Way Radio Shuttle Racking System
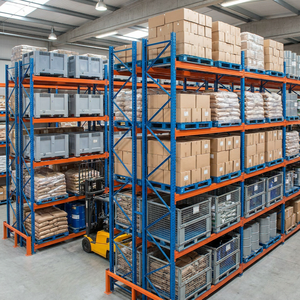
Selective Heavy-Duty Pallet Racking Industrial Q235B Steel
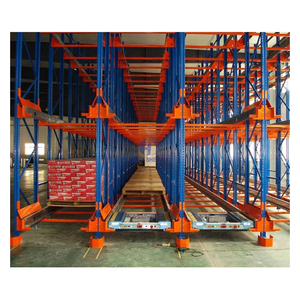
Custom Heavy-Duty Automatic Storage Shuttle Pallet Rack
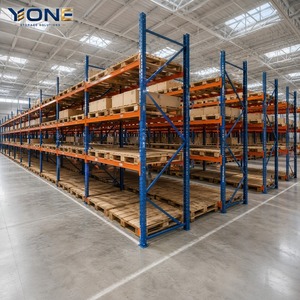
Industrial Pallet Racking Selective System (1000–4000kg)
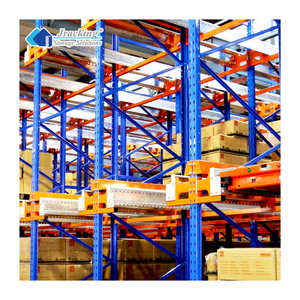
CE Certified Double-Sided Two-Way Radio Shuttle Rack System
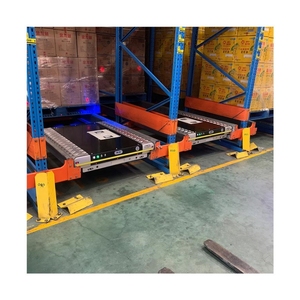
Heavy Duty Industrial Steel Warehouse Shuttle Racking System
Structural Rigidity, CE Verification & Metallurgy Standards
Modern intralogistics infrastructure demands zero tolerance for structural fatigue and geometric deflection. Our pallet shuttle racking systems are calculated using Finite Element Analysis (FEA) under strict adherence to European Standard EN 15512 and Machinery Directive 2006/42/EC.
Certified High-Tensile Steel Profiles
We deploy certified prime Q235B and high-yield Q355B cold-rolled structural steel, sourced exclusively from top-tier state-owned mills with full mill test certificates (MTC). Structural uprights feature omega-profile geometry with multiple load-bearing return flanges to maximize second moment of area (I-value), mitigating torsional buckling under extreme vertical loads.
- Yield strength verified: ReH ≥ 355 N/mm²
- Tolerances strictly conforming to EN 15620 Class 400
- Deflection ratios engineered beyond 1/500 thresholds
CE Machinery & Low Voltage Safety Directives
Unlike standard static racking, pallet shuttle storage is a dynamically motorized machine classification. Our systems carry CE Mark compliance under Certification No. 2435-CPR-8605159, harmonized under the Machinery Directive 2006/42/EC and Electromagnetic Compatibility (EMC) Directive 2014/30/EU. Onboard intelligent shuttles integrate emergency stop circuits, dual optical obstacle detection, and software interlocks.
- Dual Category 3 / PL d safety sensing architectures
- EN 528 compliance for automated guided carriers
- Independent third-party laboratory dynamic load verified
Patented Precision Guide Rails
The interface between the shuttle carrier wheels and the racking structure represents the highest mechanical friction point. We utilize continuous roll-formed, heavy-gauge galvanized steel guide rails with integral centering lips. These rails double as the continuous support ledge for pallets and the running surface for shuttle wheels, eliminating horizontal tracking drift and wheel rim degradation.
- Hot-dip galvanized zinc layer: 275g/m² corrosion barrier
- Anti-derailment lip design preventing vehicle dislodgement
- Vibration-dampened boltless rail connector sleeves
System Comparison: Engineering Data & Volumetric ROI
Selecting the correct high-density storage configuration requires analyzing aisle clearance ratios, forklift travel times, structural damage vectors, and initial versus ongoing operational expenditure (OPEX).
| Evaluation Parameter | Radio Shuttle Racking | Drive-In Racking System | Push-Back Cart System | Automated AS/RS 4-Way |
|---|---|---|---|---|
| Volumetric Space Utilization | 85% – 90% (Ultra High) | 70% – 75% (Moderate) | 75% – 80% (High) | 92% – 96% (Maximum) |
| Forklift Mast Damage Vector | Virtually Zero (External Only) | High (Mast Enters Racks) | Low (Aisle Pick Face Only) | Zero (Fully Automated) |
| Inventory Rotation Protocols | FIFO or LIFO Selectable | Strict LIFO Only | Strict LIFO Only | Dynamic FIFO & LIFO Batching |
| Throughput (Pallets / Lane / Hr) | 40 – 60 Pallets / Shuttle | 15 – 22 Pallets / Truck | 20 – 30 Pallets / Truck | 80 – 120+ Pallets / Tier |
| Lane Depth Potential | Up to 40+ Pallets Deep | Max 6 – 10 Pallets Deep | Max 4 – 6 Pallets Deep | Unlimited Continuous Grid |
| Sub-Zero Cold Store Efficiency | Optimal (-30°C LiFePO4) | Poor (High Air Infiltration) | Average (Gravity Sticking) | Maximum Thermal Efficiency |
| Labor Cost Reduction Impact | 50% – 60% Fleet Optimization | Baseline | 20% Reduction | Up to 85% Headcount Reduction |
*Data calculated based on standard 1200 x 1000mm industrial Euro/UK pallets and 1165 x 1165mm Australian standard pallets operating in a 10-meter ceiling warehouse environment.
Strategic Procurement Trends for Pallet Shuttle Systems (2025–2030)
Global supply chain directors and engineering EPC contractors are shifting from single-vehicle semi-automation toward interconnected, energy-regenerative intra-facility micro-ecosystems.
Transition from 2-Way Carriers to 4-Way AS/RS
While traditional 2-way semi-automated shuttles require manual forklift transfer between storage channels, future-ready facilities are increasingly investing in 4-Way multi-directional shuttle matrices. Equipped with transverse directional wheel shifting, vertical lifts (reciprocating hoists), and fleet routing algorithms, 4-way systems unlock fully autonomous, lights-out pallet movement with zero human footprint inside storage aisles.
Sub-Zero LiFePO4 Chemistry & Fast Inductive Charging
Cold chain logistics operations (storing pharmaceuticals, ice cream, meat, and frozen seafood at -18°C to -30°C) previously suffered from rapid lead-acid battery voltage drops. Modern procurement emphasizes internally heated Lithium Iron Phosphate (LiFePO4) battery packs combined with automated inductive rail-charging pads. Shuttles automatically top up charge during pallet dwell times, guaranteeing 24/7 uninterrupted uptime without manual battery extraction.
Edge Telemetry, IoT Vibration Sensing & WMS Integration
CE-certified suppliers now embed IoT telemetry modules directly onto the shuttle chassis. Continuous real-time monitoring of wheel bearing vibration, motor temperature rise, brake pad wear, and optical rail alignment alerts maintenance engineers to potential failures before line stoppages occur. Seamless RESTful API and OPC UA connectivity connect the shuttle controller to SAP, Manhattan Associates, or proprietary enterprise WMS solutions.
Guangzhou Heda Shelves Co., Ltd. — 25 Years of Precision Manufacturing
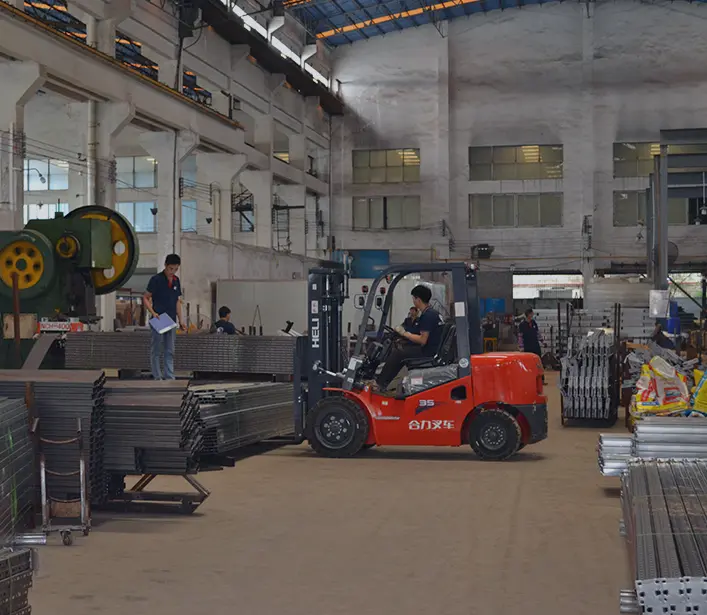
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has grown from a specialized roll-forming facility into a globally recognized warehouse storage equipment manufacturer. Covering an advanced 30,000 square meter production compound with over 300 experienced engineers, structural designers, and fabrication specialists, our monthly production capacity exceeds 30,000 tons of precision-engineered racking components.
• ISO 9001:2015 Quality Management System: No. 18624Q00169R0M
• Full Compliance with RoHS Directive & AS 4084 / NZS 1170.5 Seismic Criteria
We provide full structural data packages for every project: structural section modulus, load deflections, finite element analysis (FEA) reports, and customized CAD layout calculations. From bulk grain hubs and chemical distribution centers to rapid-turnover 3PL cold stores, Heda Shelves provides OEM/ODM manufacturing partnerships that bridge international standards with competitive factory pricing.
Frequently Asked Questions for Pallet Shuttle Procurement
Direct answers to the critical structural, mechanical, electrical, and compliance questions asked by procurement directors, warehouse engineers, and plant operators.