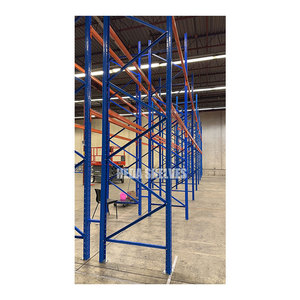
 Heavy Duty
4-Layer 600kg Warehouse Stacking Case Flow Rack
- Capacity: 600 kg/tier uniform load
- Track: High-impact polymer rollers
- Application: Heavy spare parts sorting
Manufactured to ISO 9001:2015 and CE standards from high-tensile Q235B cold-rolled steel. Explore our certified case flow modules configured for distribution centers, manufacturing cells, and automated picking tunnels.
Heavy Duty
 Modular Lean
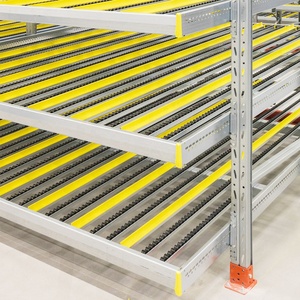 Dynamic FIFO
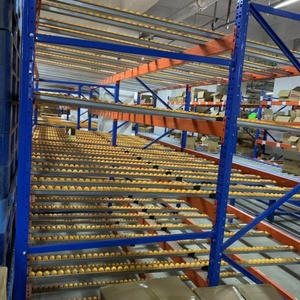 5-Tier High-Density
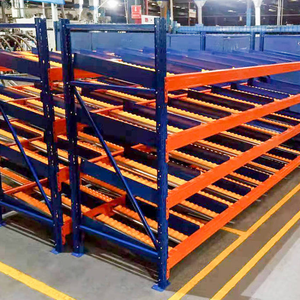 Boltless Quick-Fit
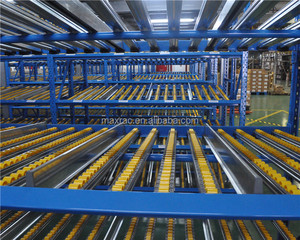 Maxrac System
 Multi-Level
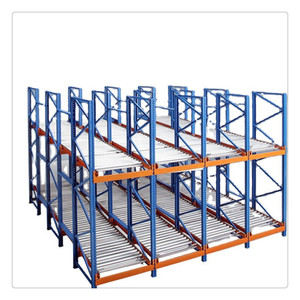 Bin Integration
A Case Flow Rack—commonly termed a carton flow rack or gravity feed live storage system—is a dynamic storage apparatus engineered specifically for high-density split-case and full-case picking operations. Operating strictly on the mechanical principle of gravity feed, individual storage lanes are inclined slightly downwards from the rear replenishment aisle (charging face) to the front retrieval aisle (discharging face). As a picker extracts the frontmost carton or plastic tote, the successive containers immediately coast forward to replenish the pick face automatically, adhering strictly to First-In, First-Out (FIFO) stock rotation.
From an intralogistics engineering perspective, case flow systems fundamentally eliminate picker transit waste. In traditional static shelving, up to 70% of total operator shift duration is consumed by dead-heading travel and cross-aisle traversal. Integrating case flow racks condenses linear pick faces by as much as 80%, consolidating hundreds of active SKUs into a compact, ergonomically optimized pick plane. Forklift restocking traffic is isolated entirely at the rear aisle, eliminating pedestrian-equipment collision hazards and creating an asynchronous workflow where replenishment and picking occur simultaneously without cross-dock congestion.
The operational reliability of a case flow rack depends entirely on precise kinetic modeling. If the track gradient is insufficient, static breakaway friction causes cartons to stall mid-lane; conversely, if the declination is excessive, accelerating cartons risk structural crushing upon impacting the front pick tray or bouncing out of the lane. Chinese manufacturers of high-tier case flow racks compute gravity kinematics using the governing friction-incline equation:
Modern Chinese manufacturing facilities configure case flow racks with two primary dynamic conveyance configurations: Full-Width Steel/Polymer Roller Beds and Multi-Track Plastic Skate-Wheel Flow Rails. Skate-wheel tracks utilize staggered wheels mounted inside cold-formed galvanized C-channels, delivering superior flexibility for variable carton footprints. Conversely, continuous cylindrical roller tracks with precision ball bearings provide continuous surface support, essential for corrugated cartons with structural belly sagging or non-rigid tote geometries.
Requires zero electrical power or motorized drives. Operates purely on gravitational potential energy, achieving lifelong operational cost neutrality with negligible carbon footprints.
Condenses dozens of linear meters of static shelving into compact vertical pick windows. Pick rates increase from 60–80 lines/hour to over 250–350 lines/hour per picker.
Eliminates stock aging, batch expiration, and shrinkage in perishable goods, pharmaceuticals, cosmetics, and cold-chain distribution centers through physical lane segregation.
Selecting an optimal order-fulfillment infrastructure requires evaluating volumetric storage density against equipment CapEx and labor throughput. The engineering comparative matrix below models how heavy-duty case flow racks compare against alternative warehouse storage typologies across critical material handling variables:
| Storage Architecture | Stock Rotation | Pick Face Density | CapEx / Pick Face | Replenishment Interference | SKU Selectivity | Maintenance Lifecycle |
|---|---|---|---|---|---|---|
| Carton / Case Flow Rack | Strict FIFO (100%) | Ultra-High (80% Aisle Reduction) | Moderate ($45 - $95 / lane) | Zero (Dedicated Rear Charge) | 100% Immediate Face Access | Low (Self-lubricating rollers) |
| Static Industrial Shelving | LIFO / Random | Low (Extensive aisle footprint) | Lowest ($15 - $35 / shelf) | High (Same-aisle blockages) | High (Manual search required) | Negligible (Static structure) |
| Selective Pallet Racking | FIFO / LIFO by Bay | Low (Requires forklift aisles) | Moderate ($65 - $120 / pallet) | Severe (Forklift aisle closures) | Restricted to pallet face | Low (Subject to impact damage) |
| AS/RS Mini-Load System | System Automated | Maximum (Vertical cube utilization) | Extremely High ($800k+) | Zero (Crane automated) | Sequential Crane Cycle | High (Complex mechatronics) |
| Push-Back Rack (Carts) | Strict LIFO | High (Aisle consolidated) | High ($140 - $220 / position) | Moderate (Single face charge) | Low (Single SKU per lane) | Moderate (Cart tracks & stops) |
China has established unchallenged global leadership in the engineering, fabrication, and export of industrial gravity flow systems. Operating at the confluence of upstream metallurgy and advanced cold-roll forming automation, premier Chinese rack manufacturers like Guangzhou Heda Shelves Co., Ltd. (HEDA Shelves) provide industrial engineering firms worldwide with structural advantages that domestic Western fabricators cannot match on lead times or cost-to-performance metrics.
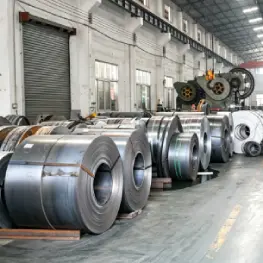
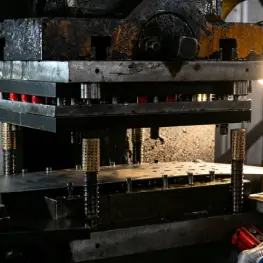
The manufacturing process begins with structural-grade Q235B and Q355B cold-rolled carbon steel coils procured from Tier-1 integrated mills including Baosteel and Ansteel. Q235B provides an optimal yield strength threshold ($f_y \ge 235 \text{ MPa}$) with high elongation ductility, preventing structural embrittlement or micro-cracking during deep cold-roll forming operations. Upright profiles feature precision continuous-hole matrix stamping executed on automated high-speed CNC pressing lines, ensuring universal tolerance consistency within ±0.5mm across entire 12-meter production runs.
Furthermore, Chinese manufacturers lead in roller compound formulations. Rollers feature high-impact acrylonitrile butadiene styrene (ABS) or pure high-density polyethylene (HDPE) infused with anti-static agents and UV inhibitors. Roller axles feature cold-drawn galvanized steel rods fitted with self-lubricating nylon bush bearings or precision shielded steel ball bearings capable of operating flawlessly in temperature extremes ranging from -30°C in industrial blast freezers to +50°C in ambient distribution hubs.
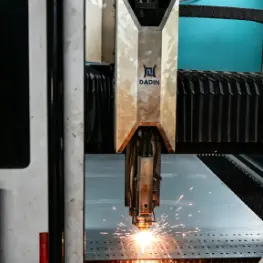
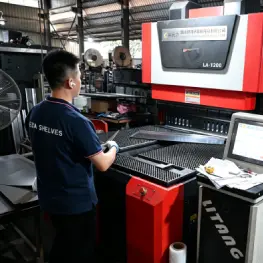
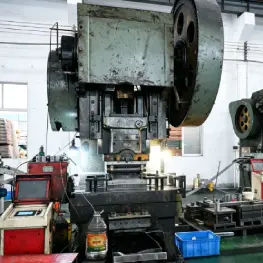
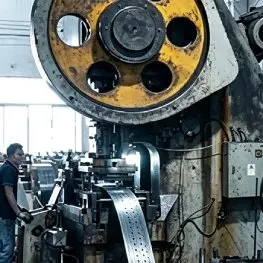
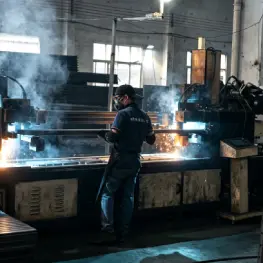
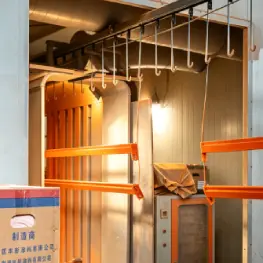
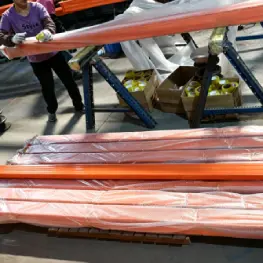
Achieving defect-free roller alignment and structural integrity across multi-tier case flow installations requires an unyielding production regime. At HEDA Shelves, every batch undergoes an automated 10-stage fabrication protocol overseen by our internal quality control department:
The intralogistics landscape is experiencing rapid evolutionary pressure driven by labor scarcity and accelerated order-to-delivery Service Level Agreements (SLAs). Global procurement managers must account for three structural innovations when specifying case flow rack systems from China over the coming decade:
The traditional human-dominated case flow picking face is rapidly converging with Autonomous Mobile Robots. Leading distribution architectures position case flow racks above or flanking autonomous transport corridors. AMR units navigate down central pick tunnels beneath rack-supported platforms, autonomously loading totes delivered from elevated gravity-feed roller shelves. Chinese factories have engineered specialized flush cantilevered pick trays with integrated laser-guided optical sensors and mechanical docking latches tailored specifically for robotic gripper end-effectors.
Legacy case flow shelves required labor-intensive bolting or screw-fastened track assemblies, severely inhibiting lane reconfiguration when carton dimensions changed during seasonal retail shifts. Next-generation systems feature tool-less clip-on aluminum track retainers that snap into place on 10mm increment lateral pitch bars. Warehouse operators can resize lane widths, insert full-length zinc dividers, or convert from single skate-wheel tracks to heavy full-width rollers within seconds without mechanical tools.
Advanced Chinese case flow racks now offer factory-prewired extruded profile channels designed to conceal data cabling for Pick-to-Light (PTL) and Put-to-Light visual displays. Coupled with miniature piezoelectric load cells placed underneath front discharge stops, the rack autonomously logs pick confirmation via carton weight differential, transmitting real-time inventory decrements to the Warehouse Management System (WMS) without requiring manual barcode scans.
Industrial structural safety permits zero tolerance for manufacturing variance. All case flow systems produced by HEDA Shelves carry documented, third-party verified accreditations confirming adherence to rigorous mechanical load testing and global environmental protocols:
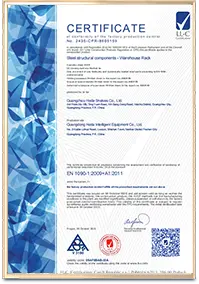
Ref: No. 2435-CPR-8605159
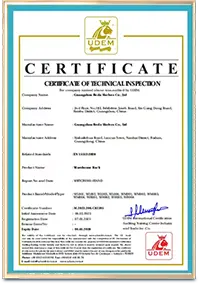
Cert: No. 18624Q00169R0M
Heavy Metals & VOC Controlled
SGS Verified Dynamic Deflection
For international supply agreements, our structural calculations cross-reference AS 4084-2023 (Australian Standard for Steel Storage Racking), EN 15512:2020 (European Standard for Adjustable Pallet and Carton Racking Systems), and site-specific seismic parameters adhering to NZS 1170.5 for projects across New Zealand and the Pacific Rim.
Review real-world high-throughput installations demonstrating how custom-engineered flow beds resolve heavy-load handling, multi-level integration, and rapid order picking challenges:
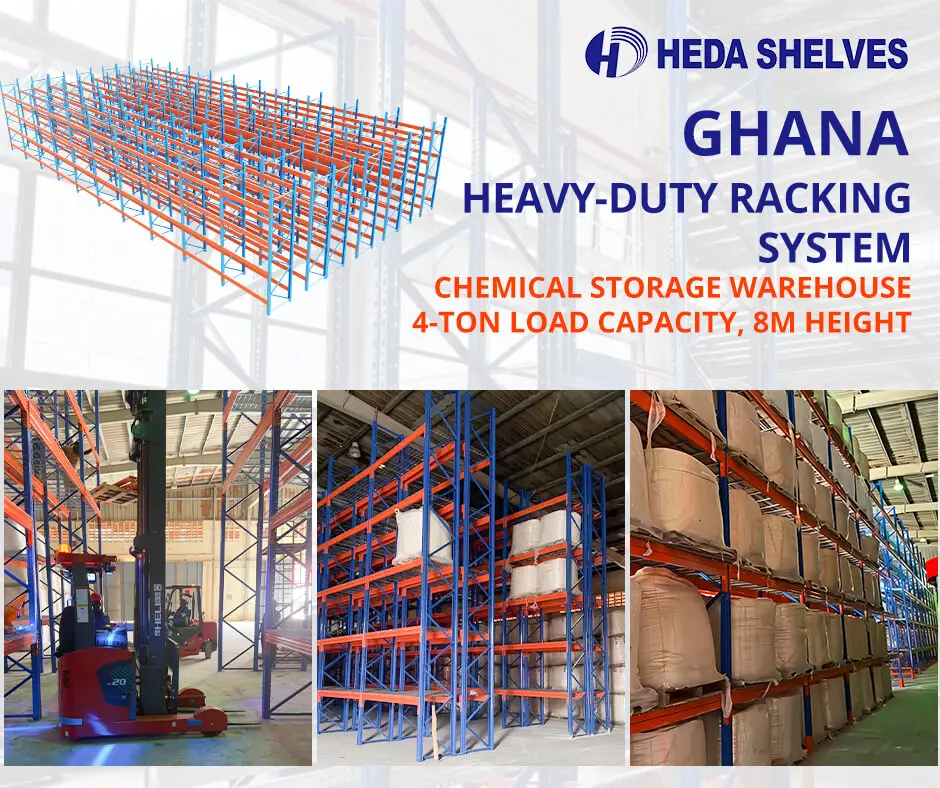
Corrosion-proof electrostatic powder-coated uprights with spark-resistant polymer rollers engineered for classified chemical processing facilities.
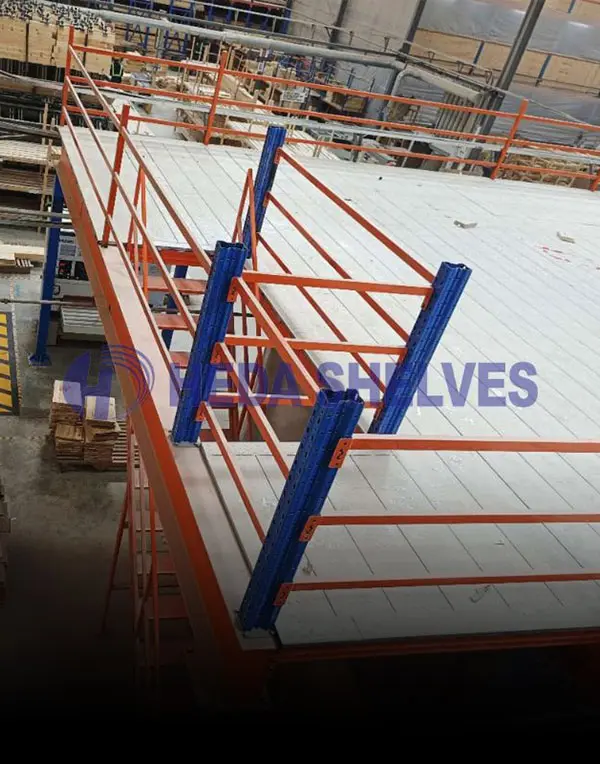
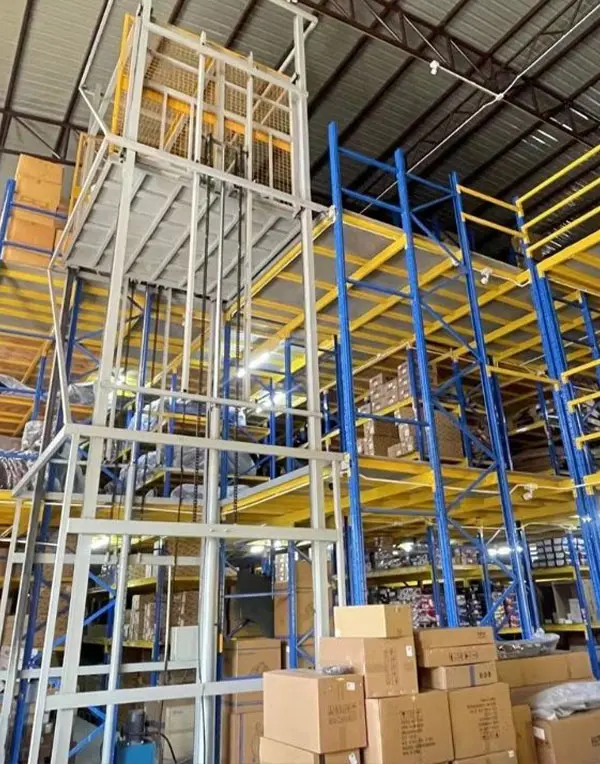
Two-tier carton flow pick tower integrating overhead structural catwalks, doubling floor pick facings without expanding building footprint.
Multi-lane flow racks featuring heavy-duty steel separator dividers and integrated kitting totes engineered for rapid OEM spare parts retrieval.
Key technical and commercial inquiries submitted by supply chain directors, industrial architects, and racking distributors importing case flow racking from China:
Accelerate your warehouse throughput with custom case flow systems engineered to your exact product dimensions, picking velocities, and seismic zone parameters. Share your warehouse floor plan today for a free design audit within 24 hours.
Connect immediately with our technical design team via live chat for instant layout advice and load rating verifications.
Send an Inquiry