Featured Industrial Racking & High-Density Storage Solutions
Manufactured from certified high-tensile Q235B and Q355B structural coil steel, our precision roll-formed warehouse racks deliver verified load capacities, strict deflection limits (L/200), and full compliance with international FEM 10.2.02, EN 15512, AS 4084:2023, and ANSI MH16.1 specifications.
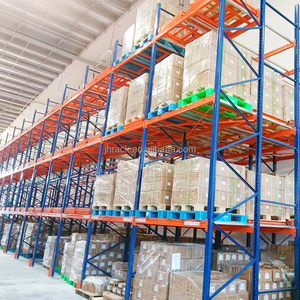
Industrial Push-Back Pallet Racks: Heavy-Duty Steel Storage System for Maximizing Warehouse Space and Efficiency
Nested cart carrier system storing 2 to 6 pallets deep per lane. Eliminates individual forklift travel aisles, utilizing gravity-fed incline tracks to boost floor utilization by up to 75% compared to selective racking.
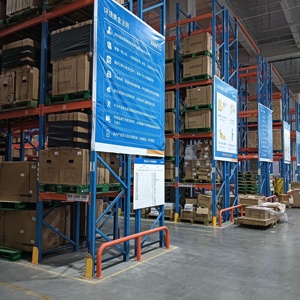
Heavy Duty Selective Pallet Rack with Custom Wire Mesh Decking High Load Steel Adjustable Warehouse Pallet Racking System
Universal industrial selective racking featuring step-beam configurations and welded wire mesh decks with flared waterfall edges. Delivers uninhibited overhead sprinkler water penetration and critical point-load drop safety.
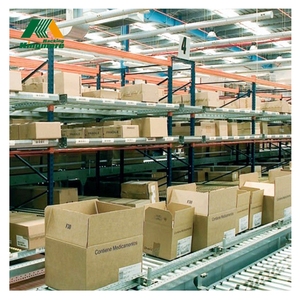
Customized Gravity Carton Flow Pallet Roller Rack System
Engineered roller beds and dynamic brake drums ensure smooth gravity-fed stock rotation for fast-moving consumer goods, pharmaceutical logistics, and temperature-controlled food distribution where strict batch rotation is non-negotiable.
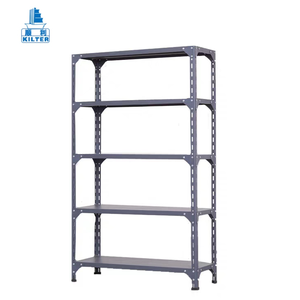
Storage Slotted Rack Metal Holders Adjustable Angle Steel Stand Shelf
Heavy-gauge slotted angle steel uprights designed for rapid boltless assembly and high-density manual parts storage. Powder-coated with electrostatically applied epoxy-polyester thermoset resin for harsh industrial environments.
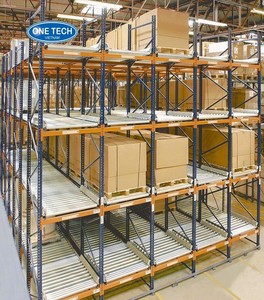
Versatile Modular Steel Carton Flow Racking System Heavy Duty Automatic Roller Track Fast Order Picking Design E-Commerce
High-speed split-case picking systems equipped with durable aluminum or sheet-metal roller tracks. Compatible with Pick-to-Light (PTL) hardware, separating replenishment personnel from pick operators to reduce fulfillment times by 40%.
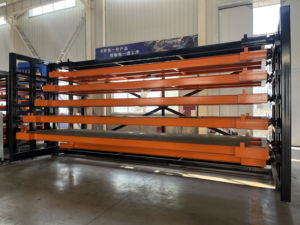
Multi-Layer Steel Heavy Duty Industrial Pipe Storage Rack Corrosion Protection 3000mm Height for Long Material Warehouse Storage
Unobstructed front cantilever design for non-palletized, long-span cargo such as structural steel tubing, extruded profiles, raw timber, and building sheets. Engineered with heavy hot-rolled I-beam bases and high-torsion pivot arms.
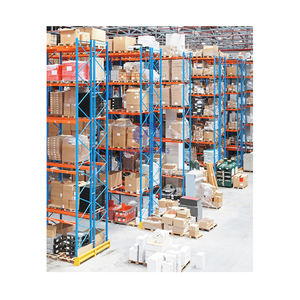
Heavy Duty Selective Pallet Racks Warehouse Rack System with Wire Mesh Decking for Industrial and Warehouse Use
Heavy-duty roll-formed selective pallet storage engineered with 4-hook beam connectors, integrated safety pins, and reinforced footplates anchored directly to reinforced concrete slab foundations. Tested for severe seismic zones.
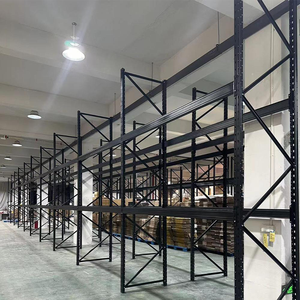
Wire Mesh Deck Pallet Racking Corrosion Resistant Dust Leakage Prevention 5-Layer Heavy Duty Warehouse Storage
Multi-tier structural racking with self-cleaning wire mesh shelving panels that prevent ambient dust accumulation and debris slippage. Built with reinforced cold-drawn wire mesh and support channels conforming to ANSI MH26.2 standards.
25 Years of Precision Storage Engineering & Global Export Leadership
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has established itself as an engineering-driven primary manufacturer of industrial pallet racking, structural steel mezzanines, and high-density warehouse intralogistics systems worldwide.
Operating a modernized 30,000 m² automated production complex staffed by over 300 experienced fabrication specialists, mechanical engineers, and metallurgical technicians, HEDA provides complete end-to-end industrial storage supply chains. We serve warehouse developers, 3PL logistics giants, cold-storage operators, and trade distributors across Australia, New Zealand, Europe, North America, Southeast Asia, and the Pacific Islands.
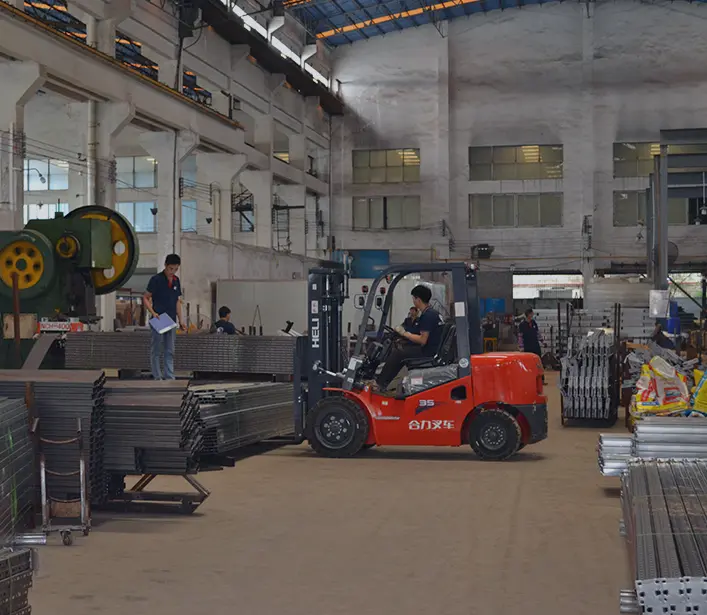
Dedicated continuous manufacturing of industrial racking systems.
Heavy machinery, roll-form mills, and automated stamping lines.
Direct partnerships with certified tier-1 steel mills (Baosteel/Ansteel).
Every container packed with ISPM-15 or steel stillage protection.
Future Procurement Trends in Industrial Storage (2025–2030)
Global supply chain directors and structural engineering consultants are moving away from ad-hoc spot buying. Strategic procurement now prioritizes total cost of ownership (TCO), supply chain agility, environmental life-cycle analysis, and multi-code compliance.
Total Landed Cost Modeling & Direct-From-Source ROI
Forward-thinking procurement teams no longer evaluate racking suppliers purely on factory ex-work unit rates. Comprehensive financial modeling calculates sea freight density, pallet position stuffing efficiency in 40ft High Cube containers, and preferential bilateral tariff schedules (such as ChAFTA and RCEP). Direct sourcing from Guangzhou Heda cuts local intermediary margins by 28% to 42% while retaining direct engineering communication.
Transition to Hybrid Pallet Staging & AS/RS Readiness
Warehouse planners are procuring static pallet racking designed to be "automation-ready." Upright profiles and beam connectors are engineered with ultra-tight deflection tolerances and pre-punched registration tracks to accommodate future retrofits of Autonomous Mobile Robots (AMRs), automated 4-way radio shuttles, or vertical automated storage systems without replacing structural columns.
Quarantine Resiliency & Biosecurity Strictness
Stringent import regulations by agencies like Australia's DAFF (Biosecurity) and New Zealand's MPI have made timber packaging a major operational liability during brown marmorated stink bug (BMSB) seasonal risk windows. Procurement standards are actively shifting toward certified all-steel transport stillages and strict ISPM-15 kiln-dried heat-treated dunnage to eliminate port holding penalties and costly fumigation delays.
State-of-the-Art Technological Advancements in Racking Design
The structural steel storage sector is experiencing an unprecedented engineering evolution driven by high-yield metallurgy, non-linear seismic simulation, and anti-corrosive nanotechnology coatings.
High-Yield Micro-Alloyed Metallurgy (Q355B vs. Q235B)
Modern cold-formed profile design utilizes fine-grain micro-alloyed structural steels that increase yield strength from 235 MPa up to 355 MPa without compromising cold-bending ductility. This enables a 15% reduction in dead weight while providing greater resistance to localized forklift strikes. Enhanced ductility also improves energy absorption during seismic cycles, ensuring racks absorb lateral forces safely.
Non-Linear Seismic Analysis & Dynamic Ductility
With seismic activity becoming a primary focus along the Pacific Rim (New Zealand, Chile, Japan, Western US), racking frameworks are engineered via advanced finite element analysis (FEA). We evaluate P-Delta second-order lateral displacement effects, beam-end connector moment rotational stiffness, and ground acceleration parameters (NZS 1170.5 and AS 4084:2023) using specialized heavy-duty baseplates and oversized concrete expansion anchors.
Nano-Composite & Hot-Dip Surface Protection
Cold chain operations operating down to -30°C and coastal facilities exposed to marine salt fog demand advanced corrosion resistance. HEDA implements an automated 8-stage pre-treatment wash involving zirconium phosphate conversion and nano-ceramic bonding, followed by 70–90 μm thermoset polyester powder coating. For exterior or high-humidity applications, continuous hot-dip galvanization (ISO 1461) delivers lasting cathodic rust protection.
Technical Comparison: Heavy-Duty Industrial Storage Architectures
| Storage System Architecture | Floor Area Utilization | SKU Selectivity | Stock Rotation | Load Capacity (Per Tier) | Recommended Industry Application |
|---|---|---|---|---|---|
| Selective Pallet Racking | 35% – 45% | 100% Direct | FIFO / LIFO | 1,000 – 4,500 kg | 3PL, FMCG, General Retail, Engineering Spare Parts |
| Push-Back Pallet Racking | 65% – 75% | Medium (Per Lane) | Strict LIFO | 1,000 – 1,500 kg | Cold Storage, Bulk Chemicals, Food Processing |
| Pallet / Carton Flow Racking | 70% – 85% | High (Per Lane) | Strict FIFO | 50 – 1,500 kg | Pharmaceuticals, Perishable Foods, E-commerce Fulfillment |
| Heavy Duty Cantilever Racking | 50% – 60% | 100% for Long Items | Selective | 500 – 3,000 kg/arm | Steel Tubes, Timber, Extrusions, Sheet Building Materials |
| Multi-Tier Mezzanine Floors | 100% – 200% Gain | 100% Manual Pick | Dynamic | 300 – 1,000 kg/m² | E-Commerce Picking Hubs, Garments, Automotive Parts |
Frequently Asked Questions by Industrial Sourcing Directors
Clear, definitive technical answers addressing engineering verification, international building code compliance, shipping logistics, and structural safety documentation.
How does HEDA Shelves ensure compliance with AS 4084, EN 15512, and ANSI MH16.1 standards?
Every industrial racking system designed and fabricated by Guangzhou Heda Shelves Co., Ltd. is engineered against verified finite element limit-state calculations. We provide complete structural submittal packages that detail:
- Full cold-formed upright and beam cross-sectional geometric properties (moment of inertia, section modulus, torsional warping constants).
- Experimental connector shear test curves and beam end-connector rotational stiffness ($K_b$).
- Comprehensive load application tables and safety plaques designed to comply with local regulatory mandates (such as Australian AS 4084:2023 or European EN 15512).
These calculations allow your local chartered professional engineer (CPEng/PE) to sign off, verify, and register the installation with local municipal building authorities without delay.
What steel grades are used, and do you supply Mill Test Certificates (MTC) with each shipment?
We source 100% prime structural steel coils directly from state-owned tier-1 steel mills, primarily Baosteel and Ansteel. We strictly utilize cold-rolled and hot-rolled structural steel grades Q235B (yield strength $f_y \ge 235 \text{ MPa}$) and high-strength Q355B (yield strength $f_y \ge 355 \text{ MPa}$).
Every production batch is accompanied by genuine EN 10204 Type 3.1 Mill Test Certificates (MTC) detailing complete chemical ladle analysis (Carbon, Silicon, Manganese, Phosphorus, Sulfur) and mechanical tensile and elongation test results. We retain complete traceability from raw master coil slit bands to the final finished frame assembly.
How do you handle seismic zone engineering for high-risk regions like New Zealand or the Pacific Rim?
For seismic-prone regions (such as New Zealand seismic hazard zones under NZS 1170.5 or California seismic classifications under CBC/IBC), our engineering department runs dynamic seismic response simulations. We analyze:
- The site's fundamental period, soil subsoil category (Class A through E), and seismic hazard coefficient ($Z$).
- Second-order P-delta effects and lateral brace stiffness in both down-aisle and cross-aisle orientations.
- Enhanced anchoring calculations: we integrate enlarged structural baseplates (up to 16mm thick) with multiple heavy-duty mechanical wedge anchors or epoxy chemical anchor studs.
We also supply reinforced double-column upright spliced assemblies and low-clearance heavy structural row spacers to ensure structural stability during seismic events.
What packaging precautions are taken to prevent shipping damage and meet biosecurity requirements?
Maritime transport involves high humidity, ocean transit motion, and strict biosecurity regulations. To address these demands:
- Biosecurity Compliance: We utilize all-steel packaging cradles and stillages, completely eliminating timber materials. If wood dunnage is requested, it is 100% heat-treated in strict accordance with ISPM-15, clearly IPPC-branded, and accompanied by formal Phytosanitary and Fumigation Certificates to prevent quarantine holds by authorities such as Australia's DAFF or New Zealand's MPI.
- Surface Finish Protection: Every bundle of uprights, step beams, and shelf levels is protected with corrugated corner guards, heavy stretch film wrapping, and heavy-duty polyester strapping to prevent metal-on-metal abrasion during sea transit.
What data do your structural engineers need to deliver a free 3D CAD warehouse layout?
To produce an optimized 3D CAD layout, bill of quantities (BOQ), and price quotation within 24 hours, our engineering team requires:
- Warehouse Dimensions: Architectural DWG or PDF showing building footprint, structural building columns, docks, overhead door swings, and clear roof height under purlins or sprinklers.
- Pallet & Load Specifications: Pallet dimension (L × W × H including cargo), total pallet weight (nominal & maximum), and bottom deck board layout.
- Forklift Capabilities: Forklift type (Counterbalance, Reach truck, VNA turret truck), minimum clear aisle width requirement, and maximum lift height.
- Operational Profile: Target SKU counts, desired rotation model (FIFO/LIFO), and any ambient, cold-storage, or hazardous material requirements.
What are the lead times for manufacturing and international ocean transit?
Standard fabrication lead time is typically 15 to 25 calendar days from signed shop drawing approvals and deposit receipt, depending on total project tonnage and custom color requirements. With our high-speed roll-forming lines producing up to 30,000 tons per month, we can fulfill fast-track, multi-container projects rapidly.
Ocean freight transit from our nearby export ports (Guangzhou Nansha, Shenzhen Yantian, or Shekou) averages 12 to 18 days to Australia/New Zealand, 18 to 25 days to the US West Coast, and 28 to 35 days to European main base ports.
Plan Your Next Warehouse Expansion with Certified Steel Racking
Contact our engineering design office directly. Share your building layout or storage targets, and our structural team will generate complete 2D/3D CAD layout proposals, pallet capacity analyses, and transparent factory-direct pricing within 24 hours.