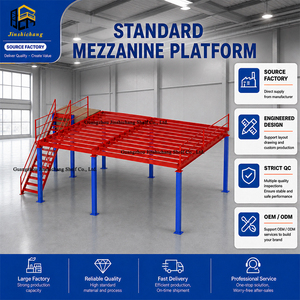
Customized Steel Mezzanine Floor for Warehouses
- Capacity: 300 - 1500 kg/m²
- Modular bolt-together structural steel
Designed, rolled, welded, and powder-coated in our Guangzhou manufacturing base to exact industrial parameters for international logistics, cold chains, and FMCG hubs.
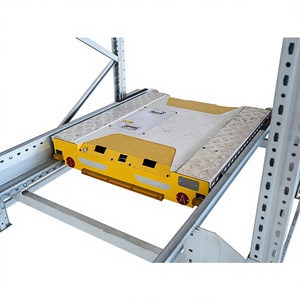
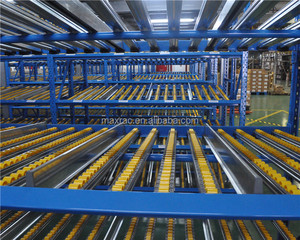

How inclined roller tracks, centrifugal brake systems, and First-In-First-Out (FIFO) mechanics eliminate forklift aisles while preventing load runaway.
Gravity pallet flow racks utilize gravity-fed wheel or roller lanes pitched at an engineered pitch—typically between 2.5% and 3.5% (approx. 1.5°–2°). Our technical department calculates this angle relative to pallet base morphology, total pallet weight (ranging from 500kg up to 1800kg per position), and bottom runner deflection under real warehouse temperature profiles.
Unchecked pallet acceleration is the leading cause of structural impact failures in deep-lane systems. HEDA integrates heavy-duty direct-drive centrifugal brake rollers at measured intervals. These internal eddy-current or friction brakes cap downward velocity at a safe 0.25 to 0.3 meters per second, ensuring zero impact upon contact with the discharge separator.
When lanes extend 5 to 20 pallets deep, the cumulative back-pressure on the extraction face can exceed several metric tons, making forklift extraction perilous. We manufacture integrated mechanical separators that isolate the front discharge pallet from rear pallets until the front pallet is completely picked, reducing operator stress and forklift mast wear.
How structural engineering, automation synergy, and carbon compliance are transforming international wholesale procurement from Chinese factories.
Traditional standalone gravity racks are evolving into high-throughput dynamic buffer bays interfacing directly with Automated Guided Vehicles (AGVs) and Autonomous Mobile Robots (AMRs). Global distribution centers increasingly procure gravity tracks calibrated with magnetic sensors and optical reflection targets, allowing robotic forklifts to pick and place pallets without human intervention.
Procurement directors in Oceania, North America, and Europe now demand full structural verification aligning with AS 4084, NZS 1170.5, RMI MH16.1, and FEM standards. HEDA Shelves addresses this by providing full FEA (Finite Element Analysis) stress simulations and certified structural cross-sections with every wholesale batch, guaranteeing compliance with local building authorities.
Cold storage running costs have accelerated the demand for low-temperature ductile steels such as Q355D and Q355E that resist low-temperature embrittlement down to -30°C. Coupled with eco-friendly TGIC-free electrostatic coatings and zinc-rich pre-treatments, modern racking profiles maintain impact integrity despite constant freezer thermal cycling.
Direct factory ownership, advanced automated production cells, and comprehensive global engineering support from South China.
Prime cold-rolled steel coils procured directly from top-tier Chinese state mills (Baosteel/Ansteel) with standard mill test certificates (MTC) ensuring yield strengths up to 355 MPa.
Continuous multi-station roll-forming lines precision punch tear-drop, diamond, or hex hole patterns with ±0.2mm tolerance, eliminating internal stress concentrations in upright posts.
A 9-stage continuous pre-treatment system involving degreasing, hot acid pickling, rust removal, and automated zinc-phosphating guarantees exceptional powder adhesion.
Fully automated Swiss Gema powder coating booths cure non-toxic thermoset epoxy coatings at 180°C–200°C, providing impact-resistant finishes rated for harsh logistics conditions.
Critical considerations regarding steel gauge, shipping calculations, customs clearance, and engineering sign-off.
Send us your warehouse dimensions, ceiling heights, pallet dimensions, and handling requirements. Our engineering team returns full 2D CAD layouts and 3D system simulations within 24 hours.