Heavy-Duty Industrial Shelving & Pallet Racking Components
Explore our certified range of modular structural components, automated conveyor assemblies, high-density push-back carts, and wire-mesh decking engineered to international seismic and loading standards.
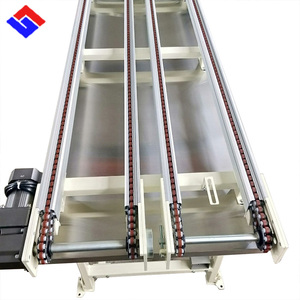
Aluminum Rail Motorized Duplex Chain Pallet Flow Industrial Assembly Double Speed Chain Conveyor
Integrated heavy-duty extruded aluminum guide rails with double-pitch engineered roller chains for smooth industrial assembly lines and automated material feeding.
- Payload: Up to 1,500 kg/m
- Extruded AL6063-T5 Structural Rails
- High Wear-Resistant Nylon/Steel Rollers
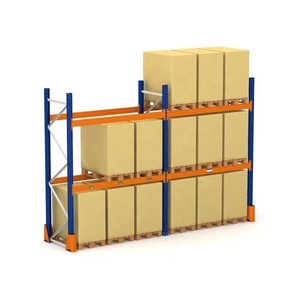
Professional Heavy Duty Pallet Racking System Warehouse Shelves
Standard-setting selective uprights and step beams engineered for maximum volumetric efficiency in distribution hubs handling multi-SKU storage.
- Capacity: 1,000–4,500 kg / level
- 50mm / 75mm Pitch Adjustability
- Certified Q235B Cold-Rolled Steel
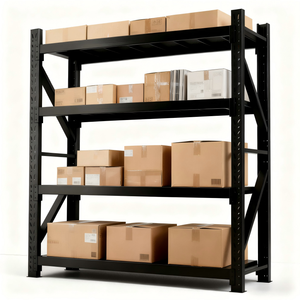
Adjustable Industrial Warehouse Stacking Racks & Shelves Cargo & Storage Equipment Multi Tier Storage Rack Shelving Units
High-versatility boltless industrial shelving modules configured for multi-tier mezzanine floors, pick-module towers, and automated parts consolidation.
- Loading: 300–800 kg / shelf tier
- Interlocking Drop-In Steel Decking
- Catwalk & Stairway Integrated
Storage Stacking Racks Pallet Steel Metal Shelves Garage Warehouse Racking
Portable, nestable post racks providing flexible buffer storage during peak seasonal cycles without requiring permanent anchor bolts.
- 4-High Safe Stacking Capability
- 4-Way Forklift Entry Base Structure
- Hot-Dip Galvanized / Powder Coated
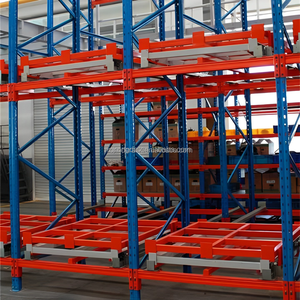
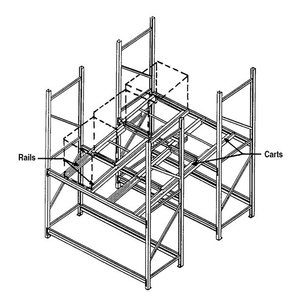
Warehouse Storage Adjustable Push Back Pallet Racking Manufacturer Steel Rack
Precision-engineered inclined nested carriage design storing 2 to 6 pallets deep. Maximizes cubic density while dedicating separate pick faces per lane.
- 2 to 6 Pallet Deep Channel Capacity
- Low-Profile Heavy Flange Carts
- Integrated Friction Anti-Derail Stops
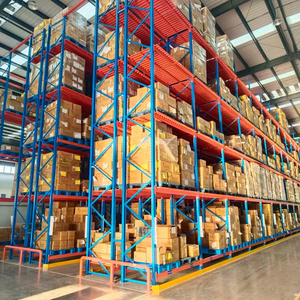
3000kg Capacity Pallet Racking System for Manufacturing Workshop Bolted Connection Load Accept OEM & ODM
Reinforced bolted upright truss connections designed for heavy industrial die storage, tool cribs, and production machinery buffer areas.
- Point Load: 3,000 kg / pallet space
- High-Tensile 8.8 Grade Structural Bolts
- Heavy Column Upright Protectors
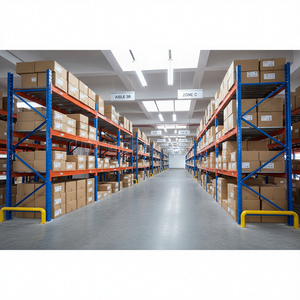
Wholesale Warehouse Racking System Heavy Duty Metal Iron Shelving Warehouse Storage Push Back Push Back Pallet Racking Systems
High-throughput wholesale racking system utilizing gravity flow carts to save up to 60% aisle space compared to traditional selective racking arrangements.
- Continuous Cold-Formed Steel Rails
- Sealed Bearing High-Velocity Rollers
- Cold Room Anti-Freeze Lubrication
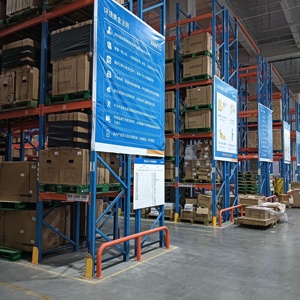
Heavy Duty Selective Pallet Rack with Custom Wire Mesh Decking High Load Steel Adjustable Warehouse Pallet Racking System
Safety-focused selective pallet rack frames fitted with custom welded wire mesh panels and heavy channel supports, fully compliant with international fire sprinkler codes.
- NFPA 13 Fire Sprinkler Penetration
- U-Channel Flanged Waterfall Design
- Rust-Proof Zinc Galvanized Surface
Engineering Blueprint: Anatomy of High-Yield Industrial Shelving Components
Industrial storage structures operate under continuous static loads, seismic vibrations, and repetitive dynamic impacts from automated material handling equipment. Choosing components fabricated under strict metallurgical controls ensures lifecycle reliability, seismic ductility, and full regulatory approval.
1. Advanced Roll-Formed Upright Column Geometry
The structural backbone of any high-bay shelving or racking installation is the upright frame column. Unlike standard open structural channels, our manufacturing facility utilizes a closed 9-bend to 13-bend cold-roll profile engineered from certified high-strength structural strip steel (yielding a minimum tensile strength of 355 to 490 MPa). Each additional cold-formed bend enhances the section modulus ($W_x, W_y$) and increases resistance against torsional-flexural buckling under axial compression loads.
Upright perforations (pitch-spaced at 50mm, 75mm, or 76.2mm intervals) are produced via automated high-speed multi-stage CNC stamping dies before cold roll forming. This guarantees hole center-to-center pitch tolerances within ±0.15mm across a continuous 12-meter profile. Tear-drop, diamond, and hexagonal keyhole slots are optimized to prevent localized stress risers, providing positive geometric interlock with beam connector claws.
2. Step Beams, Box Beams & Interlocking Connector Physics
Horizontal load support depends on seam-welded continuous box beams or stepped profile channels. Our dual C-section interlocked and robotic continuous seam-welded box beams provide symmetrical flexural stiffness along the vertical and horizontal axes. This eliminates horizontal bowing under heavy pallet dead loads. The beam end connectors feature 3-tooth or 4-tooth robotic-welded stamped high-tensile brackets.
Every connector is equipped with an automated spring-steel safety locking pin that withstands an upward dislodgement shear force greater than 10 kN (well above the minimum requirements stipulated by AS 4084 and FEM 10.2.02). This prevents accidental beam dislodgement caused by forklift mast operator errors during pallet lifting.
Component Mechanical Property & Standard Comparison
| Component Name | Material Grade | Yield Strength ($F_y$) | Tensile Strength ($R_m$) | Standard Compliance | Primary Surface Finish |
|---|---|---|---|---|---|
| Heavy Duty Upright Profiles | Q355B / SS490 / S355JR | ≥ 355 MPa | 470–630 MPa | AS 4084 / EN 15512 / RMI MH16.1 | Thermoset Epoxy Powder (60–80µm) |
| Roll-Formed Box / Step Beams | Q235B / S235JR | ≥ 235 MPa | 370–500 MPa | EN 10025 / ASTM A36 | High-Visibility Safety Orange / Yellow |
| Seismic Baseplates & Anchors | Q235B / High Tensile Steel | ≥ 235 MPa | 400–550 MPa | NZS 1170.5 / ACI 318 Annex D | Hot-Dip Galvanized / Powder Coated |
| Wire Mesh Decking & Dividers | Drawn Low-Carbon Wire (Q195) | ≥ 295 MPa | ≥ 450 MPa | NFPA 13 Fire Sprinkler Standard | Electro-Zinc Galvanized / Hot-Dip Galv |
| Push-Back Nested Carriages | Structural Steel Hollow Section | ≥ 235 MPa | 370–500 MPa | ISO 9001:2015 Monitored QC | Impact Polyurethane Coated Rollers |
Future Procurement Trends in Industrial Storage Components (2025–2030)
How supply chain leaders, warehouse contractors, and procurement executives are adapting their sourcing strategies to navigate automation integration, environmental certifications, and localized regulatory compliance.
1. Rise of Automation-Ready Modular Component Tolerances
With the rapid adoption of Autonomous Mobile Robots (AMRs), Automated Guided Vehicles (AGVs), and stacker cranes, traditional manual racking tolerances are becoming obsolete. Sourcing criteria are shifting toward millimeter-precise component fabrication (deflection limits capped at $L/350$ vs standard $L/200$) to guarantee optical sensor alignment, predictable laser guidance reflection, and collision-free high-speed shuttle transit.
2. Decarbonized Steel & Eco-Certified Surface Chemistries
Global carbon-border adjustment mechanisms (such as the EU CBAM) are compelling Tier-1 warehouse developers to demand low-carbon electric-arc-furnace (EAF) steel sourcing and RoHS-compliant finishing. Procurement workflows now evaluate factory pre-treatment chemistries, favouring non-toxic zirconium and silane nano-conversion coatings that reduce energy consumption by up to 35% compared to conventional hot phosphate immersion baths.
3. Direct-from-Factory Containerized Stillage Logistics
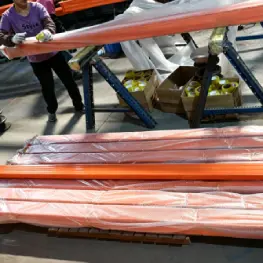
To avoid secondary distributor markups and inland transshipment damage, institutional buyers are ordering pre-sorted, containerized racking kits packed on reusable ISPM-15 compliant steel or heat-treated timber stillages. Direct factory packaging models allow offloading directly onto installation slabs, eliminating pallet damage and decreasing installation crew assembly timelines by up to 40%.
Technological Innovations Driving Modern Component Fabrication
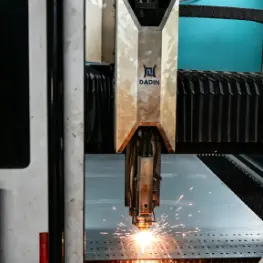
Precision racking manufacturing is an exact science. Behind our high-output facility lies an ecosystem of automated production lines, laser profile processing, and tight quality-assurance loops.
1. 24-Station CNC Continuous Cold Roll-Forming
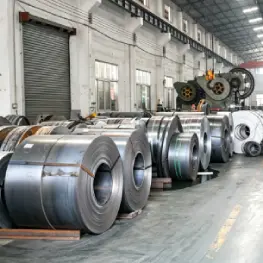
Our facility runs automated, multi-roller cold-bending lines that transition flat steel slit coils into finished upright columns in a single, controlled pass. Gradual step-by-step roller forming eliminates micro-cracking and maintains homogeneous wall thickness throughout profile bends, preserving internal molecular grain alignment.
2. 6-Axis Robotic Tandem Welding Cells
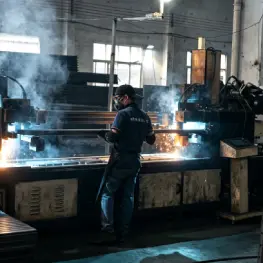
Beam end-connector weld joints are fused using Japanese OTC/Fanuc multi-axis robotic welding cells with automated seam tracking. Consistent penetration, zero spatter, and continuous gas-shielded (Ar/CO₂ mix) welding ensure beam brackets withstand catastrophic dynamic impact loads without shear failure.
3. 12-Stage Automated Pre-Treatment & Powder Coating
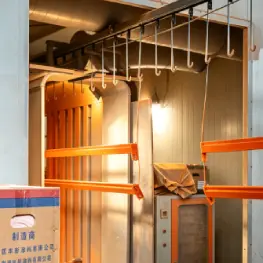
Prior to painting, steel profiles traverse a 12-stage tunnel containing degreasing, ultrasonic water baths, hot pickling, and zirconium-based nano-passivation. Electrostatic automated spray booths apply pure polyester or epoxy-hybrid powders baked at 200°C, producing an anti-scratch surface verified to exceed 500 hours of ASTM B117 salt spray exposure.
10-Step Quality Assurance & Fabrication Process
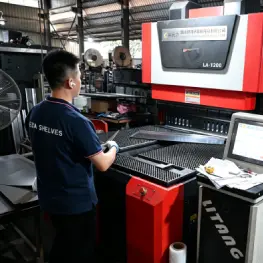
Every component leaving our factory floor passes through an unbroken chain of custody, metallurgical spectroscopy, automated dimensional checks, and load verification.
Guangzhou HEDA Shelves: 25-Year Engineering Heritage
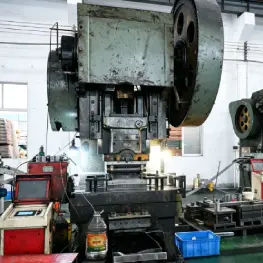
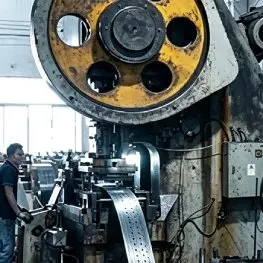
Established in 2001, Guangzhou Heda Shelves Co., Ltd. has grown from a specialized metal stamping workshop into a 30,000 square meter intelligent manufacturing base with over 300 experienced engineers and technicians.
Full OEM & ODM Private Label Capabilities
We partner with material handling system integrators, regional shelving distributors, and racking brands worldwide. Our engineering division produces fully branded parts, custom-color powder coating, custom punch slot geometries, and private-label packaging to integrate seamlessly into existing product lines.
Turnkey Engineering & 3D CAD/FEA Modeling
Do not risk structural undersizing. Supply your site layout, slab compressive data, and pallet parameters, and our engineering department will deliver a comprehensive 3D CAD proposal and Finite Element Analysis (FEA) structural calculation report within 24 to 48 hours, free of charge.
Oceania & Global Compliance Track Record
With extensive experience designing under Australian AS 4084, New Zealand NZS 1170.5 (seismic bracing), European FEM 10.2.02, and American RMI standards, we provide complete engineering certification packs for straightforward sign-off by local structural certifiers and municipal building authorities.

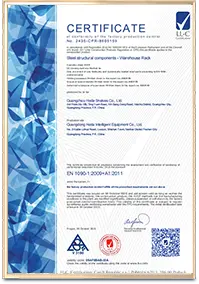
CE Certified Factory
Certificate: No. 2435-CPR-8605159 European Conformity

ISO 9001:2015 Quality
Cert No: 18624Q00169R0M Valid Through June 2027

RoHS Certified Eco-Coat
Hazardous Substances Controlled & Lead-Free Powder
Independent Load Audits
Certified Third-Party Static & Dynamic Destruction Tests
Industrial Shelving Components: Frequently Asked Questions
Critical technical insights addressing structural steel specifications, seismic compliance, biosecurity import requirements, and volume manufacturing lead times.