Industrial Pallet Racking & Heavy-Duty Storage Configurations
Explore our factory-engineered range of modular heavy-duty racking systems, structural steel frameworks, and gravity flow setups customized to high-throughput warehousing.
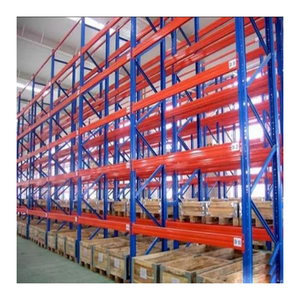
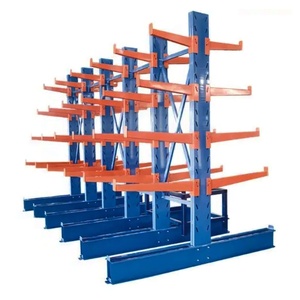
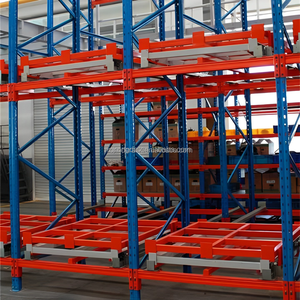
Industrial Authority in Drive-In Pallet Racking Architecture
As a direct-from-source manufacturer holding CE Certification No. 2435-CPR-8605159 and ISO 9001:2015 accreditation, Guangzhou Heda Shelves Co., Ltd. delivers structural integrity designed around international seismic codes, high pallet density requirements, and cold chain parameters.
Structural Steel Integrity (Q235B / Q355B)
We source prime, high-tensile cold-rolled steel coils with documented mill certificates. Our drive-in uprights, cantilever arms, and load-bearing pallet rails undergo finite element method (FEM) analysis to prevent buckling under multi-tiered asymmetric loads.
Bespoke CAD/3D Layout & Seismic Engineering
From Australian standard 1165 × 1165 mm timber pallets to Euro (1200 × 800 mm) configurations, our in-house engineering team provides free 3D CAD stress simulations and seismic tie-back calculations tailored to local safety regulations.
Corrosion Shielding & Cold Storage Metallurgy
Automated 10-stage pre-treatment, including multi-stage pickling, phosphating, and electrostatic powder coating (60-80μm). For deep-freeze environments (-30°C) and marine shipping climates, we provide hot-dip galvanization adhering to EN ISO 1461 standards.
Turnkey OEM/ODM Global Distributor Support
We empower regional rack suppliers, material handling integrators, and storage system distributors worldwide with custom punch tooling, proprietary connector patterns, branded load rating plaques, and ISPM-15 export-compliant timber packaging.
Certified Compliance & Traceable Quality
Every fabrication batch includes full inspection documentation, dimensional tolerance audits (±0.5mm), and material yield testing. All load ratings conform to AS 4084, ISO 9001:2015, and RoHS chemical baseline regulations.
Full Logistics Integration & Port Access
Positioned in Guangzhou with seamless access to South China container ports. We coordinate direct breakbulk and 40HQ container shipments worldwide, guaranteeing rapid transit to Oceania, Southeast Asia, North America, and Europe.
Drive-In Racking Architecture: Volumetric Density Analysis
Drive-In systems optimize volumetric storage space by up to 75% compared to conventional selective configurations. Below is an engineering comparison matrix for procurement teams evaluating high-density storage frameworks.
| Storage Matrix Feature | Drive-In Pallet Racking | Push Back Cart Racking | Radio Shuttle Racking | Standard Selective Rack |
|---|---|---|---|---|
| Stock Rotation Logic | LIFO (Last-In, First-Out) | LIFO (Last-In, First-Out) | FIFO or LIFO Automated | 100% Selective Access |
| Volumetric Space Efficiency | Very High (Up to 75% Floor Yield) | High (Up to 60% Floor Yield) | Maximum (Up to 85% Floor Yield) | Standard (35-40% Floor Yield) |
| Forklift Entry Requirement | Drives Directly Inside Lanes | Operates Strictly in Main Aisle | Operates Strictly at Lane Face | Requires Dedicated Aisle Space |
| Standard Lane Depth | 2 to 10 Pallets Deep | 2 to 6 Pallets Deep | Up to 40 Pallets Deep | 1 to 2 Pallets Deep |
| Optimal Use Case Profile | Cold Storage, Homogenous SKUs | Medium SKU Variety, Buffer Storage | Massive Cold Warehouses, FMCG | High SKU Variance, Multi-Client 3PL |
| Capital Expenditure Index | Cost-Effective / Highly Durable | Moderate (Cart / Rail Mechanisms) | Higher Initial Automation Outlay | Lowest Base Initial Cost |
Future Procurement Trends & Engineering Evolutions
Global supply chains demand higher seismic resilience, lower lifecycle maintenance overheads, and seamless hybrid automation compatibilities.
1. High-Yield Cold-Formed Metallurgy
Procurement teams are shifting away from heavy hot-rolled channels toward ultra-high-strength, cold-formed steel sections (e.g., Q355B and high-grade galvanized coils). This reduces deadweight loads on warehouse slabs by up to 18% while enhancing dynamic elastic limit recovery during forklift impacts.
2. Cold Chain Total Cost of Ownership (TCO)
With global cold-storage power expenditures climbing, drive-in pallet racking remains the benchmark for refrigerated facilities. Maximizing thermal envelope utilization by reducing aisle volume directly lowers cubic refrigeration costs, providing rapid payback on capital expenditure.
3. Hybrid AGV & Narrow-Aisle Convergence
Modern drive-in structures are increasingly engineered with floor-mounted laser guidance channels, entry funnels, and reinforced upright bull-noses. This allows automated guided vehicles (AGVs) and reach trucks to enter lanes without human operator collision risks.
10-Stage Heavy-Duty Manufacturing Workflow
Our ISO 9001 certified production lines turn raw structural steel into precision components, guaranteeing tight tolerances and maximum safety margins.
Raw Steel Inspection
Strict spectroscopy and yield-strength verification of prime Q235B/Q355B coils before entering the uncoiler.
Precision Slitting & Cutting
CNC slitting lines ensure exact web and flange dimensions with clean edges ready for profile rolling.
Automated CNC Punching
Continuous hydraulic pitch punching ensuring 50mm / 75mm hole alignment precision along columns.
Multi-Roll Profile Cold Bending
18 to 24-station rolling mills form omega upright profiles with zero micro-fracturing along bend radiuses.
Continuous Roll Forming
Heavy-duty pallet support rails and top tie-beams precision-rolled to millimeter-level linear tolerances.
Robotic MIG Welding
Automated multi-axis robotic welders bond beam end connectors and heavy footplates with uniform penetration.
Shot Blasting & Polishing
Removal of mill scale, surface contaminants, and weld spatter to achieve optimal Sa 2.5 surface roughness.
Pickling & Phosphating
Immersion pre-treatment tanks create a dense chemical conversion coating for long-term corrosion prevention.
Electrostatic Powder Coating
Automatic GEMA electrostatic spray booths curing durable thermosetting polyester powder at 200°C.
Quality Audit & Packing
Dry film thickness (DFT) checks, cross-hatch adhesion testing, and steel-stillage packing for export transit.
Frequently Asked Questions by Industrial Buyers
Key engineering, compliance, and supply chain considerations when procuring drive-in and heavy-duty storage racking systems internationally.
How do Drive-In racking designs achieve structural stability without regular cross beams?
Because forklifts enter storage lanes directly, traditional intermediate shelf beams are eliminated. Structural rigidity is achieved using heavy-duty top tie beams, horizontal top-bracing frames, rear vertical X-bracing, and rigid upright-to-rail cantilever brackets engineered to absorb dynamic sway and asymmetric loads.
What documentation is provided for local building permit compliance?
We supply full structural engineering documentation packs including 3D CAD layouts, material mill certificates, steel section properties, deflection calculations, and load capacity tables referencing AS 4084, FEM, or ANSI/RMI MH16.1 guidelines for your local certifier's review.
How does HEDA prevent forklift damage inside Drive-In rack lanes?
We integrate floor-mounted steel guide rails running along the entire lane depth to center forklift wheels automatically. Additionally, we provide heavy-gauge wraparound column protectors, anchor reinforcements, and flared guide funnels at each lane entrance to safeguard uprights from strikes.
What is the typical lead time and shipping turnaround for global projects?
Standard OEM manufacturing lead time is 15 to 25 business days depending on volume and powder finish requirements. Ocean freight transit from Guangzhou ports to major international terminals typically ranges from 12 to 28 days, fully supported by export customs clearance documentation.
Can Drive-In racking be installed in sub-zero freezer cold storage?
Yes. We use specialized fine-grain structural steels that maintain impact toughness and ductility down to -30°C without cold embrittlement. Powder coatings are formulated for extreme thermal cycling, or components can be hot-dip galvanized to eliminate moisture condensation peeling.
What essential input data is required to generate an accurate layout quotation?
Please share your warehouse architectural DWG/PDF (clear eaves height, column spacing, floor capacity), pallet dimensions (W × D × H including overhang), maximum pallet gross weight, forklift make/model with mast lift height, and operating temperature range.
Accelerate Your Storage Capacity with an Engineered Layout
Connect with our technical engineering department today for free 2D/3D CAD layouts, structural calculations, and direct-from-factory volume quotes tailored to your exact facility dimensions.
Inquire Now