Bathroom Wall-Mounted Floating Decorative Partition Storage Rack
Precision cold-rolled light industrial steel framework designed for multi-tier retail stockroom staging and modular partition utility.
Engineered for direct port dispatch across Australia, New Zealand, Europe, and the Americas. Built to exceed international yield thresholds with full structural certification.
Precision cold-rolled light industrial steel framework designed for multi-tier retail stockroom staging and modular partition utility.
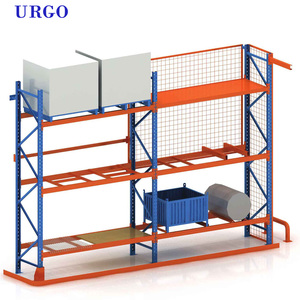
Ultra-high density footprint engineered for high-bay articulated turret trucks, maximizing vertical cube storage with bottom-mounted guide rails.
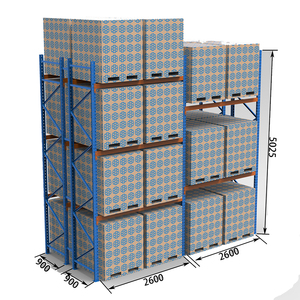
Heavy duty structural steel box-beams with robotic seam welds, providing 2,000kg UDL capacity per bay pair for back-to-back warehouse runs.
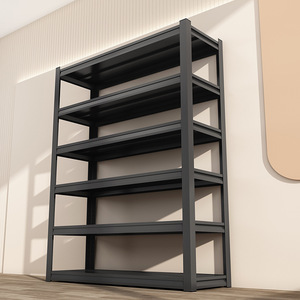
Corrosion-resistant structural alloy overhead system designed for specialized cold-chain staging and hygienic cleanroom warehousing.
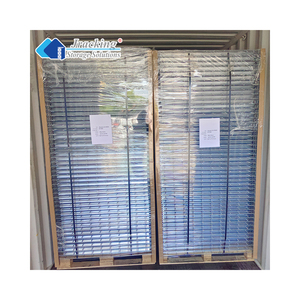
Heavy-gauge welded wire decking panels engineered to enhance NFPA/ESFR sprinkler penetration while eliminating point-load deflection.
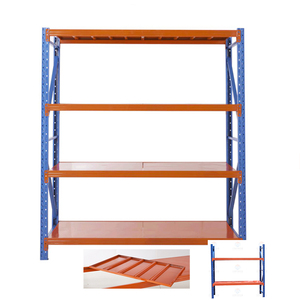
Versatile intermediate pick-face solution utilizing step-beam frames with drop-in steel shelves for high-density automotive and carton distribution.
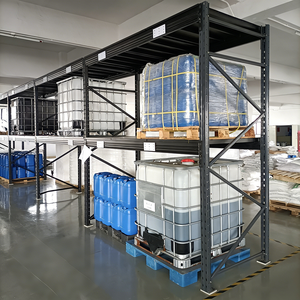
Integrated structural upright profiles equipped with wrapped-steel impact column protectors to mitigate forklift collision shear stresses.
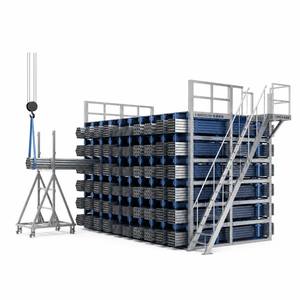
Specialized structural cradle rack designed for bar stock, conduit, and piping extrusion packs with ISO 9001 and CE certified metallurgical integrity.
Key performance benchmarks for global supply chain directors, distribution architects, and structural safety auditors.
In modern high-velocity distribution environments, heavy-duty industrial pallet racking is not merely static steel storage; it serves as the foundational structural backbone that determines logistical throughput velocity, floor space capitalization, and worker safety. International procurement managers tasked with identifying the top 10 heavy duty industrial pallet racks exporters face an increasingly intricate regulatory and engineering landscape. Variations in seismic engineering criteria, mill-certified steel yield strengths (such as Q235B versus Q355B), automated punching tolerances, and protective anti-corrosive coatings dictate long-term total cost of ownership (TCO).
A premier industrial racking exporter must operate beyond basic metal fabrication. Leading exporters distinguish themselves through advanced finite element analysis (FEA), in-house roll-forming production lines, robotic precision welding, and comprehensive adherence to global standards—including Australia's rigorous AS 4084:2023, Europe's EN 15512:2020, and America's RMI (ANSI MH16.1). When sourcing across international borders, structural engineering teams require transparent yield calculations, comprehensive seismic base-plate data packs, and biosecurity-compliant container packing methodologies to prevent port rejections and site erection delays.
Exporters of high caliber enforce direct mill traceability. Premium upright profiles are cold-rolled from high-tensile structural coil with certified chemical limits, eliminating micro-fracturing along bend radiuses under extreme static or dynamic impact loadings.
Global logistics hubs situated along the Pacific Rim demand advanced dynamic displacement analysis. Top exporters provide site-specific seismic engineering packs featuring enlarged base plates, reinforced back-to-back row spacers, and localized anchor sheer ratings.
Modern pallet rack layouts balance selective accessibility with volumetric density. From Very Narrow Aisle (VNA) systems maximizing vertical cube utility to automated Radio Shuttle channels, system selection dictates fulfillment operational expenditure.
How intelligent warehouse automation, eco-resilient coatings, and digitized engineering are transforming high-capacity steel storage systems worldwide.
Industrial warehousing is rapidly shifting away from manual forklift operations toward automated pallet storage and retrieval systems (AS/RS) and multi-directional radio shuttles. Procurement criteria now demand manufacturing tolerances within fractions of a millimeter. Uprights and guide tracks must maintain absolute plumbness over 24-meter elevations to avoid automated optical sensor drift and shuttle jams.
With exponential expansion in refrigerated food storage and tropical coastal logistics centers across Oceania and Southeast Asia, conventional enamel paint finishes are obsolete. Sourcing strategies mandate pre-treatment phosphating, thick electrostatic thermoset powder coatings, or batch hot-dip galvanizing exceeding ASTM A123 standards to combat aggressive chemical vapors and condensing freezer freeze-thaw cycles.
Next-generation industrial pallet racks are engineered directly as Digital Twin assets within Building Information Modeling (BIM) workflows. Future procurement models require exporters to deliver native IFC and Revit families loaded with precise structural properties, empowering warehouse operators to deploy real-time IoT strain gauges and impact sensors to monitor deflection after accidental fork-truck collisions.
Over 25 years of specialized export excellence backed by verifiable certifications, extensive manufacturing infrastructure, and comprehensive global logistic frameworks.
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. has grown into an international manufacturing force spanning over 30,000 square meters of dedicated production space. With an active workforce comprising over 300 experienced engineers, structural modelers, and production specialists, Heda maintains a robust monthly output capacity surpassing 30,000 tons. Having engineered and dispatched more than 10,000 turnkey warehouse installations globally, our factory serves as the primary original equipment manufacturer (OEM) and original design manufacturer (ODM) for leading rack distributors and enterprise operators across Australia, New Zealand, Europe, and the Americas.
Our operational ethos is grounded in engineering rigor and transparent compliance. We proudly publish our accredited certifications for third-party institutional verification, including CE Certification (No. 2435-CPR-8605159), ISO 9001:2015 Quality Management System (No. 18624Q00169R0M), and RoHS material compliance. Every container leave our bays with full component numbering, mill test certificates, seismic calculations, and export-grade biosecurity packing designed to sail through DAFF (Australia) and MPI (New Zealand) border clearances without fumigation delays.
Analysis of your facility floor plan, clear ceiling heights, slab psi ratings, slab flatness specs, and forklift mast travel profiles.
Full 3D rendering and structural CAD layout optimized for aisle clearances, flue spaces, NFPA fire compliance, and maximum pallet yield.
Automated punching, cold roll-forming, robotic welding, acid-wash pickling, and thermoset powder coating under strict ISO 9001 quality audits.
Containerized stillage bundling, complete export paperwork, and remote or on-site engineering installation guidance.
Clear, engineering-backed answers addressing structural standards, seismic design, shipping timelines, and compliance.
Consult with our engineering team today. Provide your facility layout, clear ceiling heights, and pallet specifications to receive an engineered 3D CAD proposal and factory-direct quotation.
Send an Inquiry