Engineering Principles of High-Capacity Metal Pallet Racking
Modern automated logistics hubs and multi-tiered fulfillment facilities demand structural certainty. Sourcing structural steel storage racks from a qualified Chinese industrial manufacturer requires technical evaluation across cold-formed steel tensile yield strengths, dynamic beam deflection thresholds, seismic bracing dynamics, and anti-corrosion chemical passivation.
Precision-Engineered Industrial Pallet Storage Systems
Customized cold-rolled Q235B and Q355B high-grade steel configurations manufactured for selective accessibility, extreme gravity density, and automated shuttle integration.
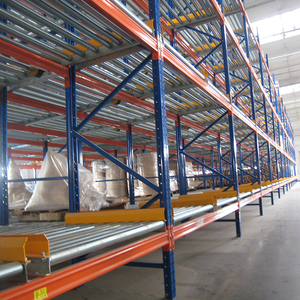
High Efficient Steel Selective Gravity Pallet Racks with High Storage Capacity
- Load: Up to 1,500 kg per pallet position
- Rotation: First-In, First-Out (FIFO) gravity roller
- Steel: High-tensile Q235B cold-rolled profiles
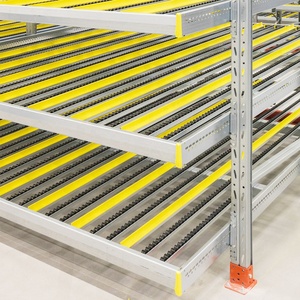
Warehouse Storage Gravity Carton Flow Rack for Box & Split-Case Handling
- Tracks: Integrated high-density aluminum roller beds
- Ergonomics: Angled loading and pick trays
- Efficiency: Eliminates up to 60% of picker transit time
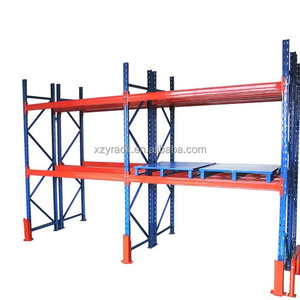
Pallet Rack Steel Feet Base Plates for Pallet Racking Box Beam Columns
- Fabrication: Heavy-gauge stamped structural plate
- Anchoring: Multi-hole seismic anchoring layout
- Finish: Zinc electro-galvanized or hot-dip galvanized
Industrial Warehouse Gravity Flow Racking Shelves Pallet Storage Rack
- Speed Control: Continuous centrifugal braking rollers
- Safety: Pallet separator mechanism at discharge end
- Suitability: Beverage, dairy, and cold-store operations
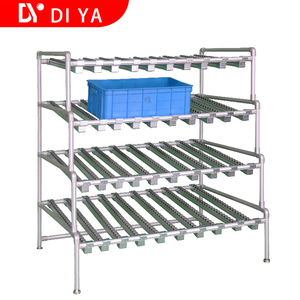
Diya Heavy Duty Aluminium FIFO Pipe Rack for Workshop & Assembly Storage
- Structure: Modular high-strength anodized aluminum tubing
- Customization: Fast reconfigurable lean line-side feed
- Durability: Zero rust, low weight, cleanroom certified
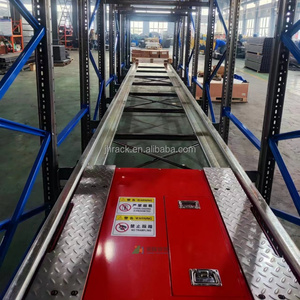
Automated Warehouse AS/RS Pallet Shuttle Deep-Lane Storage System
- Shuttle Drive: Wireless 24V/48V high-cycle lithium runner
- Utilization: Up to 90% floor-to-ceiling cubic density
- Modes: Dual operational support for FIFO and LIFO lanes
Customized Industrial Heavy Duty Pallet Rack System Warehouse Storage
- Section: Dual-rib box beams with 3 or 4-hook connectors
- Capacity: 1,000 kg to 5,000 kg per beam level
- Engineering: Custom designed to AS 4084 / FEM standards
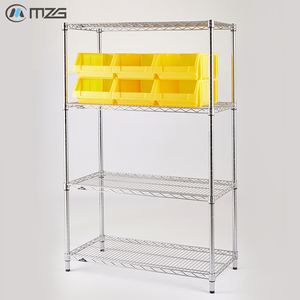
Bulk Heavy Duty Industrial Multi-Layer Metal Wire Decking & Shelving
- Safety: Enhanced sprinkler penetration & smoke clearance
- Reinforcement: Inverted welded channel wire deck ribs
- Finish: Anti-rust chrome plated or epoxy powder coat
Emerging Trends Shaping Industrial Pallet Rack Procurement (2025–2030)
Procurement teams and supply chain engineers are no longer purchasing passive steel framing strictly on raw tonnage price. The transition toward high-density automation, seismic compliance, and total lifecycle sustainability is redefining manufacturing specifications across tier-one facilities.
Hybrid Automation & Shuttle-First Architecture
Traditional wide-aisle selective configurations are rapidly giving way to hybrid shuttle-fed racking channels. Sourcing trends show a 42% compound growth rate in automated pallet runners that reduce forklift drive paths, suppress building footprint requirements, and protect structural uprights from constant mast collisions.
Reduced Labor & Zero Impact GeometrySeismic Engineering & Global Standard Harmonization
International tier-one logistics developers require verified calculations across regional regulatory codes: Australian AS 4084-2023, European EN 15512/FEM 10.2.02, and American RMI MH16.1. Factories must provide finite-element analysis (FEA) validating base plate yield, anchoring shear parameters, and upright torsional resistance.
FEA Validated Static & Dynamic TestingTotal Cost of Ownership (TCO) Over Nominal Price
Experienced logistics directors reject ultra-thin raw steel sections that warp under standard L/200 beam deflection loads. Procurement criteria have shifted directly to high-yield Q355B cold-rolled profiles, electrostatic powder coats resistant to 500-hour salt-spray tests, and biosecurity-compliant containerized packaging.
500-Hour Salt Spray & Low-VOC Thermoset FinishesStructural Metal Pallet Racking: System Architectural Matrix
Compare mechanical properties, aisle configurations, SKU selectivity coefficients, and typical operational thresholds across core pallet rack formats manufactured in our factory.
| Racking System Type | SKU Selectivity | Cubic Space Efficiency | Typical Load Rating | Structural Profile Standard | Target Sector Application |
|---|---|---|---|---|---|
| Selective Pallet Racking | 100% Direct | 40% – 50% | 1,000 – 4,500 kg / level | Q235B Cold-Rolled Box Beam | 3PL FMCG, General Distribution |
| Gravity Pallet Flow (FIFO) | Lane Dependent | 75% – 85% | 1,500 kg / pallet | Brake Roller Beds + Uprights | Food, Beverage, Cold Storage |
| Drive-In / Drive-Through | LIFO / FIFO | 65% – 75% | 1,000 – 1,800 kg / pallet | Heavy Cantilever Saddle Brackets | Homogeneous Bulk Stockrooms |
| Automated Radio Shuttle | High (Automated) | 85% – 92% | 2,000 kg / carrier cycle | Custom Cold-Formed Shuttle Rails | Deep Freeze, Pharmaceutical Hubs |
| Rack-Supported Mezzanine | Multi-Tier Manual | Up to 200% Floor Multiplier | 300 – 1,000 kg / m² deck | Integrated Structural Upright Columns | E-commerce, Spare Parts Fulfillment |
Advanced Beam-to-Column Interlock Physics & Dynamic Safety Keys
Traditional pallet racking relies on stamped friction tabs prone to micro-fissuring and metal fatigue under cyclic forklift impact. Our facility has implemented precision multi-hook welded connector knuckles cut on robotic fiber lasers. Each hook maintains dynamic mechanical tooth engagement within the 50mm / 75mm pitch column perforations. Equipped with spring-steel automated locking pins with a minimum shear displacement threshold of 10 kN, accidental dislodgement from upward forklift forks is virtually eliminated.
Furthermore, our cold-forming lines utilize multi-pass roll forming tooling (18 to 22 sequential roll stations). This gradual shaping process eliminates residual internal stresses within the cold-worked steel corners, maximizing upright section properties (Ix, Iy) and resisting torsional-flexural buckling under axial compression loads exceeding 25 tons per frame.
The 10-Stage Quality-Controlled Manufacturing Protocol
Spectrometric tensile verification of certified Q235B/Q355B coils.
High-speed precision steel slitting with ±0.1mm tolerance.
Continuous hydraulic multi-punching for pitch uniformity.
22-stage roll passes creating rigid omega upright geometries.
MIG robotic seam welding of 3/4-hook beam connectors.
Deburring, weld spatter cleaning, and uniform edge rounding.
Acid pickling, degreasing, and nanotech anti-corrosion bath.
80-100µm high-adhesion polyester thermoset curing at 200°C.
Deflection verification against AS 4084 / FEM L/200 limits.
ISPM-15 crates or heavy steel stillages for damage-free shipping.
Frequently Asked Questions by Global Racking Buyers
Detailed technical, structural, engineering, and international shipping answers for warehouse managers, civil engineers, and supply chain procurement officers.
What steel grades and structural calculation standards are utilized in your racking systems?
We source premier hot-rolled and cold-rolled certified carbon steel coils primarily conforming to Chinese standards Q235B (yield strength $f_y \ge 235\text{ MPa}$, equivalent to ASTM A36 / S235JR) and high-load Q355B (yield strength $f_y \ge 355\text{ MPa}$, equivalent to ASTM A572 Grade 50 / S355JR). All raw mill heats come accompanied by original Mill Test Certificates (MTC) validating mechanical composition and elongation thresholds.
Our structural design algorithms follow both Australian Standard AS 4084:2023 (Steel Storage Racking), European Standard FEM 10.2.02 / EN 15512, and American RMI MH16.1. We strictly configure our beam profiles to maintain an operational live-load deflection limit of less than $L/200$ (where $L$ is the clear span length between upright columns), guaranteeing structural safety under full working capacity.
How do you support seismic engineering calculations for active seismic regions like New Zealand and the Pacific Rim?
When designing installations for seismic-prone zones—such as New Zealand (NZS 1170.5 compliance) or Western US regions—our in-house engineering team works directly from your site geotechnical data, importance level (IL), and calculated spectral acceleration coefficients ($C_h(T)$).
To accommodate elevated ground acceleration, we engineer heavy-duty footprint anchorages, enlarged reinforced base plates (10mm to 16mm thickness), heavy-gauge horizontal and diagonal cross-bracing struts, and doubled back-to-back row spacers. We deliver comprehensive 3D finite element simulation (FEA) reports and structural data sheets that local structural certifiers and Chartered Professional Engineers (CPEng) require for rapid municipal building consent sign-off.
What are the lead times for custom production and international sea freight delivery?
Standard manufacturing lead time across custom-engineered pallet racking orders typically spans 15 to 25 business days from final 3D CAD drawing sign-off and deposit receipt. Because our production capacity exceeds 30,000 tons per month across automated rolling lines, we comfortably absorb large multi-hundred-ton distribution center rollouts without operational bottlenecks.
Ocean transit from our facility via Guangzhou (Nansha) or Shenzhen (Yantian/Shekou) ports directly to key oceanic hubs takes approximately:
- Sydney, Melbourne, Brisbane: 14 to 21 days
- Auckland, Tauranga: 18 to 26 days
- West Coast USA (LA/Long Beach): 16 to 22 days
- European Main Ports (Rotterdam/Hamburg): 30 to 38 days
How do you handle biosecurity and timber packaging regulations (DAFF / MPI / ISPM-15)?
Border and biosecurity regulations—particularly Australian DAFF and New Zealand Ministry for Primary Industries (MPI)—enforce strict controls on imported organic materials. To prevent expensive port quarantine delays or on-arrival fumigation charges, we utilize two clean export packaging protocols:
1. Heavy-Duty Structural Steel Stillages: Components are bundled inside recyclable fabricated steel frames, entirely eliminating timber and removing 100% of organic quarantine inspection risks.
2. Certified ISPM-15 Heat-Treated Crates: Any necessary wooden skids, dunnage, or pallets undergo accredited kiln heat treatment (56°C for a minimum of 30 continuous minutes) and feature legible, official IPPC circular stamps along with compliant fumigation certificates.
What parameters are required to generate a Free 3D CAD Layout and Load Capacity Quote?
To enable our engineering office to prepare an optimal, code-compliant 3D rendering and comprehensive quotation within 24 hours, please share:
- Warehouse Architectural DWG or Floor Plan: Building dimensions (length, width, clear internal height beneath trusses, sprinklers, or light fixtures).
- Pallet Specifications: Pallet dimension (e.g., standard Australian 1165x1165mm, Euro 1200x800mm, or US 48x40in), load height including pallet, and maximum gross loaded weight.
- Material Handling Equipment (MHE): Forklift make/model, maximum lift mast height, turning radius, and minimum aisle width clearance required (counterbalance, reach truck, or VNA turret truck).
- Environmental Site Conditions: Ambient storage, chilled, or cold-store (-30°C), and facility geographic location for seismic calculations.
What anti-corrosion surface treatments do you offer for humid, outdoor, or sub-zero environments?
We provide three specialized structural coating systems tailored to operational humidity and chemical exposure:
Electrostatic Powder Coating (Standard Interior): Multi-stage chemical degreasing, zinc phosphatizing, and automated electrostatic polyester powder application (70–100 µm film thickness) cured at 200°C for superior scratch, impact, and peeling resistance.
Hot-Dip Galvanizing (HDG) to ISO 1461 / ASTM A123: Complete molten zinc bath immersion (minimum 75–85 µm zinc layer thickness). Ideal for corrosive coastal climates, fertilizer storage, open-air lumber yards, and deep freezer facilities subject to intense condensation.
Pre-Galvanized Coil Components: Roll-formed from high-yield continuous galvanized steel coils (Z275 coating class), providing cost-effective rust inhibition for non-painted components such as pallet supports, upright row bracing, and wire decking brackets.
Accelerate Your Logistics Infrastructure With Direct Factory Supply
Submit your warehouse CAD drawings or operational specifications today. Our senior structural engineers will engineer an optimized 3D layout, verify structural load tables to AS 4084 / CE standards, and provide a transparent factory-direct commercial proposal within 24 hours.