Industrial Pallet Racks On Tracks & Dynamic Flow Systems
Heavy-duty mobile bases guided through precision laser-aligned floor tracks, combined with dynamic gravity roller conveyors to maximize volumetric storage efficiency up to 90% in ambient and sub-zero logistics operations.
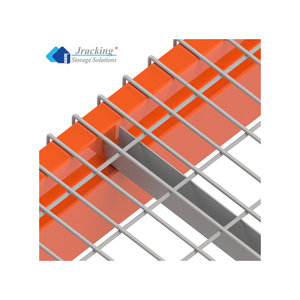
Wire Mesh Waterfall Decking Pallet Rack Selective System
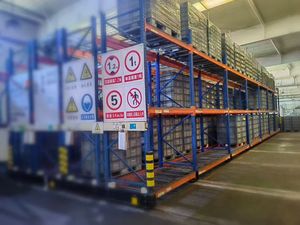
Mobile Pallet Racking System Guided by Fixed Floor Tracks
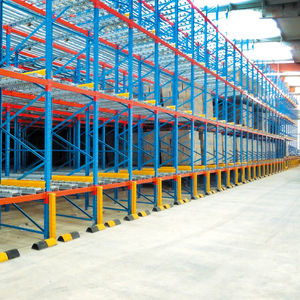
Heavy-Duty Steel Gravity Pallet Racking with Roller Tracks
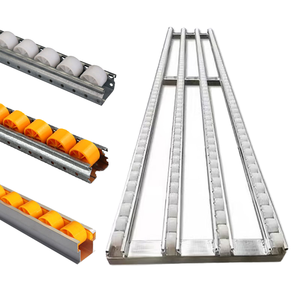
Industrial Roller Track Flow Racks with Aluminium Guide Strips
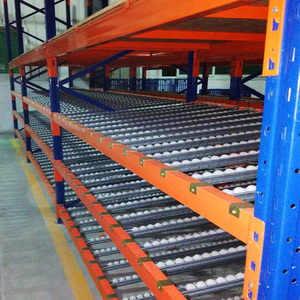
Full-Width Steel Roller Track Pallet Flow Racking Storage
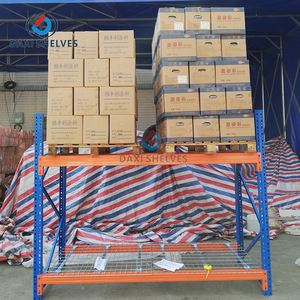
Heavy-Duty Motorized Mobile On-Track Pallet Racking Bogie Base
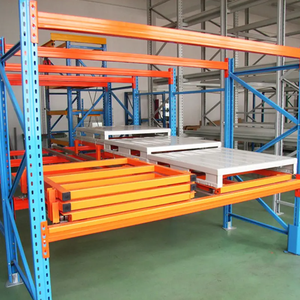
Q235B Steel Telescopic Push Back Racks on Inclined Tracks
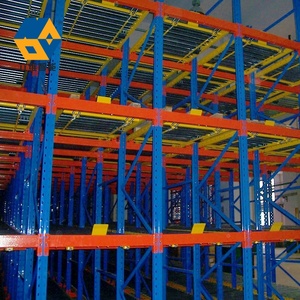
Gravity Flow Pallet Storage Racking with Modular Roller Beds
Structural Kinematics & Floor-Track Mechanics of Mobile Racking
In modern supply chain engineering, conventional selective pallet racking consumes up to 60% of total warehouse floor footprint solely for access aisles. Motorized Pallet Racks on Tracks (also categorized in intralogistics as Powered Mobile Racking or Rail-Guided Dynamic Base Racking) revolutionize spatial economics by placing complete racking superstructures onto electronically synchronized mobile bases (bogies) that traverse across heavy-duty steel tracks embedded flush within the concrete floor slab.
Flush-Floor Embedded Guide Tracks
Fabricated from structural low-carbon manganese alloy steel, the floor tracks feature two distinct geometric profiles: double-flanged guide rails for directional lateral constraint and flat load-distribution rails for pure vertical transfer. Tracks are installed with a level tolerance of < 1.0 mm per 10 meters, secured via chemical anchors and self-leveling, non-shrink structural grout to resist dynamic point loads up to 150 kN per wheel.
Synchronized Geared Drives & Acceleration
Each mobile carriage is driven by multiple decentralized planetary hollow-shaft gearboxes directly coupled to high-wear forged wheels. Controlled by internal Siemens or Omron PLCs with Variable Frequency Drives (VFD), carriages execute programmed S-curve acceleration and deceleration (< 0.08 m/s²), preventing pallet displacement and harmonic resonance across high-rise rack columns.
Multi-Tier Optical Safety Loop
Fully certified to international functional safety standards (ISO 13849-1 PL-d / SIL-2). Racking carriages integrate optical longitudinal laser scanners, mechanical safety contact foot bars, and dual photoelectric safety curtains across aisle entrances. Any micro-movement detection immediately disengages the 400V electromagnetic motor brakes within 12 milliseconds.
Empirical Storage System Performance Matrix
Engineering comparison analyzing a 2,500 m² ambient or cold-storage logistics facility with an 11-meter clear hook height:
| System Architecture | Floor Space Efficiency | Direct Pallet Accessibility | Cold Store Power Reduction | Capital Expense (Capex) | Operational Efficiency (Opex) |
|---|---|---|---|---|---|
| Motorized Pallet Racks on Tracks | 85% - 90% (Maximum) | 100% Selective (Individual Aisle Open) | -42% kWh/pallet | Medium - High (ROI < 2.5 yrs) | Lowest Cost / M³ |
| Standard Selective Pallet Racking | 40% - 48% (Baseline) | 100% Immediate Direct Access | 0% (Standard Heat Dissipation) | Lowest Initial Hardware | High (Excess Building Footprint) |
| Deep-Lane Drive-In Racks | 65% - 72% (High Density) | Poor (Strict LIFO / Honeycombing) | -18% kWh/pallet | Low - Medium | Medium (Forklift Strike Risk) |
| Pallet Flow / Gravity Roller Tracks | 75% - 82% (Dynamic FIFO) | Sequential FIFO Only | -25% kWh/pallet | Medium - High (Brake Rollers) | Very Low (Zero Motor Energy) |
| Automated AS/RS Crane System | 88% - 94% (Vertical) | 100% Automated Pick | -38% kWh/pallet | Extremely High (> 3.5× Mobile) | Low Labor / High Maintenance |
Future Procurement & Technological Trends (2025–2030)
How industrial storage buyers, cold-chain operators, and EPC system integrators are navigating technological convergence, raw material compliance, and total cost of ownership (TCO) shifts.
1. Sub-Zero Cold-Chain Energy Optimization
With industrial cold-storage electricity rates surging globally, refrigerated cubic volume cost is the dominant OPEX driver. Mobile racks on tracks consolidate the thermal envelope, decreasing cooling cubic air volume by up to 45%. Sourcing shifts toward low-temperature structural steels (Q355D with guaranteed Charpy V-notch impact toughness at -20°C and -40°C), synthetic arctic lubricants, and IP67 sealed drive electronics resistant to condensation cycles.
2. AGV & AMR Integration with Mobile Carriages
The traditional limitation of mobile racks—waiting for an aisle to traverse open—is eliminated through Warehouse Control System (WCS) integration. Autonomous Reach Trucks (AGVs) and Autonomous Mobile Robots (AMRs) send pre-arrival RF signals to the rack controller via 5G industrial private networks. The intended access aisle opens automatically while the AGV is in transit, boosting overall pallet cycle times to over 45 dual-cycles per hour.
3. Direct Tier-1 China Mill-to-Site Sourcing
Enterprise procurement teams are bypassing domestic Western resellers to contract directly with large-scale Chinese manufacturing factories like Guangzhou Heda Shelves Co., Ltd. Direct sourcing saves 28% to 40% on steel processing and fabrication margins, while mandating certified Q235B/Q355B mill test certificates (EN 10204 Type 3.1) and engineering calculation models aligned with AS 4084:2023, EN 15512, or ANSI MH16.1.
Furthermore, circularity and life-cycle sustainability are impacting B2B supplier selection. Cold-rolled structural members must feature low embodied carbon profiles, achieved through high-efficiency electric arc furnace (EAF) feedstocks and closed-loop multi-tank pre-treatment lines (zinc phosphating followed by solvent-free electrostatic epoxy-polyester powder coating cured at 200°C). Such finishes provide over 600 hours of salt-spray corrosion resistance (ASTM B117), critical for humid coastal and Pacific Island warehousing environments.
25 Years of Precision Manufacturing: Guangzhou Heda Shelves
Founded in 2001, Guangzhou Heda Shelves Co., Ltd. operates as an integrated industrial racking manufacturer, engineering partner, and global exporter, deploying precision German cold-roll forming lines and certified structural quality control systems.
In-House 10-Stage Precision Heavy Racking Production Sequence
| Step | Manufacturing Stage | Machinery & Technology Deployed | Quality Assurance (QA) Metric |
|---|---|---|---|
| 01 | Raw Material Inbound | Spectrometric chemical analysis & tensile testers | Yield strength verify: Q235B (≥235 MPa), Q355B (≥355 MPa) |
| 02 | Precision CNC Slitting | High-speed hydraulic uncoiler & CNC multi-blade slitter | Width tolerance ±0.1 mm, burr height <0.05 mm |
| 03 | Continuous Column Punching | Automated CNC gantry multi-station punching press | 50mm/75mm hole pitch center tolerance ±0.1 mm |
| 04 | Precision Roll-Forming | 24-station German design cold-roll profiling lines | Section profile angle tolerance ±0.5°, cross-bow <1mm/m |
| 05 | Automated Robotic Welding | Panasonic 6-axis robotic GMAW welding stations | Weld throat thickness check, zero-porosity ultrasonic spot test |
| 06 | Surface Shot-Blasting | Continuous roller-conveyor shot blasting chamber | Surface cleanliness Sa 2.5 profile, complete rust scale removal |
| 07 | Chemical Pre-treatment | Multi-stage immersion: Degrease, pickling, zinc phosphating | Coating adhesion test according to ISO 2409 Cross-Hatch Class 0 |
| 08 | Electrostatic Powder Coat | Gema automated electrostatic spray guns in clean booth | Dry film thickness (DFT) 60-90 μm, uniform cure at 200°C |
| 09 | Assembly Pre-Inspection | Structural mock-up test jig & bogie drive test rail | Motor amp draw, gear alignment, laser sensor trigger checks |
| 10 | Export Packaging & Dunnage | Steel frames, ISPM-15 heat-treated wood & moisture barrier | Zero transport rub damage, DAFF & MPI biosecurity certified |
Engineering & Procurement FAQ for Pallet Racks On Tracks
Detailed technical answers addressing civil floor requirements, seismic compliance, motor synchronization, cold storage operations, and customs clearing.
What concrete floor slab specifications and flatness tolerances are required for track installation?
Tracks can be installed via two engineering methods: (1) Pre-cast floor slab block-outs, where trenches are cast in advance and tracks leveled with high-precision jacks before second-stage non-shrink micro-expansion structural grouting; or (2) Diamond-saw trenching into existing slabs, securing base leveling plates with mechanical/chemical undercut expansion anchors.
How does the system ensure structural compliance with Australian Standards (AS 4084:2023) and New Zealand Seismic Codes (NZS 1170.5)?
For seismic regions in New Zealand and the Pacific Rim, calculations incorporate the site subsoil class, spectral acceleration coefficient $C(T)$, and structural ductility factor $k_p$ according to NZS 1170.5. In high-seismic zones, mobile bases receive heavy-duty mechanical seismic locks (anti-tilt hooks that physically engage the recessed flange of the guide rail), enlarged anchor base plates, and heavy tubular diagonal spine bracing across rack backs.
How do motorized mobile racking systems perform in cold storage environments down to -30°C?
Electrical cabinets incorporate IP65 thermostat-controlled internal ceramic strip heaters to prevent moisture condensation during ambient defrost cycles. In addition, optical sensors utilize heated lens covers to prevent frost build-up, and control wiring utilizes flexible polyurethane (PUR) or silicone insulation that maintains elasticity without cracking below -25°C.
What is the average cycle time to open an aisle, and what happens in the event of a power outage?
In the event of a total facility power outage, several fail-safe protocols exist: (1) An auxiliary generator connection port is standard on the master electrical PLC panel; (2) Manual mechanical brake-release levers allow operators to disengage electromagnetic brakes and move carriages using a manual ratchet crank; (3) Battery-backed UPS maintains sensor logic and emergency lighting states for up to 4 hours.
How are biosecurity inspections, shipping documentation, and timber packing handled for export to Australia, NZ, and Oceania?
All goods are bundled using heavy steel strapping, heavy-gauge steel stillage cradles, or timber dunnage that is 100% compliant with ISPM-15 standards (heat-treated HT and stamped) with accompanying Phytosanitary Certificates. Comprehensive documentation sets include Commercial Invoices, detailed packing lists with piece weight/volume, clean ocean Bills of Lading, and China-Australia Free Trade Agreement (ChAFTA) / NZ-China FTA Certificates of Origin for preferential duty-free entry.
What information is needed to receive a complete 3D layout, weight capacity table, and budgetary quotation?
Plan Your High-Density Mobile Racking System
Submit your site dimensional data to receive a complimentary custom 3D CAD layout, volumetric optimization calculation, and structural engineering load verification.
Spatial Floor Plan
Warehouse length, width, column grid, expansion joints & doors.
Vertical Clearance
Clear height to bottom of lighting, smoke baffles, or sprinkler heads.
Unit Pallet Profile
Dimensions (L × W × H), weight per pallet position & SKU density.
MHE & Climate
Forklift reach height, turning aisle width, and ambient vs cold room temp.
Direct communication with Guangzhou Heda Shelves structural engineering team. Typical 3D CAD turnaround within 24 hours.