Featured Industrial Racking & Dynamic Fulfillment Systems
Direct factory supply from Guangzhou Heda Shelves Co., Ltd. Engineered in compliance with international seismic and load benchmarks including AS 4084, FEM 10.2.07, and CE EN 15095 standards.
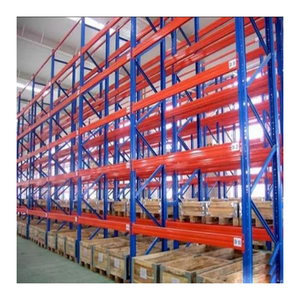
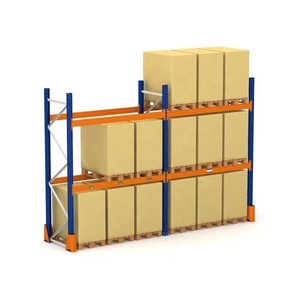
The Mathematics of High-Density Mobile Shelving: Eliminating Static Footprint Waste
In conventional stationary warehouse racking and industrial archive layouts, dedicated access aisles account for 50% to 62% of the gross floor area. Static aisle design mandates that every rack face remain permanently exposed to vehicular or manual picking traffic, generating immense cubic waste in thermal-controlled cold stores, high-rent regional fulfillment hubs, and institutional vaults.
As an authoritative OEM/ODM mobile shelving system supplier and exporter, Guangzhou Heda Shelves Co., Ltd. implements a Single-Aisle Dynamic Kinematic Architecture. By mounting superstructure shelving or heavy-duty selective uprights onto motorized or mechanically geared wheel-carriages traveling along low-deflection ground rails, multiple static access corridors condense into a single floating, demand-activated aisle.
The mathematical volumetric reclamation equation translates to:
Floor Space Conservation (%) = [ (Static Footprint Area - Mobile System Area) / Static Footprint Area ] × 100 ≥ 82.5%
The resulting operational payoff is immediate: facilities can either double their pallet/bin positions within the existing building envelope or halve their architectural footprint, radically slashing concrete slab expenditure, active HVAC loads, cold-storage power draw, and municipal land acquisition costs.
Structural Architecture of Industrial Mobile Shelving Systems
Engineered from prime cold-rolled Q235B and SPCC structural steel, our custom OEM/ODM mobile carriages operate reliably under cyclic load profiles exceeding 24 tons per dual-bay carriage.
1. Carriages & Anti-Torque Wheel Bogies
Fabricated from heavy-gauge structural box beams with robotically welded gussets. Solid C45 carbon steel dual-flanged wheels rest on sealed, self-lubricating spherical roller bearings designed to mitigate lateral crabbing and drive-shaft torsional deflection under asymmetric point loads.
2. Triple-Reduction Mechanical & Smart Electric Drives
Manual-assist units utilize a 1:4.5 mechanical planetary gear chain that allows a warehouse picker to glide 4,000 kg with mere 35N of rotary force. Motorized variants feature soft-start/soft-stop inverter drives (VFD), brushless AC gear motors, and integrated torque-limiter clutches.
3. Multi-Tier Optical & Physical Safety Matrix
Fully compliant with CE Machinery Directive 2006/42/EC and EN 15095. Incorporates floor-level infrared sweeping optical safety curtains, emergency trip stop bars along carriage skirts, aisle occupancy lockout keys, and mechanical seismic anti-tip guide claws engaging sunken steel rail lips.
OEM/ODM Mobile Shelving System Comparison Matrix
Tailoring load capacity, carriage actuation, and surface protection to distinct warehouse environments, from sub-zero blast freezers to cleanroom automotive component staging.
| System Classification | Actuation Mode | Max Carriage Length | Load Rating per Bay | Floor Rail Interface | Primary Sector Application |
|---|---|---|---|---|---|
| Manual Mechanical Compactor | Triple-Reduction Handwheel (1:3 or 1:4.5) | Up to 12.0 meters | 600 kg – 1,200 kg / bay | Surface Ramp or Flush In-Slab | Archives, Medical Records, Specimen Vaults |
| Powered Medium-Duty Mobile Shelf | 0.4 kW Integrated Electric AC Motor / PLC | Up to 24.0 meters | 1,000 kg – 3,000 kg / bay | Recessed Channel Rail, Level Grouted | E-Commerce Picking, Auto Spares, Electronics |
| Heavy-Duty Motorized Pallet Rack | Dual Synchronized 0.75 kW - 1.5 kW Geared Motors | Up to 45.0 meters | 5,000 kg – 24,000 kg / carriage | High-Strength Flat & Guide Inverted Angles | 3PL Cold Storage, Heavy Manufacturing, Chemical |
| Stainless Cleanroom Mobile System | AISI 304 / 316 Sealed Chain or Hand-Push | Up to 8.0 meters | 400 kg – 800 kg / bay | Hermetic Stainless Washdown Tracks | Pharmaceutical Labs, Commercial Kitchens |
| Automated Guided (AGV) Mobile Node | Busbar Power Rail + WMS Bus Interface | Modular Scalable Bays | Per Engineering FEA Specification | Laser-Guided Flush Ground Strip | Dark Fulfillment Centers, Automated Warehousing |
Future Procurement Trends in Industrial Mobile Storage (2025–2035)
As global real estate pressures, net-zero cold chain targets, and labor shortages intensify, enterprise supply chain directors are adopting high-density mobile storage under new strategic parameters.
1. Deep AMR & Autonomous Forklift Synergy
Mobile racking procurement is rapidly migrating away from standalone operational silos. Advanced installations now demand industrial Wi-Fi, OPC-UA, and REST-API modules embedded in the mobile rack PLC control panels. This enables warehouse management systems (WMS) to command carriage separation remotely, so autonomous mobile robots (AMRs) or automated reach trucks drive directly into opened aisles without human dispatch delays.
2. Cold Chain Thermal Densification (Net-Zero Push)
Refrigerated and -30°C blast-freezer power costs are the number one operational expenditure for dairy, meat, and perishable exporters. High-density mobile racking condenses static air cubes by up to 50%, requiring significantly fewer cooling kilowatts per metric ton stored. Procurement tenders now explicitly calculate cold store energy payback (ROI), standardizing on low-temperature synthetic lubricants, silicone wiring harnesses, and heated control enclosures.
3. Decarbonized Steel Sourcing & Modular Demountability
Enterprise ESG mandates are transforming supplier vetting. Global buyers require mill test certificates detailing low-carbon electric arc furnace (EAF) steel sourcing, RoHS-certified lead-free powder coatings, and non-destructive bolted base geometries. Racking systems that can be dismantled, lengthened, or relocated without destroying the structural slab command a major lifecycle value premium over welded static mezzanines.
Guangzhou Heda Shelves Co., Ltd.: Your Trusted OEM/ODM Partner
Founded in 2001, we deliver engineering-led structural storage systems to global racking distributors, EPC warehouse contractors, and Fortune 500 logistics integrators.
30,000m² Dedicated Production Facility
Our heavy-duty industrial facility houses 12 automatic continuous roll-forming lines, robotic welding workcells, automated laser profile cutters, and an in-house 10-stage pre-treatment electrostatic powder-coating conveyor line yielding 30,000 metric tons monthly.
Rigorous Certifications & Traceability
We publish our verifiable certification numbers: CE Certification No. 2435-CPR-8605159 and ISO 9001:2015 Quality Management System No. 18624Q00169R0M. Every production lot includes raw material mill certificates, ultrasonic weld testing, and powder adhesion reports.
Bespoke OEM/ODM Engineering Team
Backed by over 300 technical engineers and project designers, we generate comprehensive 3D CAD models, finite element analysis (FEA) load stress diagrams, and custom-branded upright color schemes tailored to private label distributor portfolios within 24 to 48 hours.
Compliant Export Logistics & Biosecurity
Specialized heavy timber crating adheres strictly to ISPM-15 heat-treatment regulations, expediting customs and quarantine inspection with the Australian Department of Agriculture, Fisheries and Forestry (DAFF) and New Zealand MPI. Complete ChAFTA documentation supplied.
End-to-End Quality Verification Process
From hot-rolled steel strip receipt through automated cold bending, every mobile shelving carriage and upright profile passes rigorous non-destructive inspection gates.
Steel Coil Testing
Yield strength verification of Q235B/SPCC coil stock, chemical composition analysis, and thickness caliper testing against ±0.05mm tolerance limits.
Precision Roll-Forming
Multi-station cold roll-forming lines shape upright posts and carriage channel beams without micro-fracturing structural bend radii.
10-Stage Pre-Treatment
Hot degreasing, multi-stage acid pickling, zinc phosphating, and deionized water rinse cycles to ensure absolute rust immunity and powder bonding.
Electrostatic Curing
Robotic electrostatic powder application followed by a 200°C baking tunnel creates an ultra-durable, scratch-resistant 60–80μm polymer barrier.
Frequently Asked Technical & Procurement Questions
Clear, engineering-driven answers to the most common questions raised by warehouse developers, procurement officers, and structural engineers.
What slab flatness tolerances and load-bearing capacities are required for heavy mobile racking? +
How does HEDA ensure seismic engineering compliance in earthquake-prone regions such as New Zealand and Japan? +
Can mobile racking systems operate safely inside sub-zero blast freezers and cold storage environments? +
What failsafe personnel safety systems protect operators inside an open mobile racking aisle? +
What are the lead times for custom OEM/ODM roll-forming, containerization, and sea transit? +
How do you handle biosecurity and timber packaging compliance for Australian and New Zealand imports? +
Request a Custom 3D CAD Layout & Factory-Direct Quote
Whether you require a custom branded OEM run of manual mechanical compactor shelving or an industrial-grade motorized pallet racking deployment for cold storage, our senior engineering team will calculate your floor loading, layout dimensions, and ROI breakdown within 24 hours.