Top 10 Rack Storage Shelves Manufacturer & Factory
An engineering whitepaper and buyer benchmark evaluating direct industrial manufacturers, cold-roll steel standards, AS 4084 / FEM compliance, and intelligent warehouse automation infrastructure.
Factory-Direct Heavy-Duty Systems
Industrial Racking & Precision Shelving Catalog
Engineered for global distribution centers, third-party logistics (3PL), automotive facilities, and refrigerated cold stores. All systems are fabricated from certified structural cold-rolled steel coils, fully compliant with international load limit states.
Top 10 Rack Storage Shelves Manufacturer & Factory Evaluation Matrix
When supply chain directors and enterprise warehouse procurement executives analyze the global competitive landscape—evaluating international entities such as SSI Schaefer, Mecalux, Dexion, Stow Group, Daifuku, Interlake, Nedcon, Jungheinrich, BITO, and HEDA Shelves—the decision rests on technical compliance, steel yield reliability, dynamic seismic verification, and total landed cost.
2001Est.
Founding Year
30,000m²
Direct Factory Footprint
30,000T/Mo
Steel Processing Output
10,000+
Worldwide Projects Executed
Evaluation Parameter
HEDA Shelves Direct Factory
European Integrated Brands
North American Tier-1 OEMs
Generic Commodity Workshops
Primary Design Codes
✔ AS 4084:2023, EN 15512, NZS 1170.5
EN 15512, FEM 10.2.02, DIN standards
RMI (ANSI MH16.1), AISI S100
Inconsistent non-certified internal tables
Steel Certification & Metallurgy
Certified Baosteel/Shougang Q235B / Q355B with MTR
Low initial price; extreme risk of on-site failure
Direct-Factory Advantage
Eliminating third-party brokers allows procurement managers to obtain precise mill test certificates, certified chemical batch numbers, and direct-line production scheduling. Sourcing from our 30,000 m² Guangzhou production facility provides direct control over profile geometry, cold-roll thickness tolerances, and immediate revision capabilities for bespoke warehouse layouts.
Strict Regulatory Compliance
Unlike workshops operating without structural traceability, HEDA Shelves holds valid CE Certification No. 2435-CPR-8605159 and ISO 9001:2015 Certification No. 18624Q00169R0M. Design engineers utilize AS 4084 limit state principles and EN 15512 standards to calculate maximum permissible beam deflection within the L/200 structural ceiling.
Interoperable Modern Automation
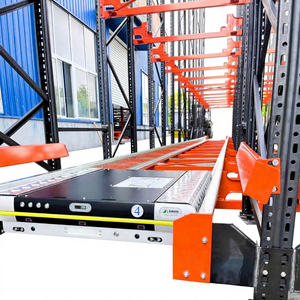
Modern distribution demands seamless integration between structural racking and automated machinery. Our high-density radio shuttle tracks, VNA inductive guide rails, and gravity flow dynamic lanes maintain sub-millimeter tolerances across 50-meter uninterrupted runs, preventing AGV and carrier jamming during high-throughput operational peaks.
Metallurgical Rigor & Mechanics
Structural Integrity: From Raw Coil to Certified Deflection Thresholds
The failure of an industrial rack system in an operational warehouse carries catastrophic financial and safety consequences. High-capacity performance starts at the atomic level: selecting premium hot-rolled carbon steel coils (Q235B and Q355B) that demonstrate optimal elongation percentages (≥26%) to absorb dynamic forklift docking impacts without brittle fracturing.
Continuous Multi-Station Roll Forming: Cold-roll forming lines utilize up to 24 consecutive roller passes, incrementally shaping upright profiles to prevent internal micro-stress cracks and preserve cold-work yield hardening.
Complex Omega Column Geometries: 8-to-10 bend engineered upright geometries distribute axial compression evenly, maximizing the radius of gyration ($r$) and preventing torsional buckling under heavy vertical loads.
Dual-Locking Safety Connector Pins: Beam-to-column connections rely on precision-stamped 3-prong or 4-prong claw connectors featuring spring-steel safety locking pins with an anti-dislodgement resistance exceeding 5 kN per connection.
7-Stage Anti-Corrosion Finishing: Components undergo automatic ultrasonic alkaline degreasing, acid pickling, zinc-phosphating, and an electrostatic epoxy-polyester thermosetting powder coat baked at 200°C for superior chemical resistance.
Maximum Allowable DeflectionDeflection ≤ L / 200 (Elastic Limit)
Safety Factor Factorization1.5 to 1.65 Structural Limit State
Powder Coating Thickness60 – 85 Microns (ISO 2178 Validated)
Seismic Ground Accel. ($a_g$)Up to 0.45g Dynamic Wave Spectral
Baseplate AnchoringM12 / M16 Heavy Anchor Expansion Studs
Industry 4.0 & Strategic Sourcing
Future Procurement Trends in Industrial Storage Infrastructure
Strategic buyers must forecast structural requirements beyond immediate storage needs. The next decade of warehouse design is defined by high cube utilization, algorithmic intralogistics, and strict ESG compliance across international borders.
01
High-Density Shuttle & AMR Integration
Rising industrial land values are rendering standard wide-aisle (3.5m) selective layouts obsolete. Procurement is pivoting toward semi-automated radio shuttle racking and Autonomous Mobile Robot (AMR) compatible structural platforms that reduce aisle space by up to 60% and elevate cubic capacity utilization above 85%.
02
Dynamic Seismic Micro-Zoning
Following stringent regulatory updates in Pacific Rim territories, New Zealand (NZS 1170.5), Australia (AS 4084:2023), and the western Americas, generic load charts are no longer approved by municipal certifiers. Future procurement mandates finite element analysis (FEA) and site-specific response spectrum calculations before fabrication.
03
Scope 3 Decarbonization & EPDs
Global ESG reporting requires multinational 3PLs to audit embodied carbon within warehouse steel racking. Progressive factories now utilize electric-arc furnace (EAF) steel coils, low-VOC TGIC-free powder coatings, and zero-discharge closed-loop chemical pre-treatment systems with verified Environmental Product Declarations (EPD).
04
Direct-to-Factory Engineering Sourcing
Mid-tier equipment distributors often add 30-50% markups without contributing structural engineering value. Modern procurement teams contract directly with scaled manufacturers like HEDA Shelves to receive customized 3D CAD modeling, factory witness testing, and custom export packing tailored to local customs biosecurity clearances.
Precision Manufacturing
Inside HEDA Shelves: 10-Stage Production Architecture
Operating out of our advanced 30,000 m² facility with a dedicated engineering team of over 300 professionals, HEDA Shelves maintains strict internal quality control across every phase of steel processing.
1. Coil QC & Laser Blanking
Incoming hot/cold rolled coils undergo ultrasonic thickness inspection and yield tensile validation. CNC high-speed slitting lines cut coils to width tolerances of ±0.1mm to ensure uniform roll-formed profiles.
2. Automated CNC Punching
Heavy mechanical continuous punching presses apply 50mm or 75mm pitch diamond/teardrop hole configurations along the upright column axis, maintaining ±0.2mm cumulative tolerance over 12-meter lengths.
3. Cold Profile Roll-Forming
Upright columns and interlocking box beams pass through dedicated automated rolling lines, ensuring crisp profile angles, straightness tolerances within 1/1000, and zero residual profile twist.
4. Robotic Dual-Torch Welding
Beam end connectors and heavy base plates are fused to structural sections utilizing automated Panasonic MIG/MAG dual-torch robotic welding cells, guaranteeing deep weld penetration and zero slag defects.
5. Full Pre-Treatment & Coating
Automated immersion overhead tracks cycle structural components through alkaline degreasing, pickling, water rinsing, and silane/phosphate nanocoating before electrostatic powder curing.
6. Biosecure Export Packing
Racking components are strapped into rigid steel stillages or ISPM-15 heat-treated cradles, fully compliant with Australian Department of Agriculture (DAFF) and NZ MPI biosecurity requirements.
Procurement Knowledge Base
Frequently Asked Questions by Industrial Warehouse Buyers
Direct engineering and commercial answers to resolve standard regulatory, structural, logistical, and installation inquiries during warehouse project planning.
How does HEDA Shelves ensure compliance with AS 4084:2023 and European EN 15512 standards?
Our structural engineering team produces comprehensive engineering calculation dossiers with reference to AS 4084:2023 (Steel Storage Racking) and EN 15512 (Cold-formed Steel Storage Racks). We supply certified cross-sectional properties, moment-rotation curves of the beam-to-column connector assemblies, shear capacities, and baseplate anchorage calculations. This documentation allows your registered local Professional Engineer (CPEng / NER in Australia/NZ or PE in North America) to review and stamp building consent and rack safety documentation quickly.
What is the standard production and shipping lead time to major global ocean ports?
Standard factory production lead time for orders between 2 and 15 High-Cube 40ft containers (40HQ) is typically 15 to 22 business days from final 3D CAD approval. Ocean freight transit times from our South China shipping hubs (Nansha / Shekou / Yantian) average:
Australia/NZ: 12 to 21 days (Sydney, Melbourne, Brisbane, Auckland);
Western Europe: 26 to 34 days (Rotterdam, Hamburg, Felixstowe);
North America: 14 to 20 days (Long Beach, Oakland, Vancouver) and 28 to 35 days (Savannah, Houston, Newark).
Can your pallet racking systems be configured for extreme seismic hazard zones?
Yes. For seismic environments—such as New Zealand (NZS 1170.5 criteria), the US West Coast (ASCE 7 / IBC), or earthquake-prone Pacific regions—we calculate dynamic response spectrum accelerations ($S_a$). We engineer systems with enlarged heavy-gauge structural baseplates, dual floor anchor bolts per post, thick-gauge spine horizontal and diagonal portal bracing, reinforced upright cross-sections, and heavy-duty top-tie structural overhead bridges.
How do you handle biosecurity and timber packaging compliance for Australian and New Zealand ports?
We adhere strictly to Australian DAFF (Department of Agriculture, Fisheries and Forestry) and New Zealand MPI (Ministry for Primary Industries) biosecurity import mandates. Racking is packed using solid welded steel transport cradles or fully certified ISPM-15 compliant heat-treated timber dunage bearing official HT stamp certifications. Complete container packing declarations, fumigation documentation (if requested), commercial invoices, and ChAFTA/NZ-China FTA Certificates of Origin (Form COO) accompany every shipment to expedite border clearance.
What technical information is required to generate a customized 3D CAD layout and quotation?
To deliver an engineering drawing within 24 hours, our layout team requires:
1. Warehouse Architectural Plan: Dimensions (Length × Width), interior column grid locations, roller doors, egress paths, and ceiling clear height under obstructions (lighting/sprinklers);
2. Pallet Specifications: Pallet dimension (W × D × H including cargo overhang) and gross weight per unit load;
3. Material Handling Equipment (MHE): Forklift make/model, mast collapsed and extended heights, turning radius, and minimum right-angle stacking aisle width ($A_{st}$);
4. Operating Temperature: Ambient, air-conditioned, chiller, or deep freeze (-25°C).
What surface finishes are recommended for outdoor or corrosive environments?
For standard indoor ambient warehousing, our 60–80 micron electrostatic epoxy-polyester thermosetting powder coat provides excellent impact resistance and anti-scratch durability. For cold stores with condensation, humid coastal islands, chemical manufacturing warehouses, or outdoor cantilever pipe storage, we supply Hot-Dip Galvanizing (HDG) compliant with ISO 1461 / ASTM A123, ensuring zinc coating thickness between 70 and 100 microns for decades of rust-free service life.
Do you support OEM and private-label manufacturing for regional racking distributors?
Yes. A significant portion of our 30,000-ton monthly output supports regional racking brands, commercial builders, and logistics integrators. We support custom punch tool tooling (50mm, 75mm, 76.2mm pitch), custom beam profile roll-forming, private-label safe working load rating plates, brand-specific RAL powder coating matching, and neutral or distributor-branded export packaging.
What on-site installation support and assembly documentation is provided?
Every shipment includes an installation manual, step-by-step 3D assembly exploded views, bolt torque specification tables, and numbered architectural placement schematics matching bundle shipping tags. For large-scale projects, we provide remote video installation assistance or deploy senior factory site supervisors to lead local rigging crews, verify leveling shims, and oversee anchor tensioning.
Engineering Consultation
Accelerate Your Warehouse Capacity with Direct-Factory Engineering
Submit your warehouse CAD floor plan, clear height dimensions, pallet specifications, and forklift parameters. Our engineering department will return an optimized 3D layout, pallet capacity analysis, and landed price quotation within 24 business hours.